Choosing the best Aluminum Perfume Bottle manufacturer for 2026 requires more than comparing polished samples and low quotations. It requires evidence. A reliable supplier should demonstrate material traceability, stable wall thickness, accurate neck dimensions, coating resistance, and repeatable color matching. These details matter when a bottle meets a crimp pump, travels through humid warehouses, or sits under retail lighting for months.
Market signals support this careful approach. Grand View Research’s fragrance market analysis identifies premium packaging, brand differentiation, and sustainable materials as important growth influences. Smithers’ packaging sustainability reports also emphasize lightweighting, recyclability, lifecycle measurement, and supply-chain transparency. Aluminum can support these goals, but only when manufacturers control energy use, surface treatment, and scrap recovery. The material alone is not proof of sustainability.
That distinction matters.
This 2026 guide examines manufacturers through practical experience and measurable capability. It considers aluminum forming methods, anodizing and lacquering quality, mold development, decoration precision, leak testing, and compatibility with fragrance components. It also reviews certifications, audit records, export experience, minimum order quantities, and after-sales support. PMMI packaging reports repeatedly highlight automation, quality control, and resilient supply chains as purchasing priorities. Those priorities deserve attention here.
However, no ranking is universally correct. Supplier websites may present incomplete factory data, and sample quality may not represent mass production. Buyers should request recent inspection records, production videos, test reports, and reference projects. A beautiful prototype can still hide inconsistent threads or weak coating adhesion. In this context, Perfume Bottle Aluminum is not merely a search term; it represents a packaging decision requiring technical judgment, commercial caution, and honest verification.
Aluminum Perfume Bottle Manufacturing: An Overview for 2026
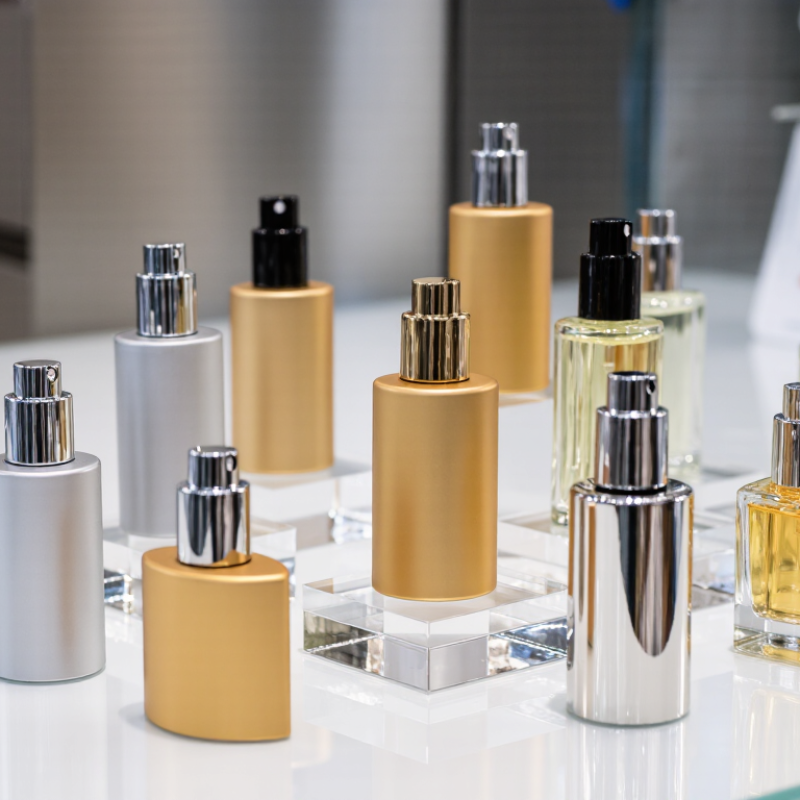
In 2026, aluminum perfume bottle manufacturing combines lightweight design with stricter quality control. It starts with metal. Manufacturers usually form bottles through deep drawing, extrusion, or precision stamping. Each method affects wall thickness, shape, production speed, and tooling cost. Experienced teams check the alloy before forming, because inconsistent material can create wrinkles, cracks, or uneven surfaces. Small errors matter. A bottle may look attractive yet fail during filling or transport.
Surface treatment requires careful control. Polishing, anodizing, painting, and protective coating can create different textures and color effects. Internal lacquer is equally important, since fragrance ingredients may react with bare aluminum. Reliable factories test chemical compatibility, coating adhesion, neck dimensions, and closure torque. They also perform leak tests, drop tests, and repeated opening checks. These details provide practical evidence of manufacturing capability, not just attractive samples.
When evaluating a manufacturer, request material certificates, inspection records, production samples, and clear tolerance data. Ask how defects are classified and how batches remain traceable. Sustainable production should include efficient material use, recyclable packaging, and responsible waste handling. However, recycled content can require tighter process controls. No process is flawless. A polished prototype can hide problems that appear during mass production. Pilot runs, independent inspections, and documented corrective actions reduce that risk. My view is cautious: the best supplier is not always the cheapest or most impressive, but the one that reports limitations honestly and improves them consistently.
Aluminum Perfume Bottle Manufacturing: An Overview for 2026
Common commercial perfume bottle formats include 30 ml, 50 ml, 100 ml, and 150 ml. These fill volumes are widely used in fragrance packaging and can be produced with aluminum bodies, internal coatings, decorative finishes, and compatible closures. When evaluating manufacturers, buyers should also review coating compatibility, dimensional consistency, decoration quality, minimum order quantities, and production lead times.
Designing an aluminum perfume bottle starts with the product experience, not the decoration. Engineers study the fragrance formula, fill volume, closure system, and expected handling conditions. Aluminum offers light weight and strong impact resistance. However, it can react with certain contents without a suitable internal coating. That detail is easy to overlook.
Manufacturers usually form the bottle through impact extrusion or deep drawing. The metal sheet or slug is shaped under controlled pressure, then trimmed and annealed when needed. Each step affects wall thickness, weight, and neck accuracy. The inside is cleaned carefully before applying a compatible protective lacquer. Coatings need uniform coverage, especially around the shoulder and base. Small gaps can create long-term quality problems.
The outer surface may receive polishing, anodizing, painting, or printed decoration. Experienced production teams inspect color, gloss, scratches, and logo alignment under consistent lighting. They also test thread fit, crimp dimensions, leakage, drop resistance, and coating adhesion. Samples should be checked with the actual pump and fragrance, not with water alone. That is a common shortcut.
A reliable manufacturer documents material batches, process settings, and inspection results. Independent testing can verify chemical compatibility and packaging performance. Still, no process is flawless. A visually perfect bottle may fail after repeated temperature changes. Buyers should request pilot samples, aging tests, and clear tolerance data before approving large production. Small design adjustments often prevent expensive rework.
| Evaluation Dimension | Typical Industry Specification | How It Is Designed or Produced | Why It Matters for Perfume Packaging | Recommended Supplier Check |
|---|---|---|---|---|
| Bottle Material | Common aluminum grades include 1050, 3003, and 5052, selected according to forming, strength, and surface requirements. | Aluminum sheet or slug is cut, stamped, impact-extruded, or deep-drawn into the required bottle body. | Aluminum is lightweight, opaque, recyclable, and provides protection from light exposure that can affect fragrance appearance and stability. | Request the exact alloy designation, temper, material certificate, and recycled-content statement where applicable. |
| Typical Capacity Range | Approximately 10–200 mL for travel, sample, personal-use, and premium fragrance formats. | The designer defines the internal volume, external dimensions, shoulder profile, base geometry, and center of gravity before tooling. | Capacity influences product positioning, shipping cost, portability, and compatibility with pumps and closures. | Confirm nominal fill volume, brimful capacity, tolerance, and the required fill line with the packaging supplier. |
| Wall and Base Design | Wall thickness is design-dependent; many formed aluminum packages use thin, lightweight walls with a reinforced base and neck area. | Finite-element analysis, forming trials, and dimensional inspection are used to balance rigidity, weight, and manufacturability. | The structure must resist denting, deformation, leakage, and damage during filling, transport, and consumer handling. | Ask for wall-thickness maps, compression results, drop-test conditions, and allowable cosmetic dents. |
| Internal Protection | A compatible internal coating or lacquer may be used when the fragrance formula requires additional chemical resistance. | The formed body is cleaned, treated, coated, and cured under controlled time and temperature conditions. | The internal barrier helps reduce direct contact between the fragrance formula and the aluminum surface. | Require formula-compatibility testing, coating specification, cure records, and extractables or migration evaluation when relevant. |
| Neck and Closure Compatibility | Crimp, screw, or custom neck systems may be used; the finish must match the selected pump, valve, collar, and cap. | The neck is formed or machined to controlled diameter, height, roundness, and sealing dimensions. | A precise neck finish supports reliable crimping, spray performance, leak prevention, and consistent assembly. | Verify neck drawings, pump compatibility, crimp dimensions, torque requirements, and assembled leak-test results. |
| Surface Finishing | Available finishes commonly include anodizing, spray coating, metallic coating, satin brushing, polishing, and protective clear coating. | Surface preparation is followed by coloring or coating, curing, and visual inspection under defined lighting conditions. | The finish creates the visual identity while improving scratch resistance and perceived product quality. | Approve a master color standard and check gloss, adhesion, abrasion resistance, color deviation, and coating uniformity. |
| Decoration Options | Screen printing, pad printing, hot stamping, offset printing, laser marking, embossing, and debossing are widely used. | Decoration is applied after forming and surface treatment, with registration controls for curved or tapered bodies. | Aluminum supports both minimalist unprinted designs and high-contrast premium graphics. | Evaluate artwork accuracy, ink or foil adhesion, barcode readability, abrasion resistance, and batch-to-batch color consistency. |
| Leak and Pressure Testing | Testing methods may include vacuum, pressure, inverted-storage, thermal-cycle, and assembled-package leakage tests. | Samples are tested after filling or with a validated test medium; results are compared with approved acceptance criteria. | Fragrance leakage can damage labels, cartons, dispensing components, and surrounding products. | Request written test methods, sample quantities, acceptance limits, and reports from production-equivalent samples. |
| Dimensional Quality Control | Critical checks include height, diameter, neck finish, wall thickness, roundness, weight, volume, and decoration position. | Calipers, gauges, coordinate-measuring equipment, weighing systems, and visual standards are used during inspection. | Tight dimensional control improves pump fit, assembly efficiency, shelf appearance, and filling-line performance. | Confirm inspection frequency, sampling plan, calibrated equipment, control plans, and certificate-of-analysis availability. |
| Sustainability Profile | Aluminum is widely recyclable, and recycled content can reduce the material’s primary-production energy demand; actual benefits depend on sourcing and processing. | Manufacturers can reduce impact through lightweighting, scrap recovery, recycled feedstock, efficient coating systems, and optimized transport packaging. | Sustainability claims must reflect the complete package, including coatings, pumps, caps, labels, and material separation. | Ask for recycled-content evidence, environmental declarations where available, scrap-recycling data, and clear disposal guidance. |
| Compliance Documentation | Relevant documentation may include material declarations, restricted-substance statements, quality certificates, packaging specifications, and traceability records. | Compliance is managed through documented specifications, approved raw materials, batch records, inspections, and corrective-action procedures. | Document control supports market access, retailer requirements, product safety reviews, and consistent future production. | Check alignment with applicable requirements such as REACH, packaging regulations, ISO-based quality systems, and destination-market rules. |
Evaluating aluminum perfume bottle manufacturers in 2026 requires more than attractive samples. Examine alloy quality, wall thickness, coating durability, and neck precision. A reliable manufacturer should provide material certificates, batch records, and clear testing procedures. Ask how they control color differences between production runs. Small variations can become expensive on retail shelves.
From practical sourcing experience, factory evidence matters more than polished presentations. Request a live production video or an on-site audit. Check stamping accuracy, thread fit, inner lining, and resistance to fragrance oils. The manufacturer should explain its quality limits honestly. If every answer sounds perfect, investigate further. Real production has occasional defects, and transparent corrective actions build stronger trust. Review worker safety, waste handling, and compliance with applicable packaging regulations before signing an agreement.
Tips: Order pilot samples before large production. Test filled bottles under heat, cold, vibration, and repeated handling. Measure leakage after storage, not only immediately after filling. Confirm minimum order quantities, tooling ownership, lead times, and inspection responsibility in writing. Keep one approved sample as a reference. It prevents disputes later. A useful supplier also responds clearly when specifications change, although this communication is sometimes overlooked.
Choosing an aluminum perfume bottle manufacturer requires more than comparing unit prices. A capable supplier should control alloy grade, wall thickness, neck dimensions, coating quality, and closure compatibility. Request production samples, not only catalog images. Fill them with the intended formula and test leakage, odor transfer, scratches, and crimp stability. Small details matter.
The International Aluminium Institute reports that recycling aluminum can use about 95% less energy than producing primary aluminum. This makes recycled content an important supplier question. Ask for recycled-content documentation, batch traceability, and evidence of responsible material sourcing.
Grand View Research valued the global fragrance market at approximately USD 50.85 billion in 2023, with continued growth projected through 2030. Rising demand increases pressure on manufacturers to deliver consistent quality at scale.
Look beyond impressive samples. A supplier may offer beautiful decoration but weak internal protection. Request coating specifications, migration test results, salt-spray data, and documented quality procedures. Confirm minimum order quantities, mold ownership, lead times, and replacement policies before signing. A factory audit can reveal practical issues, such as dusty assembly areas or inconsistent inspection records. Not every report is perfect. That is precisely why independent testing remains useful. The best manufacturers combine engineering discipline, transparent communication, and repeatable production. They should also explain what happens when a batch fails, rather than hiding behind polished presentations.
Choosing an aluminum perfume bottle manufacturer requires more than comparing catalog photos and quoted prices. A reliable partner should explain alloy grades, coating methods, closure tolerances, and production limits clearly. Ask for recent samples, not only polished prototypes. Examine the bottle under bright light. Look for uneven anodizing, sharp edges, loose caps, or scratches around the neck.
Request material certificates and documented quality procedures before approving production. The manufacturer should provide dimensional reports, leak-testing records, and packaging details. Small defects often appear after filling, transport, or repeated opening. Ask how rejected units are recorded and corrected. A factory that hides problems creates larger costs later. Clear communication matters too. Confirm minimum order quantities, tooling ownership, sampling fees, lead times, and inspection points in writing.
Sustainability claims need evidence. Check recycled aluminum content, coating chemistry, energy data, and waste-handling practices. Local testing may also be needed for packaging safety and market requirements. Do not accept vague promises. During supplier evaluation, speak with the technical team, not only a sales contact. Their answers reveal practical knowledge. I once considered appearance too heavily in a packaging decision. The finish looked excellent, but the cap fit changed after temperature testing. That mistake was avoidable. A capable manufacturer welcomes difficult questions, reports limitations honestly, and supports controlled improvements when the first design is not perfect.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru