2026 Best Types of Weld Fittings for Global Buyers?
Choosing the best weld fittings in 2026 requires more than comparing prices or catalog photographs. Global buyers must connect fitting performance with pressure ratings, material grades, welding methods, and service conditions. A fitting used on a clean-water line may not suit a high-temperature chemical process. Small details matter.
This guide examines common types, including butt-weld elbows, tees, reducers, caps, and socket-weld connections. It considers stainless steel, carbon steel, alloy steel, and other widely specified materials. Experienced procurement teams usually check dimensions, wall thickness, heat numbers, mill certificates, and inspection records before approval. They also confirm compatibility with ASME, ASTM, EN, ISO, or project-specific requirements. Standards alone do not guarantee quality.
Supplier reliability matters just as much. Clear drawings, traceable documentation, consistent packaging, and responsive technical support can prevent costly installation delays. A properly protected fitting should arrive with clean bevels, visible markings, and no damaging dents. That sounds basic. It is often overlooked.
The “best” choice depends on the pipeline’s actual duty, not the supplier’s strongest marketing claim. This article compares weld fittings through practical buyer concerns, such as corrosion exposure, fabrication efficiency, delivery risk, and lifecycle value. Some recommendations may remain imperfect because projects differ, and no universal ranking can cover every plant or region. Buyers should verify critical details with qualified engineers and approved inspection procedures before placing an order. That caution is worthwhile.
What Are Weld Fittings and How Are They Classified?
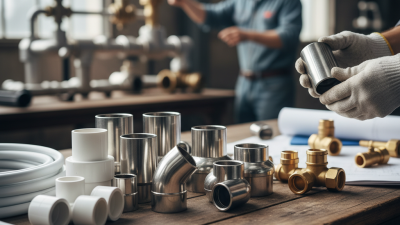
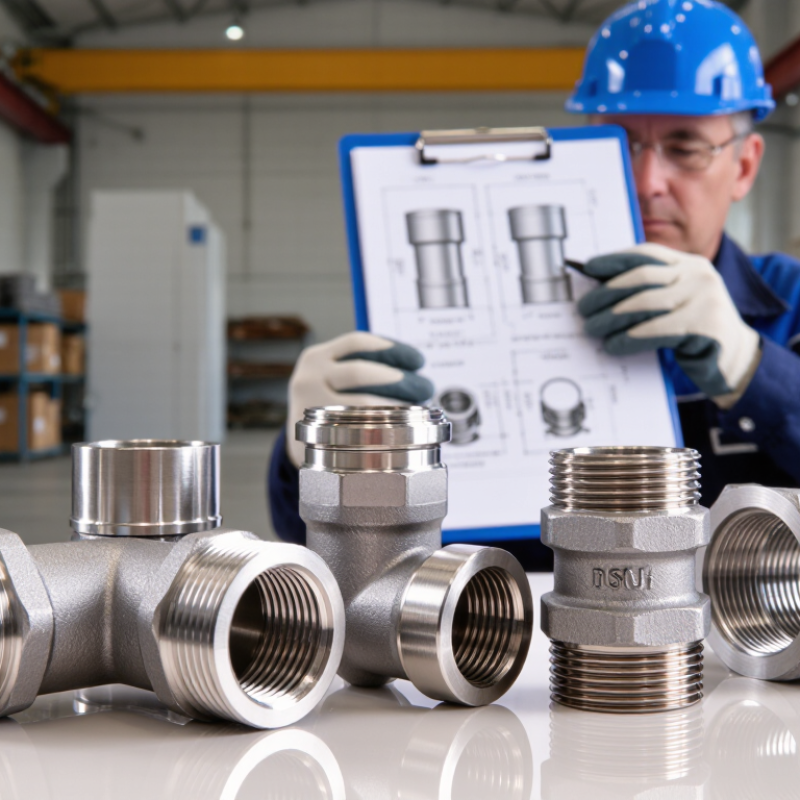
In 2026, weld fittings remain essential for building reliable industrial piping systems. They connect pipes permanently and manage direction, size, or flow changes. Typical examples include elbows, tees, reducers, caps, and stub ends. Their classification begins with the connection method: butt-weld fittings have beveled ends, while socket-weld fittings fit inside a recessed socket.
Butt-weld fittings are commonly selected for larger pipe sizes, high temperatures, and demanding pressure service. Socket-weld fittings suit smaller bore systems and offer practical alignment during installation. The choice depends on pipe diameter, wall thickness, access, and operating conditions. Small details matter.
Fittings are also classified by shape, material, pressure rating, and dimensional standard. A long-radius elbow usually reduces turbulence more effectively than a short-radius design. Concentric reducers keep the centerline aligned, while eccentric reducers can support drainage or prevent air pockets. Carbon steel, stainless steel, duplex steel, and nickel alloys serve different temperature and corrosion environments. Material certificates, heat numbers, and dimensional checks support traceability. However, classification is not always clean. One fitting may belong to several groups at once, and selecting by shape alone can be a costly mistake. Engineers should verify NPS or DN size, schedule, weld preparation, service fluid, and applicable standards before approval. A perfect drawing still cannot replace a careful fit-up inspection.
Which Weld Fitting Types Suit Different Piping Applications?
Selecting weld fittings by application prevents leaks, stress concentration, and expensive rework. The choice is rarely only about diameter.
For process and utility pipelines, butt-weld elbows, tees, reducers, and caps provide smooth flow and strong alignment. Long-radius elbows usually reduce turbulence and pressure loss. Short-radius elbows save space, but they can increase local stress. ASME B16.9 defines key dimensions for these factory-made fittings. ASTM A234 covers many carbon and alloy steel grades used in elevated-temperature service. Check both standards carefully.
High-pressure instrument lines often need socket-weld fittings under ASME B16.11. Their compact design suits small-bore connections, although poor cleaning can leave crevices. Sanitary piping may use butt-weld fittings with polished internal surfaces. Food, pharmaceutical, and clean-water systems demand careful control of surface roughness and dead legs. Thin-wall tubing is different. Excessive welding heat can distort the bore, so qualified procedures matter.
Material selection should follow temperature, corrosion, and fluid chemistry. ASTM A403 supports common stainless-steel wrought fittings, while ASTM A815 covers duplex and other alloy systems. The World Steel Association reported approximately 1.89 billion tonnes of crude steel production in 2023, showing the scale of global material supply. Availability does not guarantee suitability. A lower-cost carbon-steel reducer may fail quickly in chloride service. Field inspection also reveals a practical weakness: drawings often specify fitting size but omit corrosion allowance, weld inspection, or surface requirements. That omission deserves correction before purchasing.
How Do Materials and Manufacturing Standards Affect Fitting Choice?
2026 Best Types of Weld Fittings for Global Buyers?
Material selection often determines whether a weld fitting survives years of pressure, heat, and corrosion. Carbon steel suits many general pipelines, while stainless steel performs better in humid or chemically aggressive service. Duplex grades may offer stronger corrosion resistance, but they require tighter welding control. Nickel alloys handle severe environments, although their cost can change a project budget quickly.
Manufacturing standards affect more than paperwork. Dimensions, wall thickness, bevel geometry, and pressure ratings should match the piping system. ASME B16.9, EN 10253, and applicable ASTM material specifications are common references, but they are not automatically interchangeable. Buyers should confirm the project standard, design pressure, temperature range, and local inspection requirements before ordering.
Traceability is practical, not decorative. A reliable supplier should provide heat numbers, material test certificates, dimensional reports, and clear marking. I have seen fittings pass a visual check but fail when wall thickness varied near the weld end. That detail matters. Request independent inspection when the service is critical. Still, no checklist catches every mistake. A cheaper fitting may reduce the invoice while increasing installation delays. One overlooked mismatch can affect an entire line. Experienced buyers compare documents, samples, welding procedures, and service conditions together, rather than choosing by material name alone.
How Can Global Buyers Compare Quality, Compliance, and Total Cost?
Global buyers should compare weld fittings through evidence, not catalog photos.
Butt-weld fittings suit continuous process lines, while socket-weld fittings fit smaller, high-pressure connections. Threaded fittings can simplify installation, yet they may introduce leakage risks in vibration-heavy service. Material selection must match pressure, temperature, corrosion exposure, and welding procedure. Ask for heat numbers, chemical analysis, mechanical results, and dimensional inspection records.
Quality is measurable at receiving inspection.
Check wall thickness at several points, bevel angle, ovality, surface marks, and weldability. For stainless or alloy fittings, positive material identification can prevent an expensive mix-up. Request independent testing when the application is critical or supplier records seem incomplete. Standards such as ASME B16.9 or B16.11 may apply, but the project specification remains decisive. A certificate alone is not proof of consistent production.
Compliance comparison should include product standards, traceability, marking, packaging, and destination-specific documentation.
Confirm whether EN 10204 3.1 certificates, pressure tests, or third-party inspection are required before shipment. Calculate total cost, including machining, welding labor, coating, freight, customs, rejects, and replacement delays. The cheapest fitting may become costly after one failed installation. Use a supplier audit, sample order, and clear acceptance plan. No checklist is perfect. Our estimates can miss field conditions, especially changing corrosion rates or difficult access. Leave room for technical review.