The 2026 aerosol market is moving toward cleaner, faster, and more adaptable filling systems. A Bov Aerosol Cans Filling Machine supports bag-on-valve production, where the product remains separated from the propellant. This design can serve personal care, household, food-grade, and approved healthcare applications. Every application still requires suitable materials, validated processes, and compliance with local safety standards.
This guide examines the main BOV machine types expected in 2026. It considers manual, semi-automatic, and fully automatic configurations. It also compares inline, rotary, and monoblock arrangements. Practical details matter here. A stainless-steel frame may resist corrosion, but it does not guarantee reliable performance. The filling valve, crimping station, pressure tester, and control system must work together. Small errors can appear as uneven product weights, weak seals, or inconsistent spray patterns.
Real production experience shows that speed alone is a poor purchasing measure. A line claiming 3,000 cans per hour may perform differently after changeovers, cleaning, and operator checks. Think beyond the brochure. Product viscosity, container dimensions, valve specifications, and batch sizes influence the final choice. Safety interlocks, pressure monitoring, guarding, and traceable records should receive equal attention. These features protect people and improve process confidence.
No machine is perfect.
This overview aims to help manufacturers evaluate equipment with clearer expectations. It highlights strengths, limitations, maintenance needs, and suitable production conditions. Some comparisons remain difficult because suppliers use different testing methods. That uncertainty deserves careful review. A reliable decision should combine factory trials, technical documentation, service support, and total operating cost.
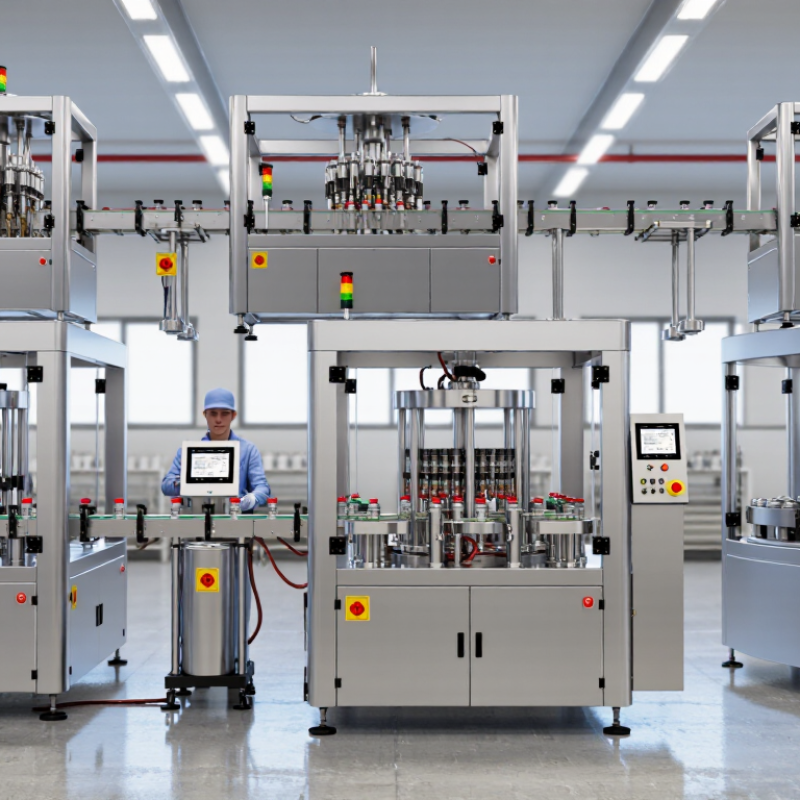
The 2026 BOV aerosol can market is moving toward flexible filling systems. BOV means bag-on-valve, where the product stays inside a sealed bag. Propellant surrounds it and pushes the contents outward.
A 1-inch valve supports faster product transfer and easier equipment alignment. Rotary BOV filling machines suit high-volume lines. Intermittent machines offer better control for smaller batches.
Modern systems can insert the bag, dose the product, crimp the valve, and charge the propellant with fewer manual steps.
The European Aerosol Federation reported more than 5 billion aerosol units produced in Europe during 2023. That scale increases pressure for stable output and lower material waste.
BOV packages can spray at almost any angle, including upside down.
This 360° use helps empty awkward areas inside a container. Some technical reports cite evacuation rates of up to 98%, but the result depends on viscosity, valve design, bag shape, and filling accuracy. The number is not automatic. It needs testing.
In practice, operators should check spray consistency after storage, transport, and repeated use. A weak crimp can cause leakage.
Excessive filling speed can also trap air or deform the bag. Inline inspection, calibrated dosing pumps, and leak testing improve process reliability.
Yet even advanced machinery needs adjustment. Real production conditions rarely behave perfectly.
2026 Top BOV Aerosol Cans Filling Machine Types
Liquid-product BOV filling lines demand controlled handling from the first pump stroke. The product enters a preformed bag, while operators monitor temperature, viscosity, and fill weight. A stable feed system prevents splashing, foam, and trapped air. Small changes matter.
Some machines fill the bag before valve placement. Others crimp the valve first and fill through its stem. The correct method depends on the bag material, liquid thickness, and required dose. Sensors check each container’s weight, while pressure tests help identify leaks. In practice, a perfectly smooth process is rare. Product residue may collect around the filling nozzle.
Valve placement requires accurate alignment. The valve must sit evenly on the can opening before crimping begins. A misaligned valve can create an uneven seal or poor actuator performance. Crimping pressure, depth, and diameter should follow validated specifications. Operators should inspect samples under consistent lighting and record every adjustment.
Reliable lines combine mechanical precision with practical experience. Cleaning procedures must protect seals, pumps, and contact surfaces. Batch records should include rejected units, downtime, and unusual material behavior. These details often reveal problems earlier than automated alarms. A short trial run is useful, but it cannot replace long-term process review.
| Machine Type | Primary Function | Typical Output | Suitable Product Viscosity | Typical Fill Accuracy | Recommended Applications |
|---|---|---|---|---|---|
| Semi-Automatic BOV Bag Filling Machine | Fills liquid or semi-liquid product into preformed BOV bags before valve assembly. | 8–20 bags/min | 1–5,000 mPa·s | ±1.0% to ±2.0% | Pilot production, laboratory batches, seasonal products, and low-volume packaging. |
| Automatic BOV Bag Filling Line | Automatically indexes bags, doses product, checks fill weight, and transfers bags for valve placement. | 30–80 bags/min | 1–10,000 mPa·s | ±0.5% to ±1.0% | Personal-care liquids, household products, food-grade sauces, and water-based formulations. |
| BOV Valve Placement Machine | Places the metering valve onto the filled bag and aligns the valve with the can opening. | 40–120 cans/min | Product-dependent | Positioning tolerance typically ±1 mm | High-speed assembly of BOV valves, bags, dip tubes, and aerosol can components. |
| Automatic Valve Crimping Machine | Crimps the valve cup to the can neck to create a mechanically secure and pressure-resistant seal. | 40–150 cans/min | Not viscosity-limited | Crimp diameter commonly controlled within ±0.05 mm | BOV cans requiring repeatable valve retention, leak prevention, and controlled crimp dimensions. |
| Integrated BOV Filling, Valve Placement and Crimping Line | Combines bag filling, can loading, valve placement, crimping, coding, and in-line inspection. | 60–180 cans/min | 1–10,000 mPa·s | Fill-weight control typically ±0.5% | Continuous commercial production where synchronized handling and reduced operator intervention are required. |
| Servo-Driven High-Precision BOV Line | Uses servo dosing, electronic torque or crimp monitoring, recipe control, and automated rejection. | 100–240 cans/min | 1–20,000 mPa·s with suitable pump selection | Typically ±0.3% to ±0.5% | Large-scale production requiring traceability, consistent dosing, automated quality checks, and rapid changeovers. |
| Key selection factors: product viscosity and foaming behavior, bag material compatibility, can and valve dimensions, target line speed, crimp specifications, cleanability, pressure testing, fill-weight verification, and applicable aerosol packaging regulations. | |||||
Pressure-filling machines for bag-on-valve aerosol cans commonly cover 6–120 cans per minute. The correct range depends on valve design, product viscosity, can diameter, and operator handling. At low speed, technicians can watch each can closely. At 120 cans per minute, timing becomes less forgiving. A pressure-filling line must control propellant pressure, product volume, and valve seating with consistent accuracy.
The European Aerosol Federation reported more than 5.5 billion aerosol units produced in Europe during 2023. That volume shows why stable filling and reliable inspection matter. Industry packaging assessments from Smithers also identify automation, lightweight containers, and improved quality control as continuing market priorities. In practical use, a pressure sensor should confirm the filling cycle, while a calibrated scale checks product weight. Small deviations can reveal blocked valves or unstable pressure.
Leak testing is not an optional finishing step. It may use a warm-water bath, pressure decay, or another validated method suited to the container. EN 14847 provides guidance for aerosol can testing, but plant procedures still require documented validation. A 120-cpm claim can look impressive. It does not guarantee dependable output. Line speed often falls when cans require longer stabilization or repeated testing. I would verify real production samples, not only the machine specification. Even careful systems need review, because seal defects may appear after filling rather than immediately.
Cold-filling machines are designed for propellant handling near −20°C, where moisture and temperature changes become serious concerns. At this temperature, seals can stiffen, hoses may lose flexibility, and pressure readings may fluctuate. A reliable system uses insulated lines, low-temperature-rated gaskets, and continuous temperature monitoring. The filling head should control dosage without creating sudden pressure changes inside the can. ATEX safety controls are equally important. The machine should support proper zoning, certified electrical components, grounding, and controlled ventilation. Ignition risks must be assessed before installation.
Tips: Check every seal after a cold start. Inspect bonding cables before each shift. Use calibrated sensors, not assumptions. Keep an inspection record. A simple checklist often catches loose connections or unexpected frost. Staff should understand emergency isolation and safe restart procedures.
In practical testing, the first cycle may not represent stable performance. Allow the system to reach thermal balance before judging accuracy. This detail is easy to overlook. Operators should monitor fill weight, line pressure, surface temperature, and valve response together. A pressure value alone can mislead. Frost around a fitting may indicate insulation failure, a loose connection, or an incorrect process setting. Stop and investigate. Equipment selection should also consider cleaning access, maintenance intervals, and verified safety documentation. Some designs look efficient but become difficult to service in winter conditions.
BOV filling lines usually fall into linear and rotary types. Linear machines suit flexible production and frequent format changes. Rotary machines deliver steadier output for high-volume contracts. Reported speeds vary widely, from about 30 to 200 cans per minute. The real figure depends on bag insertion, crimping, propellant charging, and inspection stations. Grand View Research valued the global aerosol cans market at approximately USD 11.5 billion in 2023. That scale increases pressure on uptime, but speed alone is not a selection standard.
EN 14847 mainly defines dimensional requirements for tinplate aerosol containers. It does not replace complete process validation or equipment safety assessment. Check neck dimensions, body diameter, height, and crimp compatibility before approving a machine. Container testing should include leak detection, crimp inspection, pressure checks, and sample burst testing through qualified procedures. FEA market statistics reported more than five billion aerosol units filled in Europe in 2023. Consistent testing therefore matters, even for smaller plants. A perfect speed claim can mislead.
Tips: Request a witnessed factory test using your actual BOV cans. Record cans per minute, reject rates, fill-weight variation, and changeover time. Ask for EN 14847 dimensional records, not only a compliance statement. Leave testing capacity in the layout. It is often forgotten.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru