Flaking Mill technology is becoming more important as grain processors, feed producers, and oilseed plants seek higher throughput with tighter energy control. The FAO Food Outlook highlights continuing pressure on global food and feed supply chains, while the USDA Oilseeds: World Markets and Trade reports show the strategic importance of efficient soybean and oilseed processing. These trends make reliable equipment selection more than a purchasing exercise.
This 2026 guide reviews leading Flaking Mill manufacturers and suppliers through practical criteria. We consider processing capacity, roll diameter, flake uniformity, steam conditioning, power consumption, maintenance access, and spare-parts support. A machine may look impressive in a brochure. Its real value appears beside a noisy gearbox, warm bearings, and uneven flakes after long production shifts. Supplier experience matters, especially when a plant handles changing moisture levels or different grain varieties.
Independent verification remains essential. Technical claims should be checked against test results, factory documentation, warranty terms, and applicable safety requirements. ISO-certified production can support quality control, but certification alone does not guarantee strong field performance. The comparison is not flawless. Published capacities often depend on raw material conditions, operator skill, and product specifications. That detail is easy to miss.
Readers should therefore treat this list as a structured starting point, not a final verdict. The best supplier combines sound engineering, transparent communication, responsive service, and measurable results. In 2026, reliability may matter more than the lowest quotation. A cheaper mill can become expensive when downtime interrupts every truck, silo, and production schedule.
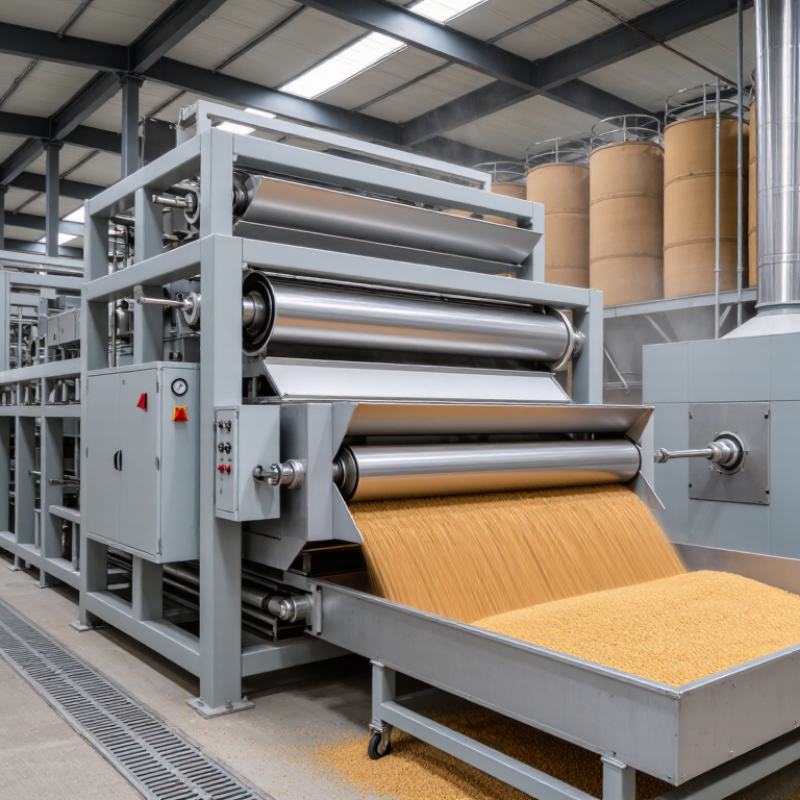
A flaking mill converts conditioned grain into thin, even flakes for efficient processing. The common target is 0.25–0.5 mm. This range requires stable roll pressure, controlled moisture, and accurate feed distribution. A 3–8 t/h capacity suits many medium-scale processing lines. However, rated capacity depends on grain type, moisture content, and flake thickness.
In practical operation, grain should enter the rolls continuously, without sudden surges. Uneven feeding creates thick edges and excessive powder. Operators should check the roll gap during every shift. A simple thickness gauge can reveal changes faster than visual inspection. Conditioning temperature also matters. Grain that is too dry may crack, while excess moisture can cause sticking and unstable throughput. Clean rolls help maintain consistent friction.
Not every machine reaches its advertised output.
A reliable supplier should provide test data for 0.25–0.5 mm flakes, not only maximum capacity figures. Ask about roll diameter, motor load, gap adjustment, spare parts, and maintenance access. During acceptance testing, collect samples at several points in the same hour. Measure thickness variation, fines, and actual throughput. One trial may look excellent, yet fail after a longer run. That weakness deserves attention. Good technical support should explain these limits clearly and recommend settings for the specific grain being processed.
| Technical Dimension | Recommended Benchmark | Typical Operating Range | Why It Matters |
|---|---|---|---|
| Finished flake thickness | 0.25–0.50 mm | 0.20–0.80 mm | Thin, uniform flakes improve heat transfer, hydration, and digestibility while limiting excessive fines. |
| Nominal capacity | 3–8 t/h | 1–12 t/h | Actual output depends on raw material, moisture, target thickness, roll loading, and conditioning time. |
| Application materials | Maize, wheat, barley, oats, and oilseeds | Cereals and selected oilseed products | Roll configuration and conditioning requirements should be matched to the material being processed. |
| Flaking roll diameter | 600–1,000 mm | 400–1,200 mm | Larger rolls generally provide greater contact area and higher throughput at comparable peripheral speed. |
| Roll working width | 800–1,500 mm | 500–1,800 mm | Wider rolls can increase capacity, provided feed distribution and roll alignment remain consistent. |
| Roll speed | 250–500 rpm | 200–700 rpm | Speed affects residence time, friction, product temperature, and the balance between flaking and pulverization. |
| Differential roll speed | 1.0:1 to 1.3:1 | 1.0:1 to 1.5:1 | A controlled speed difference helps create shear and improves separation of the material across the roll surface. |
| Feed moisture before flaking | 14–20% wet basis | 12–22% wet basis | The optimum level varies by grain, conditioning method, target product, and downstream process requirements. |
| Conditioning temperature | 60–90°C | 50–100°C | Steam or water conditioning softens the kernel and can reduce roll force, breakage, and energy demand. |
| Main drive power | 90–250 kW | 45–315 kW | Installed power depends on roll diameter, material hardness, moisture, throughput, and desired flake thickness. |
| Roll-gap adjustment | Hydraulic or motorized control | Manual to automatic | Stable gap control is essential for maintaining thickness uniformity and protecting the rolls from overload. |
| Roll surface hardness | Approximately 50–65 HRC | About 45–70 HRC | Hard, wear-resistant surfaces help preserve roll geometry and reduce maintenance frequency. |
| Recommended control features | Load monitoring, automatic gap control, temperature sensors, and emergency protection | Basic to fully automated control | Monitoring improves process stability, product consistency, operator safety, and preventive maintenance planning. |
Note: Values are practical industry reference ranges for preliminary equipment comparison. Final specifications should be confirmed through material testing, process trials, and the supplier’s guaranteed-performance data.
For 2026 purchasing plans, flaking mill manufacturers and suppliers should be compared by roll diameter, not catalog language alone. Industrial models from 400 to 1,500 mm serve very different production realities. A 400–600 mm roll often suits pilot lines, specialty grains, and moderate throughputs. It demands less floor space and usually simplifies maintenance access. Larger 800–1,000 mm machines provide greater working width and steadier feeding for continuous plants. The largest 1,200–1,500 mm models target heavy-duty operations, where structural rigidity, cooling, and drive capacity become decisive. Capacity figures need context. Grain moisture, flake thickness, and raw material density can change output significantly.
A reliable supplier should provide roll drawings, bearing specifications, surface-hardness data, and test conditions for quoted capacity. Ask how the roll gap is adjusted under load. Ask how quickly operators can inspect scrapers and replace wear parts. These details reveal engineering maturity better than polished photographs. On a factory visit, check vibration at operating speed, weld quality, guarding, and access around the rolls. Check the basics. Irregular mechanical noise can expose alignment problems early. Electrical documentation, spare-part availability, and commissioning support also affect lifetime cost. A low purchase price may become expensive when downtime interrupts a feed or cereal plant.
Diameter selection is not a simple scale-up exercise. A 1,500 mm roll may be excessive for a facility with limited power, weak foundations, or seasonal production. Conversely, undersizing a 400 mm unit can create constant bottlenecks and uneven flakes. I have seen specifications built around ideal laboratory material, then struggle with real grain variation. That mistake deserves honest review. Request samples, measured test results, and a written tolerance for flake thickness before signing. Suppliers that explain limitations clearly are often more dependable than those promising maximum capacity without operating conditions.
Industrial flaking mill reference by roll diameter: 400–1,500 mm models
The chart compares common industrial roll-diameter classes with representative roll-face widths and installed drive-power ranges. Values are engineering reference ranges for non-brand-specific equipment and may vary according to material, flake thickness, throughput, and process configuration.
Choosing a flaking mill supplier requires more than comparing motor size. Drive ratings from 55 to 250 kW suit different throughputs, materials, and operating hours. A 55 kW system may serve a small oilseed line, while a 250 kW drive supports heavier continuous production. Ask suppliers for measured capacity data, not optimistic catalog figures. Review motor efficiency, overload protection, cooling, and maintenance access. These details affect energy costs and downtime.
Tips: Request a trial report using your material. Check flake thickness at several roll gaps, such as 0.3, 0.6, and 1.0 millimeters. Confirm whether gap adjustment is manual, hydraulic, or servo-controlled. Small changes can affect moisture release and downstream performance.
Automation should control roll pressure, gap position, motor load, temperature, and alarm history. A reliable system records trends instead of showing only warning lights. Ask whether operators can export production data and adjust settings securely.
Supplier support also matters. Confirm commissioning coverage, spare-part availability, response times, and training content.
No comparison is perfect. I would not select the highest-power machine automatically. A smaller drive with stable control may outperform an oversized unit when the roll gap stays consistent. Insist on documented tests, clear tolerances, and practical service commitments.
In 2026, top flaking mill manufacturers and suppliers will be judged beyond nameplate capacity. Oilseed processors need repeatable flakes, not impressive brochures. A practical target is 90% or higher flake uniformity. This means most particles stay within the specified thickness range. Thin, even flakes improve cooking, solvent contact, and downstream extraction. Small deviations still matter. A few thick pieces can reduce heat transfer and leave residual oil.
Evaluation should begin with witnessed trials using the buyer’s soybean, rapeseed, or sunflower seed. Record moisture, seed temperature, feed rate, roll pressure, and roll gap. Then collect samples at the start, middle, and end of production. Sieve analysis and thickness checks reveal whether quality remains stable. Ask suppliers for calibration records, wear limits, and maintenance response times. Experienced teams also inspect flake edges, fines, and roll surface condition. Numbers need context. A 92% result from one clean sample proves little.
Reliable suppliers explain how their mills handle changing moisture and seasonal seed hardness. They should provide operator training and clear acceptance criteria. Request data from repeated runs, not one demonstration. Some results may fall below 90% during setup. That is not automatically a failure. It signals a need to adjust conditioning, pressure, or feed distribution. We should also question our test design. Poor sampling can make a strong mill look weak, or hide instability.
Selecting a flaking mill supplier in 2026 requires more than comparing machine prices. Examine ISO 9001 certification, audit scope, and certificate validity. Quality systems should cover design, machining, assembly, testing, and corrective actions. Ask for recent inspection records and sample factory acceptance test reports. Practical evidence matters.
ATEX compliance deserves careful review when mills operate in potentially explosive dust environments. Confirm the equipment category, zone suitability, documentation, and maintenance instructions. A supplier should explain how rollers, drives, sensors, and electrical cabinets meet the stated requirements. Local regulations may add conditions. Do not assume one certificate covers every installation.
Tips: Request a realistic lead-time schedule, including engineering approval, production, testing, packing, and shipping. Check spare-parts availability in your region. Ask who responds during commissioning and how quickly remote support begins. Service promises sound useful, but response times should be written into the agreement.
Speak with previous users about temperature control, roller alignment, and product consistency. A reliable supplier can discuss operating limits without hiding weaknesses. Lead time should include contingency for delayed components. The shortest quote is not always the safest choice. Still, long delays can damage production planning. A balanced review should consider lifecycle cost, operator training, documentation quality, and technical communication. Some evaluations remain uncertain until factory testing. That uncertainty should be recorded, not ignored.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru