Choosing High Alumina Castable is not a simple matter of selecting the highest alumina percentage. Furnace temperature, slag chemistry, abrasion, installation method, and drying control can change performance dramatically. A 1,500°C kiln lining may still fail early if excess water creates pores or uneven curing leaves weak zones behind. Small details matter.
The World Steel Association reported approximately 1.88 billion tonnes of crude steel production worldwide in 2024. This scale supports continuing demand for reliable refractory linings, especially in steel, cement, nonferrous metals, and waste-treatment plants. Meanwhile, Grand View Research identifies the global refractories market as a multi-billion-dollar industry, with continued growth linked to industrial production and infrastructure investment. These figures show market importance, but they do not prove that one castable fits every furnace.
Dr. G. Routschka, a recognized refractory author, emphasizes a practical principle: “Refractory selection must begin with service conditions, not product labels.” That advice deserves attention. High alumina Castable should be judged through chemistry, bulk density, strength after firing, thermal-shock resistance, and installation consistency. A product containing 80% alumina may outperform a 90% grade in one zone, yet fail in another exposed to aggressive slag. Product data sheets also need careful questioning. Laboratory results are useful, but field behavior can differ. This guide presents seven practical tips for comparing grades, checking technical evidence, and avoiding costly assumptions before installation. No perfect choice exists. The better choice matches the furnace.
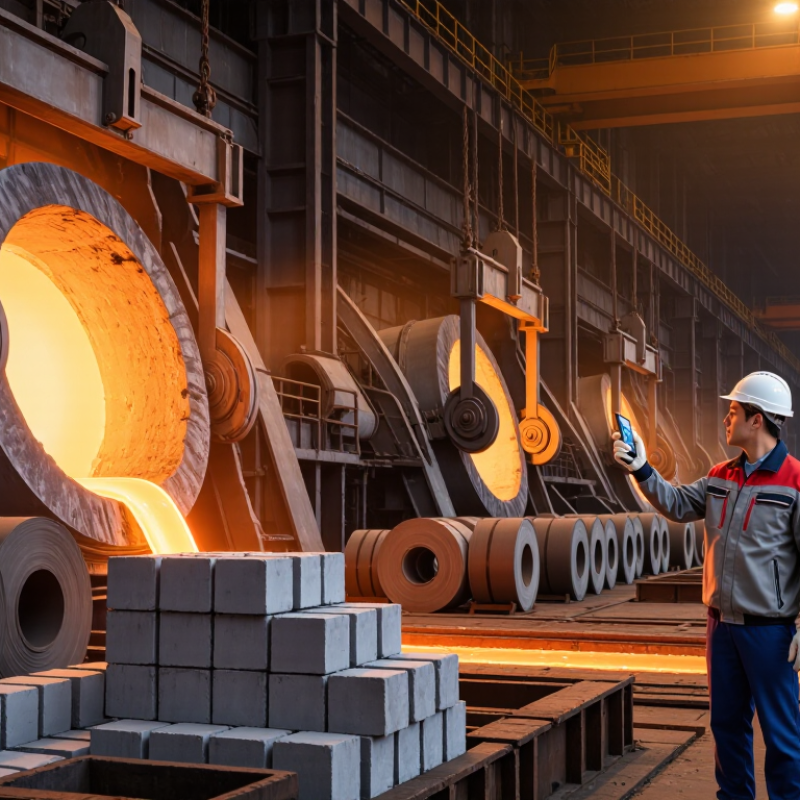
7 Tips for Choosing High Alumina Castable
High alumina castable is a monolithic refractory containing over 45% Al2O3, commonly classified by alumina content and performance. It uses alumina-rich aggregates, cement or alternative binders, and carefully graded powders. Its main applications include steel ladles, tundish linings, cement kilns, furnace hearths, and nonferrous-metal equipment. The demand is substantial. The USGS Mineral Commodity Summaries 2024 estimated global cement production at about 4.1 billion metric tons in 2023. World Steel Association data recorded approximately 1.89 billion tonnes of crude steel that year. These industries require linings that resist heat, abrasion, chemical attack, and repeated thermal cycling.
Choose the alumina grade for the actual duty, not only the highest percentage. Check service temperature, slag chemistry, load, and abrasion level. Review cold crushing strength and permanent linear change after firing. A low-cement or ultra-low-cement formula can reduce porosity, but it demands better mixing and curing control. Particle grading matters. Poor grading may leave weak pores around large aggregates. Installation is equally important. Use clean water, accurate dosing, proper vibration, and controlled drying. Never assume a datasheet predicts field life perfectly. Site moisture and operator technique can change results.
Ask for batch traceability and independent test records. Compare abrasion loss, thermal-shock behavior, and chemical resistance under similar test conditions. Some specifications look impressive but omit test temperatures or curing periods. That deserves questions. Pilot panels can reveal cracking before a full shutdown project. A practical choice balances alumina content, installation risk, availability, and total maintenance cost.
| No. | Selection Dimension | What High Alumina Castable Means | Typical Data or Reference Range | Why It Matters | Main Applications |
|---|---|---|---|---|---|
| 1 | Confirm the alumina grade | High alumina castable is a monolithic refractory concrete containing a high proportion of alumina-bearing aggregates and fine powders, usually bonded with calcium aluminate cement or another suitable binder. | Al2O3 content is commonly above 45% by mass. Commercial grades may range approximately from 45% to more than 90%, depending on the raw materials and intended service. | Higher alumina generally improves refractoriness, resistance to molten materials, and performance at elevated temperatures, but it may also increase cost and installation requirements. | Steel ladles, furnace linings, kiln components, incinerators, non-ferrous metal furnaces, and high-temperature heat-treatment equipment. |
| 2 | Match the maximum service temperature | The suitable castable must retain strength and volume stability under the actual operating temperature, including heat-up and shutdown cycles. | Many high alumina castables are designed for service temperatures of approximately 1,400–1,800°C; the exact limit depends on chemistry, porosity, cement content, and operating conditions. | Selecting only by alumina percentage can be misleading. The rated service temperature and test method should be checked together with the operating temperature. | Reheating furnaces, soaking pits, kiln linings, burner blocks, furnace roofs, and hot zones exposed to continuous or intermittent heat. |
| 3 | Evaluate chemical and slag resistance | Resistance depends on alumina content, calcium oxide level, matrix design, aggregate quality, and the chemistry of slag, ash, gases, or molten metal. | For severe chemical exposure, low-cement or ultra-low-cement formulations are often considered because they can provide a denser matrix and lower open porosity than conventional castables. | Incompatible chemistry can cause penetration, dissolution, spalling, or accelerated corrosion even when the material has adequate refractoriness. | Cement kilns, steelmaking vessels, slag lines, ash-handling zones, waste-incineration chambers, and non-ferrous smelting equipment. |
| 4 | Check physical properties | Important physical properties include bulk density, apparent porosity, cold crushing strength, permanent linear change, thermal conductivity, and abrasion resistance. | Typical bulk density may be about 2.2–3.0 g/cm3, while apparent porosity may be roughly 15–25%. Actual values vary significantly by grade and test temperature. | Higher density and lower open porosity usually support better resistance to penetration, while abrasion resistance is essential where solid particles or high-velocity gases are present. | Cyclone sections, clinker coolers, furnace hearths, transfer chutes, burner areas, and locations exposed to mechanical wear. |
| 5 | Choose the correct installation method | Castables may be installed by conventional casting, vibration casting, pumping, or dry gunning, depending on the formulation and site conditions. | Water addition must follow the technical data sheet. Excess water increases porosity and can reduce strength; insufficient water may prevent proper placement and consolidation. | Mixing time, water quality, vibration, layer thickness, ambient temperature, curing, and drying directly affect the final lining performance. | Maintenance repairs, complex-shaped linings, large furnace floors, boiler areas, kiln shells, and sections requiring fast installation. |
| 6 | Review dry-out and thermal-shock requirements | Castable linings contain mixing water that must be removed gradually before reaching high temperature. Thermal-shock resistance depends on microstructure, thickness, elastic properties, and operating cycles. | A controlled multi-stage dry-out schedule is normally required. The exact schedule should be based on castable thickness, lining design, moisture measurement, and the applicable technical data sheet. | Rapid heating can generate steam pressure and cause explosive spalling. Repeated heating and cooling can produce cracking if the grade is not suited to thermal cycling. | Intermittent furnaces, kiln doors, burner quarls, boiler linings, heat-treatment units, and equipment subject to frequent starts and stops. |
| 7 | Verify quality control and technical documentation | A reliable selection should be supported by a consistent formulation, batch traceability, test results, storage instructions, installation guidance, and service-condition recommendations. | Request data for chemical composition, particle size, bulk density, apparent porosity, strength, permanent linear change, thermal conductivity, shelf life, and recommended water addition. | Laboratory values provide a basis for comparison, but field performance also depends on design, workmanship, dry-out, operating atmosphere, and maintenance practices. | All industrial refractory installations, especially safety-critical furnace linings and high-wear or chemically aggressive zones. |
High alumina castable performance begins with alumina content, but the percentage alone does not tell the whole story. A higher value usually supports better refractoriness and wear resistance. However, poor particle grading can still cause cracking, weak bonding, or difficult installation. Check the stated alumina content and ask whether it is measured consistently by a recognized laboratory method.
Look closely at the raw materials. High-quality calcined alumina should show stable chemistry, low impurities, and controlled particle sizes. Excessive iron oxide, alkalis, or moisture may reduce service life in demanding furnace areas. I have found that a simple sample inspection can reveal uneven color, hard lumps, or dusty contamination. These signs deserve questions. They do not always prove failure, but ignoring them is risky.
Request a recent test report, not an old product sheet. Compare alumina content, bulk density, cold crushing strength, permanent linear change, and water demand. Test a small batch when the application is critical. Follow the mixing instructions carefully, because even excellent raw materials can fail after excessive water addition or poor curing. One practical mistake is trusting a single laboratory result. Production batches can vary, so supplier quality records and independent verification both matter. Ask for traceability from raw material delivery to finished castable. That detail may seem minor. On site, it can save considerable trouble.
Match refractory performance to operating conditions, not only alumina percentage. The European Commission’s JRC BAT Reference Document reports cement kiln burning zones near 1,450°C. Select a castable rated above the real service temperature, with a safety margin. Check alumina content and calcium aluminate cement levels. Higher alumina can improve refractoriness, but it may reduce thermal shock tolerance. That trade-off is often underestimated.
Measure abrasion, chemical attack, and load-bearing demand. Cement clinker, alkalis, and dust can penetrate an unsuitable matrix. ASTM C401 provides classification methods for refractory castables, including strength and service performance. Ask for permanent linear change data after firing. Excessive shrinkage can open joints. It happened in one maintenance trial I reviewed. The material was strong, but the installation cured too quickly.
Match water demand to placement conditions. Low-cement castables usually need accurate mixing and controlled vibration. Test flow, working time, and dry-out requirements before approval. The U.S. Department of Energy reports that industrial furnaces commonly lose significant energy through walls, doors, and openings. A dense, properly installed lining can reduce heat transfer, but density alone is not enough. Consider thermal conductivity, anchor design, thickness, and repair access. Request test reports, batch traceability, and independent laboratory results. Small field trials remain valuable.
Tip 1 Evaluate installation conditions before selecting a high alumina castable.
Check substrate temperature, anchor layout, mixing water, vibration access, and weather exposure. Many technical datasheets specify only 3–5% water by mass, but the correct value remains product-specific. Extra water improves flow briefly. It can later increase porosity and cracking.
Tip 2 Treat curing as a controlled chemical stage, not simple air drying.
Maintain moisture and temperature according to the technical datasheet. ASTM C401/C401M classifies refractory castables by composition and performance, but it does not provide one universal curing schedule. Record ambient temperature, mixing time, and curing duration. Small records prevent large arguments.
Tip 3 Design the dry-out around free-water removal and steam pressure.
A practical schedule may use staged holds near 110°C and 300°C, with heating rates around 25–50°C per hour. However, lining thickness, furnace geometry, and cement content can change these values. API 936 requires documented dry-out control for many industrial refractory applications. Use thermocouples at the coldest and thickest sections, not only near the burner.
The U.S. Geological Survey reported more than 390 million metric tons of global bauxite production in 2023, showing the scale of alumina-based raw materials. Yet raw-material scale does not guarantee installation quality. In field work, rushed heating remains a common failure point. A slower schedule may feel inefficient. It is often cheaper than replacing a spalled lining.
Supplier reliability should be judged through evidence, not polished promises. Ask for recent test reports, batch records, production capacity, and customer references. A dependable supplier can explain alumina content, cement level, particle grading, and recommended water addition clearly. Request a sample and compare its workability after mixing. Small differences matter.
Cost requires a wider calculation. Compare the quoted price with freight, packaging, installation labor, drying fuel, and possible downtime. A cheaper castable may need more water or produce greater shrinkage. That can increase repair work later. Check yield per ton, service temperature, abrasion resistance, and expected campaign life. Do not trust one laboratory result. Ask whether testing reflects actual operating conditions.
Service support often separates a useful supplier from a difficult one. Confirm response times before ordering. Technical staff should provide mixing procedures, vibration guidance, curing conditions, and a controlled dry-out schedule. They should also investigate failures instead of blaming installation immediately. In my experience, written instructions prevent many avoidable mistakes, but they cannot replace site judgment. Discuss spare material, storage limits, and claim handling in advance. I once underestimated delivery risk during a shutdown. The castable quality was acceptable, but late arrival caused expensive pressure. Reliability includes logistics. Examine every promise.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru