Choosing Filter Media For Silicon Industry applications is not a routine purchasing decision. It affects product purity, equipment uptime, water consumption, and worker protection. Semiconductor and photovoltaic plants now operate with tighter contamination limits and more complex chemical processes. The Semiconductor Industry Association reported global semiconductor sales of $627.6 billion in 2024, an annual increase of 19.1%. This growth increases pressure on filtration systems across wafer fabrication, polysilicon production, and supporting utilities.
The IEA’s Renewables 2024 report also highlights continued expansion in solar photovoltaic manufacturing. That expansion requires stable supplies of ultrapure water, process chemicals, compressed air, and high-quality silicon feedstock. Small filter failures can create visible problems: particles on a wafer, pressure spikes across a housing, or cloudy rinse water after cleaning. These details matter.
Seven practical tips can help engineers select media more reliably. The decision should begin with particle size, chemical compatibility, temperature, flow rate, and required cleanliness. Polypropylene, PTFE, PES, stainless steel, and ceramic media each serve different conditions. A membrane that performs well in water may fail in aggressive solvents or hot process streams. That is easy to overlook.
Performance data must come from credible manufacturers, independent testing, and site-specific trials. Certificates alone are not enough. Real process conditions can expose weaknesses. Operators should review extractables, pressure drop, retention efficiency, service life, and disposal requirements before approval. The SEMI International Standards program provides useful industry context, but no standard replaces validation on the actual production line. Good selection is careful, measurable, and occasionally revised when the first choice proves imperfect.
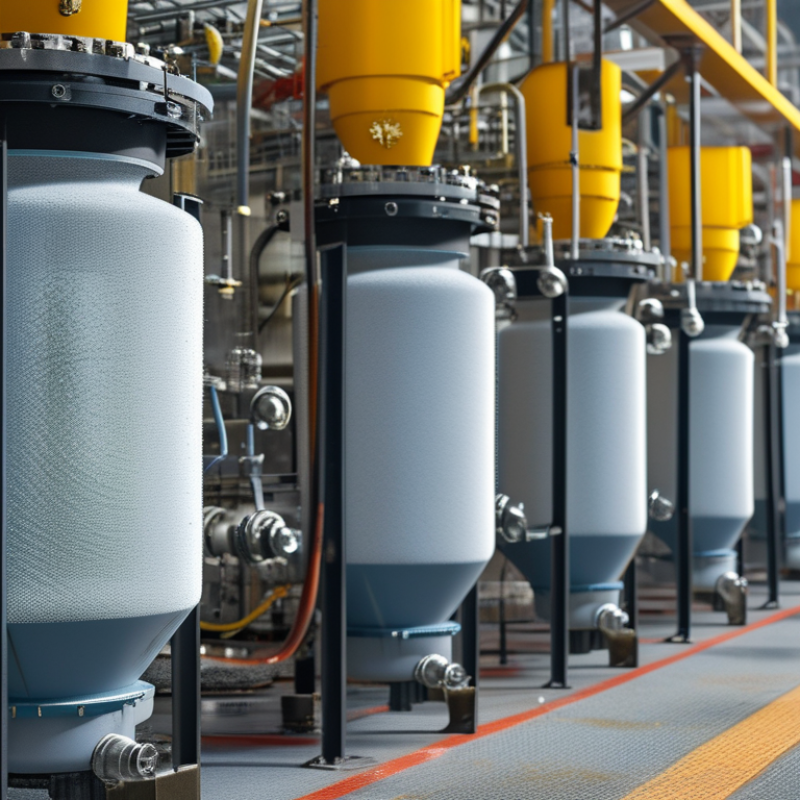
Silicon manufacturing depends on filtration that matches each process stage, not simply the finest available media. A filter must capture particles without restricting valuable flow. Particle size distribution matters. A process may contain fine powder, gel-like residues, or hard fragments from equipment wear. These materials behave differently.
Process engineers should examine chemical compatibility, operating temperature, pressure, and cleaning methods. A media that performs well in room-temperature water may weaken in an aggressive process fluid. Temperature changes can also affect pore structure and sealing performance. Watch the pressure trend. A steady rise may reveal loading, poor prefiltration, or an unsuitable pore rating. Small details matter.
Flow stability matters most.
In pilot lines, teams often test filter life under real production conditions rather than relying only on supplier data. Samples should be checked before and after filtration, including particle counts and visual residue. The housing, gasket, and media must work as one system. One common assumption deserves review: a tighter filter is not always better. It may increase energy use, shorten service life, and create unstable flow. Operators should record replacement timing, pressure loss, and unexpected process changes. These records support safer decisions and make future media selection more reliable. Still, no test replaces judgment on the production floor.
Choosing filter media for silicon processing starts with chemistry, not catalog convenience. SEMI’s 2024 fab outlook projected approximately $112.8 billion in global semiconductor manufacturing equipment spending. That investment raises the cost of contamination and premature filter failure. Match the media to the fluid’s pH, oxidizers, solvents, and temperature. Check compatibility charts, then confirm performance with a real process sample. A chart is not proof.
Select pore size according to the contaminant and required cleanliness level. Smaller pores can improve particle removal, but they may increase pressure drop and shorten service life. Evaluate extractables, especially in high-purity water, acids, and solvent streams. Measure pressure at startup and near replacement. The International Roadmap for Devices and Systems continues to identify particle and chemical contamination as important yield risks in advanced manufacturing.
Review seven practical points: chemical resistance, thermal stability, pore rating, extractables, pressure loss, cleaning method, and validation data. Confirm whether the medium survives repeated flushing or sterilization-like cleaning cycles. Some materials look suitable until wetting, compression, or temperature changes expose weaknesses. I have seen selection decisions rely too heavily on nominal micron ratings. That is a blind spot. Test retention, flow, and ionic contribution under actual conditions. Keep batch records and compare used media after service. The correct choice is rarely the cheapest filter.
| Tip | Chemical or Process Condition | Suitable Filter Media | Recommended Selection Approach | Important Compatibility Considerations | Process Control Check |
|---|---|---|---|---|---|
| 1 | Hydrofluoric acid and buffered oxide etch | PTFE membrane; polypropylene support components | Use chemically resistant PTFE for particle removal in dilute or concentrated fluoride-based solutions. Select a pore rating according to the required particle-control level, commonly from approximately 0.05 to 0.2 µm for fine filtration. | Avoid untreated glass-fiber media and materials containing silica when exposure, extractables, or dissolution could affect the process. Confirm compatibility with the exact HF concentration and temperature. | Check pressure drop, flow stability, particle counts, and fluoride-related extractables before production use. |
| 2 | Hydrochloric acid, nitric acid, or acidic cleaning solutions | PTFE or polypropylene | Choose PTFE for demanding acid service and polypropylene for many moderate-temperature aqueous acid applications. Use a graded or prefilter stage when the solution contains a high particle load. | Material resistance depends on acid concentration, temperature, exposure time, and mechanical stress. Elastomers, adhesives, and housings may limit compatibility even when the membrane is resistant. | Review chemical compatibility charts for the complete filter assembly, not only the membrane layer. |
| 3 | Sulfuric acid, peroxide mixtures, and oxidative cleaning chemistry | PTFE, with carefully selected polypropylene components where permitted | Use PTFE when strong oxidation and elevated temperature create a demanding environment. Select the filter based on the actual oxidant concentration and operating temperature rather than acid identity alone. | Hydrogen peroxide and hot concentrated sulfuric acid can accelerate degradation of unsuitable polymers, seals, and bonding materials. Nylon and many general-purpose elastomers require special scrutiny. | Perform a soak test or documented compatibility review and monitor discoloration, embrittlement, swelling, and extractables. |
| 4 | Ammonium hydroxide, alkaline cleaning, and SC-1-type solutions | Polypropylene or PTFE; PES may be used for suitable aqueous formulations | Use polypropylene for many alkaline aqueous solutions when temperature and concentration are moderate. Consider PTFE for broader chemical resistance or more severe operating conditions. | Polyethersulfone compatibility can vary with concentration, temperature, and additives. Avoid assuming that water compatibility guarantees resistance to concentrated alkaline chemistry. | Measure flow, pressure drop, pH stability, and organic or ionic extractables after chemical exposure. |
| 5 | Ultrapure water and final rinse filtration | PES or hydrophilic PTFE membrane | Use hydrophilic media to avoid wetting problems and reduce the need for pre-wetting solvents. Select a validated absolute or rated pore size appropriate for the target particle specification. | The filter itself must have low ionic, organic, and particulate extractables. Bacterial retention claims and sterilization compatibility should be verified when microbiological control is required. | Evaluate resistivity, total organic carbon, particle counts, and extractables after flushing and at steady state. |
| 6 | Organic solvents, photoresist-related liquids, and solvent rinses | PTFE; polypropylene may be suitable for selected solvents | Use PTFE for broad compatibility with many common semiconductor solvents. Match the membrane, support layer, housing, seals, and vent materials to the exact solvent formulation. | Solvent compatibility can change with aromatic content, ketones, esters, alcohols, temperature, and pressure. Hydrophobic PTFE may require appropriate wetting procedures for certain applications. | Check wetting behavior, bubble point, flow rate, extractables, and any change in filter dimensions or mechanical strength. |
| 7 | High-temperature operation, sterilization, or repeated chemical cycling | PTFE or polypropylene selected for the validated temperature range | Base the choice on the highest actual temperature, thermal cycling frequency, pressure differential, and sterilization method. Select a safety margin above the normal operating temperature. | Maximum temperature ratings differ between dry, aqueous, solvent, and pressurized service. Repeated autoclave or clean-in-place cycles may reduce mechanical life even when short-term compatibility is acceptable. | Validate cycle life through pressure-hold testing, bubble-point testing, flow testing, and visual inspection after repeated cycles. |
| General validation note: Final media selection should be confirmed using the actual chemical concentration, temperature, pressure, flow rate, exposure time, filter configuration, seal materials, and cleanliness requirements. Conduct a compatibility and extractables evaluation before introducing a filter into a silicon manufacturing process. | |||||
Filter media selection in silicon processing should begin with particle removal goals.
Tip: define the smallest harmful particle before comparing materials. A nominal rating may not capture real retention performance. Ask for tested efficiency data under your actual liquid, temperature, and pressure.
Tip: examine particle loading, not only the first clean test. A filter that blocks quickly can reduce production stability. Track pressure rise during pilot trials. Watch the numbers.
Flow rate needs equal attention.
Tip: match the media’s effective area to the required process volume. Higher flow can increase shear, pressure drop, or particle release. Use the expected viscosity, temperature, and batch size for calculations.
Tip: check flow at the end of service life. Initial performance can look impressive. It may not last. A small pilot system often reveals this weakness earlier than a full installation.
Do not ignore housing geometry, sealing quality, or dead zones.
Purity depends on more than particle capture.
Tip: confirm extractables, ionic contribution, and chemical compatibility with process fluids. Request lot-based certificates and conduct rinse testing before use.
Tip: evaluate media cleanliness after installation.
Tip: inspect whether fibers or fragments appear after pressure cycling.
In my experience, operators sometimes choose the finest media and accept excessive flow loss. That decision needs review.
Tip: balance purity, removal efficiency, service life, and operating cost. Record each result, including failures, because imperfect data can still guide a safer choice.
Filter selection begins with compatibility, not micron size. Match the media with acids, alkaline cleaners, solvents, and ultrapure water. Check extractables, swelling, and temperature limits. A membrane that performs well at 25°C may fail near 80°C. SEMI’s 2023 sustainability guidance places strong emphasis on water quality, reuse, and chemical control across semiconductor facilities. That makes material testing essential, not optional. Request challenge-test data under your actual pH, pressure, and flow conditions. Small oversights matter.
Durability affects both yield and operating cost. Review pressure-drop curves, particle-loading capacity, seal stability, and replacement intervals. The SEMI World Fab Forecast continues to show major global capacity expansion, increasing demand for reliable filtration systems. In a high-volume line, one unexpected changeout can waste labor, process fluid, and production time. WSTS reported global semiconductor sales of approximately 626.9 billion dollars in 2024. The scale is enormous. Yet the cheapest filter is rarely the lowest-cost choice. Calculate total cost per filtered cubic meter, including disposal, energy, cleaning, and downtime. Do not trust a perfect laboratory number. Field conditions are messier.
Use seven checks: chemistry, temperature, flow, pressure, retention, durability, and lifecycle cost.
Pilot testing remains wise. I would still question any media choice based only on supplier curves. Real slurry loading can behave differently. Record differential pressure and particle counts weekly, then revise the specification when evidence disagrees.
Choosing final filter media for silicon processing begins with the actual fluid, not a catalogue. Map the gas or liquid, temperature, pressure, flow rate, and expected contaminants. The media must resist process chemicals without swelling, shedding, or releasing extractables. Confirm particle retention at the required size, then compare pressure drop and usable service life. A high-efficiency medium can still fail if it restricts flow too quickly.
Testing should use process-representative conditions. Measure initial and rising pressure drop, particle counts, flow stability, and chemical compatibility. Inspect samples before and after exposure.
A qualified laboratory can support retention testing and extractables analysis, while plant engineers should verify results against production data.
Small details matter. A clean filter housing can hide poor sealing. I have seen laboratory results look excellent until vibration exposed a gasket problem.
Maintenance needs a written inspection interval, but the interval should remain adjustable. Record installation dates, lot information, differential pressure, cleaning events, and replacement reasons. Avoid handling media with bare hands. Use clean tools and controlled packaging during changeout.
Replace the element when pressure limits, particle trends, or chemical exposure require it. Do not rely on appearance alone. Some damaged media looks normal.
One practical weakness is over-trusting a single alarm threshold; gradual contamination may develop before that limit is reached. Reviewing trends weekly can reveal this earlier, although production teams sometimes skip the review during busy periods. That gap deserves correction.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru