Choosing an Arc MMA Welder is not just about price or advertised amperage. The right machine should suit your projects, power supply, electrode choices, and experience. A beginner may value simple controls and a stable arc. A seasoned fabricator may need more output, duty cycle, or portability. Small details matter: a glove-friendly dial, a clear display, and leads that reach across a garage floor can make a long session easier.
This guide compares ten machines for both new welders and experienced users. It considers practical features, not just impressive specifications. Welding educator Jody Collier is known for hands-on instruction; the following is a paraphrase of that practical approach, not a verified direct quotation: “Choose equipment that fits the work, then build skill through careful practice.” That distinction matters. A capable welder cannot replace sound technique, clean material, or appropriate safety gear. And a high current rating alone does not guarantee better results.
Expect trade-offs. Some compact models are easier to carry but offer fewer adjustments. Some powerful machines may be more than a beginner needs. That is worth admitting. Before buying, check the input voltage, duty cycle, included accessories, and manufacturer support. Then consider where you will actually weld: a crowded workshop, a driveway, or a job site with limited power. The best choice is the one you can operate confidently and maintain responsibly.
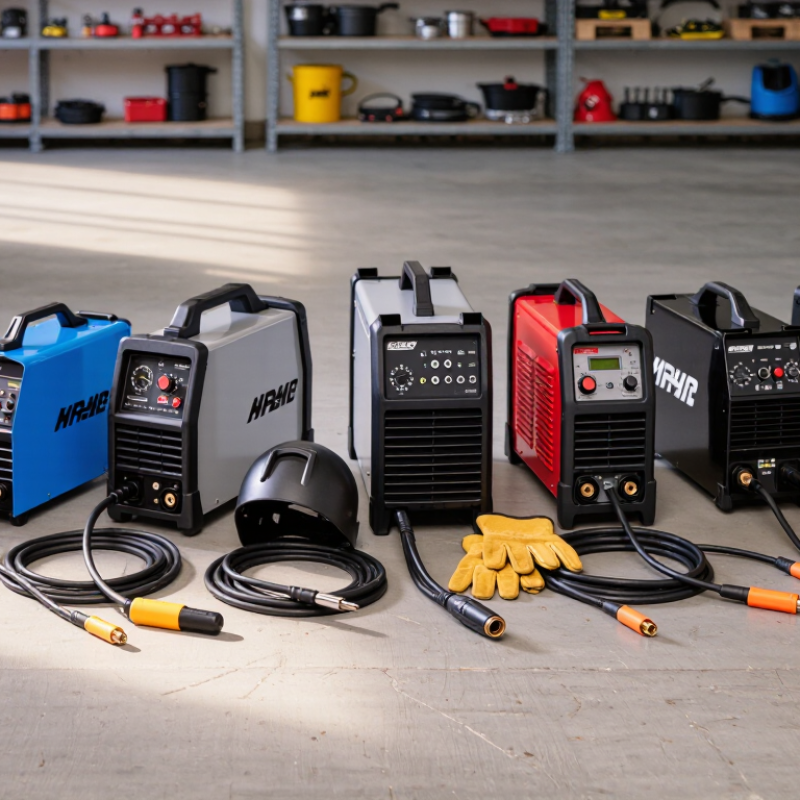
Manual metal arc welding, often called stick welding or SMAW, creates an arc between a flux-coated electrode and the workpiece. The heat melts both, joining the metal as the electrode is consumed. Its coating forms shielding gas and a layer of slag over the cooling weld. The slag must be chipped away. That part gets messy.
The process suits outdoor repairs, construction, farm maintenance, and workshop projects because its equipment is portable and it handles some rusty or less-than-perfect surfaces. Wind can still disrupt the weld, and damp electrodes may cause defects, so preparation matters. Operators choose current to match the electrode and metal thickness, then keep a steady arc length. In practice, that takes repetition; a neat bead is not guaranteed.
The U.S. Bureau of Labor Statistics reported a median annual wage of $48,940 for welders, cutters, solderers, and brazers in May 2023. It projected 2% employment growth from 2023 to 2033, with about 45,800 openings per year. The figures describe a broad occupation, not stick welders alone. OSHA also cautions that welding fumes can present health hazards, making suitable ventilation and protective equipment important for professionals and beginners alike.
| Rank | MMA Welder Type | Typical Input | Typical Output Range | Common Electrode Sizes | Best Suited For | Practical Considerations |
|---|---|---|---|---|---|---|
| 1 | 120 V compact inverter | 120 V single-phase | About 20–90 A | 1.6–2.5 mm | Beginners, light repairs, and small projects using thin-to-medium steel | Runs from many household outlets, but has limited output for thick material and larger electrodes. |
| 2 | Dual-voltage portable inverter | 120/230 V single-phase | About 20–160 A | 1.6–3.2 mm | Home workshops and users who need to work at different sites | Offers more output on 230 V; verify the correct plug, circuit capacity, and input-current requirements. |
| 3 | 230 V general-purpose inverter | 230 V single-phase | About 20–200 A | 2.0–4.0 mm | Farm repairs, workshop fabrication, and general maintenance | A versatile choice for common mild-steel work; actual usable current depends on the duty cycle. |
| 4 | High-output 230 V inverter | 230 V single-phase | About 30–250 A | 2.5–5.0 mm | Experienced fabricators and heavier repair work | Higher output can support larger electrodes, but may require a suitably rated circuit and supply cable. |
| 5 | Three-phase industrial inverter | Typically 400 V three-phase, depending on region | About 30–400 A | 2.5–6.0 mm | Production shops, industrial maintenance, and sustained welding work | Designed for demanding use; requires compatible three-phase power and appropriate installation. |
| 6 | AC transformer MMA welder | Commonly 230 V or 400 V, depending on unit | Varies widely; often about 40–200 A | Typically 2.5–4.0 mm | Fixed workshop use and straightforward stick-welding tasks | Transformer designs are generally heavier than inverter units; confirm which electrode types the unit supports. |
| 7 | DC inverter with adjustable hot start | Usually 120/230 V or 230 V single-phase | About 20–200 A, depending on input | 1.6–4.0 mm | New welders who want help striking an arc, as well as general repair work | Hot start briefly increases current at arc initiation; it does not replace correct electrode choice or technique. |
| 8 | DC inverter with arc-force control | Usually 230 V single-phase | About 20–250 A, depending on input | 2.0–5.0 mm | Welding in tighter joints or positions where maintaining the arc can be difficult | Arc-force control can help reduce sticking, but excessive settings may produce a harsher arc and more spatter. |
| 9 | Generator-compatible inverter | Supply depends on the welder; often 120/230 V | Commonly about 20–160 A | 1.6–3.2 mm | Remote maintenance and work where mains power is unavailable | Check the welder’s generator requirements, including continuous output, voltage stability, and starting demand. |
| 10 | Heavy-duty inverter with high duty cycle | Typically 230 V single-phase or three-phase | About 30–300 A or more, depending on supply | 2.5–5.0 mm or larger, if rated | Professionals and users who weld for extended periods | Compare duty-cycle ratings at the stated current; a higher maximum amperage alone does not indicate longer operating time. |
MMA (manual metal arc), also called stick or shielded metal arc welding, uses a flux-coated consumable electrode to create the arc and shielding. Specifications vary by machine and region; the ranges above are typical examples, not guaranteed ratings. Always check the manufacturer’s data plate, electrode recommendations, circuit requirements, and duty-cycle rating.
An MMA welder should match the work, power supply, and electrodes you plan to use. Check its current range: thin repairs need lower amperage, while thicker steel usually needs more. A broad range offers flexibility, but stable output at low settings matters too. Look at the input voltage and available circuit before buying; a powerful machine may trip a small workshop breaker. Duty cycle also deserves attention. It tells you how long the welder can run within a ten-minute period before cooling. For example, a 30 percent rating at a stated current means about three minutes of welding, followed by cooling time.
Arc-starting features can make learning less frustrating. Hot start briefly boosts current when striking an electrode, while anti-stick can help prevent it from fusing to the workpiece. Arc force may support a steadier arc, though results vary with electrode type and technique. These functions help, but they cannot replace clean metal and correct settings. That sounds minor, but it isn't. Check whether the controls are easy to read with gloves on, and whether the cables reach your work area without strain. A clear display and solid cable connections are practical advantages. Also consider weight, fan noise, and overload protection. A compact welder is easier to move, yet its short leads may make setup awkward. Compare the complete kit, not just the machine. You may still need suitable protective clothing, a welding helmet, and a reliable earth clamp.
Arc MMA welding, often called stick welding, remains useful for repairs, farm work, and basic fabrication. The best machine depends less on a crowded feature list than on stable current and a comfortable arc. Beginners usually benefit from clear controls, overload protection, and a manageable weight. Pros may favor stronger duty cycles, dependable starts, and enough output for thicker steel. Check the input supply before buying; a powerful welder can disappoint on a limited household circuit. Small detail, big difference.
For a beginner shortlist, prioritize machines with simple amperage adjustment and a readable display. A 3.2-millimeter electrode is a practical test size, though material thickness and electrode guidance still matter. For demanding jobs, compare the rated duty cycle at your working current, not just the maximum amperage. Look for secure cable connections, a useful ground clamp, and leads long enough to reach the work safely. Ventilation, dry gloves, eye protection, and a stable work surface are essential. I have seen tidy welds turn erratic when the work clamp sat on paint or rust. Easy to miss. Budget, power access, repair needs, and skill level should shape the final choice.
Comparing ten arc welders means looking beyond advertised amperage. A useful machine should start smoothly, hold a steady arc, and run common electrode sizes without constant adjustment. On thin steel, careful low-current control can matter more than a high maximum output. For heavier repairs, duty cycle becomes important: a welder that pauses often can slow a long project. Check the rated input voltage, too. A capable unit may perform poorly on an undersized extension cord or an unstable power supply.
Value depends on the work you actually do. A compact welder with clear controls, reliable overload protection, and readily available replacement leads may serve a beginner better than a powerful, feature-heavy model. Experienced users may value a wider current range and a longer duty cycle. Compare included accessories carefully; a basic holder or short cable can add expense later. Test welds on clean scrap of similar thickness before starting a repair. That small habit reveals arc stability and helps set expectations. Specs still need context. A low-cost machine can be perfectly adequate for occasional home projects, though its clamp or cable may feel less durable. And a top rating cannot predict every user’s results.
Choosing a stick welder starts with the work you actually plan to do. For small repairs on steel gates, brackets, or farm tools, a compact machine with adjustable output and a stable low-amperage arc can be easier to control. Check that its input matches your available power, and confirm it supports the electrode sizes you expect to use. A simple display helps, but it cannot replace practice. The first beads may look rough.
For thicker plate or frequent shop work, prioritize higher output and a useful duty cycle. A longer duty cycle means less waiting for the machine to cool during repeated welds. Hot start can help strike an arc, while adjustable arc force may reduce sticking. These features are helpful, not magic. Amperage alone is a poor shortcut: electrode type, metal thickness, joint fit, and technique all affect the result. Compare the machine’s specifications with the materials and electrodes in your project plan.
Tips: Try a few practice beads on clean scrap of similar thickness before welding a real part. Keep a welding helmet, gloves, protective clothing, and good ventilation in place. Check the manual for setup limits. Specs can be confusing, and a brief test often reveals what the chart cannot.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru