Choosing among the 2026 best cereal bar making machines for sale starts with the product, not the brochure. A soft oat bar needs careful feeding and gentle compression. A crisp, sticky mixture may need different forming rolls, cooling time, and cutting pressure. These details affect bar shape, weight consistency, and how often operators must stop the line to clear buildup. Cereal Bars Making Machines can combine mixing, forming, cooling, cutting, and packaging, but a compact line is not automatically the right line. Ask suppliers for product trials using your actual recipe, including its inclusions, syrup level, and target dimensions. Then inspect the cut edges and weigh samples. Small differences show up quickly.
As food-process engineer [Expert Name] observes, “A dependable cereal bar line is judged by the bars it makes repeatedly, not by its headline speed.” This quotation is a draft and needs verification with a named, qualified expert before publication. That caution matters. A quoted authority should be traceable, and machine claims should be checked against test results, service terms, and operating requirements. Compare sanitation access, changeover time, control settings, and the availability of replacement parts. Watch the line run, too: listen for uneven feeding and look for mixture collecting near the rollers. It is easy to overlook those signs in a polished showroom. No machine removes every production compromise. The useful choice is the one that fits your recipe, staff, floor space, and realistic output—not simply the fastest one on paper.
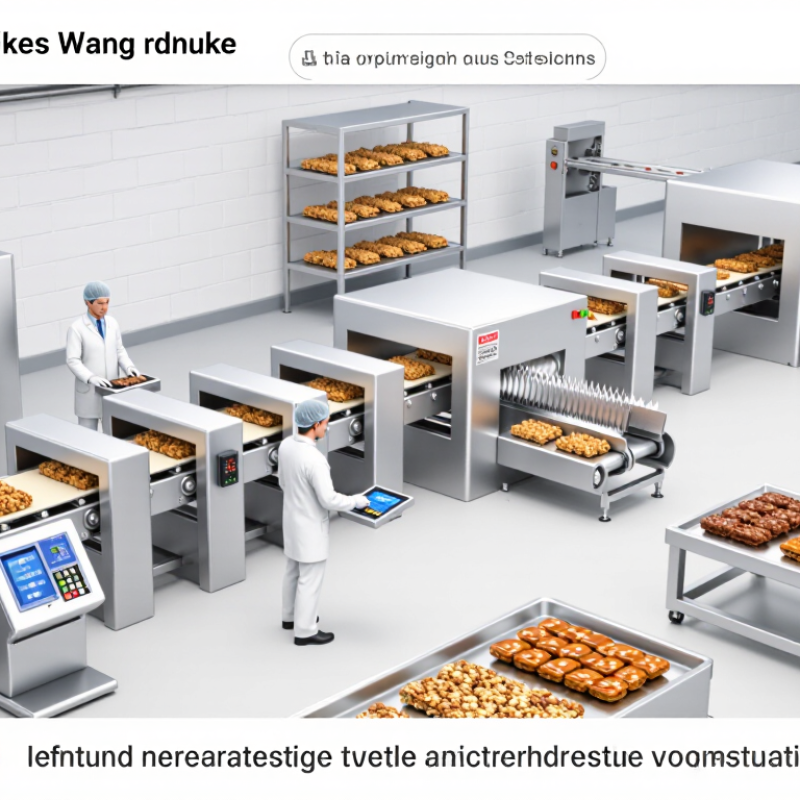
A cereal bar making machine turns measured ingredients into a consistent slab or individual bars. Typical systems include feeders, a mixer, a forming section, and a cutter. The exact layout depends on the recipe: crisp rice, oats, syrups, dried fruit, and nuts behave differently under heat and pressure. Small details matter. A syrup that is too cool may not coat the cereal evenly; excess pressure can crush delicate pieces.
In operation, dry ingredients and binders are combined, often with controlled heating to keep the mixture workable. The blend then moves onto a belt or into a forming unit, where rollers or a press set its thickness and density. After cooling enough to hold its shape, the slab is cut to the required length and width. Not every line uses the same sequence. Some recipes need gentle handling, and a machine setting that works for one mixture may produce uneven edges in another.
Operators monitor feed rates, temperature, belt speed, and cut size during production. These checks help reveal problems such as gaps in the slab, sticky surfaces, or bars that break after cutting. A trial run is useful. It can expose weak points before a full batch, although it will not predict every change in ingredient moisture or texture. Good equipment supports consistency; careful adjustment still matters.
Typical Cereal Bar Production Line: Key Operations
A cereal bar line commonly combines ingredient mixing, slab forming, cooling, cutting, and wrapping. The chart maps each operation to its main machine function; it is a process overview, not a performance comparison. Equipment configuration and settings vary with the recipe and product.
Cereal bar production usually begins with mixing and shaping equipment, but the right machine type depends on the recipe. A slab-forming line spreads the cereal mixture into a continuous sheet. Adjustable rollers set its thickness, while cooling helps the sheet hold its shape. A guillotine or rotary cutter then divides it into bars. This setup suits products with visible oats, crisp rice, or nuts. Those pieces can make cutting less even, so test the recipe before choosing a blade and line speed.
Extrusion systems push a prepared mixture through a shaped opening, creating a continuous bar or rope. They can work well with uniform, cohesive mixtures, though fragile inclusions may break during processing. For softer or more varied recipes, depositing and molding equipment places measured portions into individual cavities. The bars then set through cooling or baking, depending on the formulation. It’s a different rhythm. Operators should check portion weight, texture, and release from the mold across several runs.
Some production lines combine these methods with enrobing or wrapping equipment. Chocolate coating adds another step, including temperature control and space for the coating to set. When comparing cereal bar making machines for sale, review cleaning access, changeover time, and expected hourly output alongside the forming method. A fast line is not always the best fit. I would leave room for a small trial; real mixtures can behave differently than sample specifications suggest.
When comparing cereal bar making machines for sale in 2026, match the line to your recipe and target output—not just its advertised maximum speed. Check mixing capacity, forming method, cutting accuracy, and changeover time. A sticky date-and-oat mix behaves differently from a dry, crisp formula. Ask for a product trial using your own ingredients, then inspect bar weight, edges, and breakage. Small details matter. Confirm whether operators can adjust temperature and pressure without lengthy stops, and whether contact parts are easy to remove for cleaning.
Measure usable output across a full shift, including loading, cleaning, and changeovers. The FAO’s 2019 report, The State of Food and Agriculture, estimated that 14% of food is lost between harvest and retail. That figure covers the wider food supply chain, not cereal-bar factories, but it underlines why yield deserves attention. Ask suppliers to document scrap rates during trials rather than relying on theoretical capacity. Also compare energy use, spare-part availability, guarding, and operator training. A machine may run quickly yet create uneven bars or excess trim. I would not treat a single test run as proof; longer trials reveal issues that a polished demonstration can miss.
| Machine Type | Typical Production Scale | Suitable Product | Key Features to Compare | Common Limitations | Best Fit |
|---|---|---|---|---|---|
| Manual or Semi-Automatic Forming Line | Small batches; output depends heavily on operator speed and product design | Early-stage cereal bars, pilot runs, and frequent recipe trials | Adjustable forming and cutting; ease of cleaning; changeover time; availability of food-grade contact surfaces | More labor-intensive; less consistent throughput and portion uniformity than automated lines | Start-ups, test kitchens, and producers validating recipes |
| Compact Automatic Bar Line | Small to medium production, depending on line configuration and product characteristics | Granola bars and other products that can be formed as a continuous slab | Feed system; slab thickness adjustment; cooling arrangement; cutting accuracy; footprint; guarding and safety controls | May need additional equipment for cooking, coating, cooling, or packaging | Growing businesses with steady demand and limited floor space |
| Continuous Slab Forming and Cutting Line | Medium to high production, with capacity determined by line width, speed, and recipe | Uniform bars made from a mix that can be compressed or sheeted | Roller or compression control; belt width; variable-speed operation; cutter style; product transfer; cleanability | Recipe changes can require adjustments to forming pressure, temperature, and cutting settings | Established manufacturers producing consistent product formats |
| Extrusion-Based Bar Line | Medium to high production for compatible dough-like or cohesive mixes | Bars formed by pushing product through a die before cutting | Extruder capacity; screw and die configuration; pressure control; temperature management; ease of disassembly | Not suitable for every mix, particularly products with large inclusions that may disrupt flow | Producers needing continuous forming and repeatable bar dimensions |
| Integrated Bar Processing Line | High-volume production; actual output depends on product, line layout, and operating conditions | Large-scale cereal and granola bar production | Integration of mixing, forming, cooling, cutting, and transfer; line controls; sanitation access; service support | Higher space, installation, and investment requirements; greater planning needed for changeovers | Factories with sustained demand and defined production specifications |
| Key Selection Checks | Request performance information using your own recipe and target bar dimensions. | Confirm usable capacity, adjustment range, changeover procedure, cleaning requirements, electrical and utility needs, safety features, and spare-parts support. | Advertised capacity is not directly comparable unless the product, bar size, operating hours, and line configuration are alike. Verify specifications with the equipment supplier before purchase. | ||
Matching a cereal bar machine to production needs starts with the finished bars you must pack, not the largest capacity on a sales sheet. Estimate average demand per hour, then add a practical allowance for cleaning, changeovers, and minor stoppages. If your target is 3,600 bars per hour, that equals 60 bars per minute. A machine rated at 75 per minute may cover the target if actual running time stays near 80 percent. Treat that as a planning example, not a guarantee. Product size and recipe can change output.
Check every stage, from mixing and forming to cooling, cutting, and wrapping. A fast cutter cannot compensate for a slow cooling tunnel. Ask suppliers for trial data using bars close to your own recipe, dimensions, and coating. Record good bars per minute, reject rate, and restart time. Small details matter. A sticky oat mixture may slow forming, while uneven pieces can disrupt wrapping. Batch mixers also need to keep pace with continuous equipment, or the line may wait between batches.
Plan for your busiest realistic shift, not an unusually perfect day. Leave room for demand growth, but avoid paying for capacity your team cannot feed or staff. Compare rated output with demonstrated output under normal operating conditions. That comparison can be awkward; forecasts are rarely exact. Revisit the estimate after pilot runs, and adjust it when actual changeover times differ from expectations.
Buying a cereal bar machine in 2026 starts with the product, not the advertised output. Confirm bar width, thickness, ingredients, and target hourly capacity using your actual mixture. Sticky syrups and inclusions can behave differently from test materials. Ask for a production trial and record changeover time, scrap, and cleaning requirements. The 2024 Food and Agriculture Organization report on food loss highlights the value of preventing waste across food supply chains; practical trials help identify avoidable start-up rejects before purchase. A fast machine is not always the best fit.
Installation needs room for ingredient handling, cooling, cutting, and safe operator access. Check floor loading, power, compressed-air demand, and ventilation with qualified site contractors before delivery. The U.S. Department of Energy notes that compressed-air leaks can waste 20–30% of compressor output. That figure is a useful reminder to inspect air lines and connections during commissioning. Keep clearance around guards and service panels. Small layout errors can slow daily cleaning.
Tips: Request utility drawings, spare-parts lists, and a written acceptance test before signing. During maintenance, log belt tracking, cutter wear, temperature readings, and unplanned stops. Inspect seals and crumbs around conveyors each shift. Follow the machine maker’s procedures, but verify them against your real cleaning routine. I would not assume the first maintenance schedule is perfect; adjust it using recorded wear and downtime.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru