Choosing the best China Aluminum Fin Press Machine requires more than comparing prices, tonnage, or catalog photographs. The machine must form consistent fins, protect material thickness, and maintain stable pitch during long production runs. A small error at the die can create uneven heat-transfer surfaces, visible burrs, and expensive coil waste. Sometimes, the cheapest quotation becomes the costliest decision.
The United States Geological Survey reported approximately 70 million metric tons of global primary aluminum production in 2023. The International Aluminium Institute also identifies transportation, construction, packaging, and electrical applications as major demand sectors. These figures show why reliable fin-forming equipment matters. Growing output requires repeatable tooling, controlled feeding, and measurable quality.
Manufacturing quality authority W. Edwards Deming stated, “Quality comes not from inspection, but from the improvement of the production process.” His principle fits every Aluminum Fin Press Machine evaluation. Buyers should examine servo accuracy, press capacity, die life, fin height tolerance, safety systems, commissioning support, and spare-part availability. Ask for production samples, not promises. Inspect the formed fins under practical lighting. Measure pitch with calibrated tools. Record cycle stability across several hours.
No machine is perfect. Even experienced buyers can overlook maintenance access or operator training. This guide compares the technical and commercial factors behind Chinese fin press equipment, while questioning assumptions that often appear in supplier brochures. The best choice is not simply the fastest press. It is the system that delivers stable fins, predictable operating costs, and evidence-based performance.
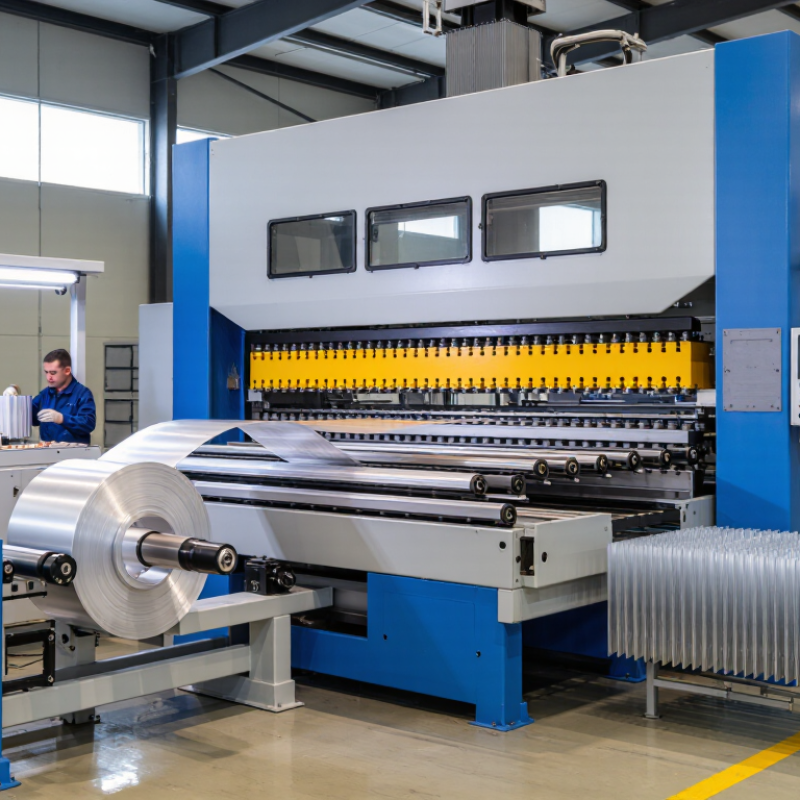
A China aluminum fin press machine is industrial equipment made in China for forming thin aluminum strips into heat-exchanger fins. It usually combines decoiling, feeding, stamping, louvering, cutting, and collection. The press shapes repeated fin profiles through a precision die. Common outputs include flat, corrugated, and louvered fins for radiators, condensers, and evaporators.
The International Aluminium Institute reported global primary aluminum production above 70 million tonnes in 2023. That scale supports a large supplier network, but it does not guarantee machine quality. Buyers should inspect strip-width tolerance, feed accuracy, press speed, die life, and changeover time. In practical testing, a stable feeder matters as much as rated tonnage. A small pitch error can create uneven airflow across a finished coil.
Look closely at the machine.
Technical specifications should state material thickness, maximum strip width, strokes per minute, and acceptable fin height. Energy performance also deserves attention. The International Energy Agency identifies aluminum production as highly energy intensive, so efficient forming and reduced scrap can affect operating costs. Factory acceptance tests should use the buyer’s actual aluminum grade and coil dimensions. This step is often skipped. That is a mistake. A machine may run well with sample stock but struggle with softer or thinner material. Safety guarding, emergency stops, electrical documentation, and spare-die availability should be verified before shipment.
What makes the best China aluminum fin press machine? Its value begins with forming every fin consistently. An aluminum fin press converts thin coil stock into heat-transfer surfaces through a timed die sequence. An uncoiler feeds the strip into straightening rollers. The press then pierces, lances, louvres, and forms the aluminum. A final station cuts each fin to length.
Inside the die, punch clearance controls edge quality and burr formation. Feed accuracy controls fin pitch. Excessive speed can cause wrinkles, cracks, or uneven louvers. The process looks simple. It is not. Operators must match material thickness, temper, lubricant, and tooling pressure. A practical trial should inspect fin height, pitch, flatness, and insertion force. I would not trust a brochure’s strokes-per-minute claim without checking production samples.
Demand for efficient heat exchange is growing. The International Energy Agency’s The Future of Cooling report projects global space-cooling electricity demand could more than triple by 2050, reaching about 6,200 TWh. Reliable fin production therefore matters in air-conditioning and refrigeration manufacturing. Material efficiency also deserves attention. The International Aluminium Institute reports that recycling aluminum uses roughly 5% of the energy required for primary production. A well-adjusted press reduces scrap and protects that advantage. Still, setup waste is often underestimated. A machine that runs slightly slower may deliver better output when fin geometry remains stable.
Thermal Conductivity of Common Aluminum Fin Alloys at Approximately 20°C
Aluminum fin press machines typically feed a coil or sheet, form repeated fin profiles with a punch and die, and then cut or separate the finished fins. Alloy selection affects forming performance and heat transfer. The chart shows commonly used aluminum alloys and their approximate thermal conductivity values; higher conductivity generally supports more efficient heat dissipation, while the machine must also provide accurate feeding, suitable forming force, and consistent fin spacing.
The best China aluminum fin press machine is not defined by speed alone. Its performance depends on specifications matched to your fin design, alloy, and production volume. Start with material thickness, coil width, and temper. A machine designed for thin aluminum may struggle with harder stock. Check press capacity, stroke length, and rated working speed. These values affect forming stability and tool life. Feed accuracy also matters. A small length error can create uneven fin spacing across a long heat exchanger.
Tips: Request a test run with your actual aluminum coil. Measure pitch, height, burrs, and scrap rate. Ask for recorded results, not only catalog numbers.
Servo feeding, encoder resolution, and PLC response influence repeatability. Look for adjustable fin height, pitch, and louver settings. Tooling change time is important when product sizes vary. Guide rollers should hold the strip firmly without leaving marks. Lubrication control can reduce friction, but excessive oil may affect later assembly. In production checks, a slower machine sometimes delivers better output because it creates fewer rejected fins. This is easy to overlook. Noise, vibration, and maintenance access also reveal practical quality. A strong frame helps, but poor alignment can still damage tooling. Consider electrical safety, guarding, emergency stops, and documentation before purchase. I would also leave room for uncertainty: advertised maximum speed may not match stable continuous speed. Ask how performance changes after several hours of operation. Reliable suppliers should explain tolerances clearly and provide service training, spare-part details, and acceptance records.
When comparing China aluminum fin press manufacturers, start with process evidence, not catalog promises. The International Aluminium Institute reported about 70.6 million tonnes of global primary aluminum production in 2023. China contributed roughly 41.4 million tonnes. This scale supports strong supply chains, but it does not guarantee accurate fin forming.
Request a recorded trial using your actual aluminum alloy, thickness, fin height, and pitch. Measure stroke rate, feed accuracy, burr height, fin damage, and finished flatness. Ask for at least eight hours of continuous operation. A machine producing perfect samples for twenty minutes proves very little.
Compare quoted press force, motor power, die life, and energy use. The International Energy Agency identifies aluminum as a highly energy-intensive industrial material, so unnecessary oversizing can increase operating costs. Check whether the manufacturer provides measured consumption, not estimates.
Reliability depends on details. Examine frame weld quality, guide-post alignment, lubrication access, control-system backups, and replacement-part lead times. Ask for failure records and customer references from similar fin sizes. Some suppliers offer attractive prices but weaker inspection documents. That is where evaluation becomes uncomfortable.
I would also verify calibration certificates and acceptance criteria before payment. A lower price may hide slower service or unstable feeding. The best comparison uses identical test conditions, transparent data, and a written response-time commitment. Even then, no factory trial predicts every production problem. Allow a practical margin for material variation and operator learning.
What Is the Best China Aluminum Fin Press Machine?
Buyers should judge an aluminum fin press by measurable output, not nationality or brochure claims. The machine must hold fin pitch, strip width, forming height, and feed length consistently during long production runs. For HVAC coils, even a small pitch error can increase air resistance and reduce heat-transfer performance. Ask for sample parts, dimensional reports, and repeatability data from several operating speeds.
Material compatibility matters. Aluminum fin stock commonly follows ASTM B209 or EN 485 requirements, while the machine’s safety design should align with ISO 12100 and relevant guarding practices. ISO 9001 certification can support process control, but it does not guarantee excellent machine performance. Inspect the press frame, die alignment, lubrication system, sensor protection, and emergency-stop response. Short test runs are insufficient.
Applications vary from air-conditioner evaporators to automotive heat exchangers and refrigeration units. The International Aluminium Institute reports that recycled aluminum uses about 5% of the energy required for primary aluminum production, making scrap control increasingly important. A precise press can reduce burrs, rejects, and unnecessary material loss. I would still question any claimed “zero-defect” rate; real production includes tool wear, coil variation, and operator mistakes. Request maintenance records, calibration procedures, noise measurements, and a clear acceptance test before purchase. A quiet machine is not always a stable machine.
| Evaluation Dimension | Recommended Data or Requirement | Why It Matters | Suitable Applications | Buyer Verification Points |
|---|---|---|---|---|
| Material Compatibility | Aluminum strip or coil suitable for stamping, commonly including heat-exchanger fin stock and other formable aluminum alloys. | The alloy, temper, surface coating, and lubrication condition affect forming force, fin stability, burr formation, and tool wear. | Radiator fins, condenser fins, evaporator fins, HVAC heat exchangers, and industrial cooling units. | Request a material compatibility statement and confirm the required alloy, temper, coil width, and surface condition before ordering. |
| Material Thickness | Typically about 0.05–0.30 mm for many heat-exchanger fin applications; the actual range depends on the die and product design. | Thickness directly influences press tonnage, feed accuracy, fin height, pitch, and the required clearance between punch and die. | Thin high-density fins, standard HVAC fins, automotive heat exchangers, and thicker industrial fin components. | Check the machine’s verified working range rather than relying only on its maximum rated thickness. |
| Production Speed | A practical specification should state strokes per minute or parts per minute under a defined fin height, pitch, thickness, and tooling condition. | Nominal speed alone does not indicate actual output. Product geometry, press stroke, feed length, and changeover time affect throughput. | High-volume automotive and HVAC production, as well as medium-volume custom heat-exchanger manufacturing. | Ask for a sample-production test and compare stable running speed, reject rate, and actual usable output. |
| Press Capacity | Capacity must be calculated from material strength, thickness, cutting perimeter, forming geometry, and safety margin. | Insufficient capacity can cause incomplete forming, excessive deflection, premature die damage, or machine overload. | Progressive fin stamping, louvered fins, serrated fins, plain fins, and perforated fin designs. | Require a tonnage calculation or test result for the intended product instead of selecting a machine by capacity alone. |
| Feed Accuracy | For precision fin production, buyers should evaluate repeatability in micrometres and confirm the measurement method. | Accurate feeding controls fin pitch, tube-hole position, louver alignment, and compatibility with downstream assembly. | Tube-and-fin heat exchangers, multi-row coils, precision louvers, and automatic core assembly lines. | Review feed-system design, encoder feedback, material straightening, guide alignment, and test-run records. |
| Fin Geometry | Confirm fin height, pitch, louver angle, louver length, collar or tube-hole diameter, and cut-off length. | These dimensions determine heat-transfer performance, air-side pressure drop, tube compatibility, and final core quality. | Plain plate fins, wavy fins, louvered fins, serrated fins, and perforated fins. | Provide approved drawings or samples and verify the die can be adjusted or replaced for future products. |
| Tooling and Die Quality | Use wear-resistant tool steel with controlled clearances, stable guiding, and replaceable wear components. | Tool accuracy affects burrs, fin deformation, dimensional consistency, maintenance frequency, and service life. | Continuous coil production and applications requiring frequent product changes. | Check die-material documentation, heat-treatment records, spare-part availability, adjustment access, and preventive-maintenance instructions. |
| Machine Frame and Vibration | A rigid frame, balanced moving components, proper foundation requirements, and controlled vibration levels are essential. | Excessive vibration can reduce feed accuracy, increase noise, loosen tooling, and shorten the service life of bearings and electrical components. | Continuous high-speed operation and production lines with strict dimensional tolerances. | Request foundation specifications, running-balance information, noise data, and a demonstration at the intended operating speed. |
| Control and Monitoring | Preferred functions include programmable recipes, fault diagnosis, overload protection, feed monitoring, and production counters. | Monitoring reduces setup errors, improves traceability, and helps operators identify material, tooling, or feeding problems quickly. | Multi-product factories, automated lines, and plants requiring repeatable changeovers. | Verify language options, data backup, password levels, alarm history, remote-service provisions, and compatibility with factory automation. |
| Safety Standards | Risk assessment should follow ISO 12100; safety-related control systems may be evaluated against ISO 13849-1 or IEC 62061; electrical equipment should address IEC 60204-1 where applicable. | These standards help address guarding, emergency stops, control reliability, electrical hazards, and foreseeable machine risks. | Factories operating under structured occupational-safety programs or supplying regulated markets. | Request the risk assessment, safety-circuit documentation, guarding details, emergency-stop test results, and applicable conformity documents. |
| Electrical and Pneumatic System | Electrical voltage, frequency, compressed-air pressure, air quality, and connection requirements must match the installation site. | Incorrect utilities can cause unstable operation, component failure, unplanned downtime, or safety issues. | Standalone presses, integrated fin lines, and plants with centralized utility systems. | Confirm utility consumption, required air filtration, electrical protection, cable standards, and installation drawings. |
| Lubrication and Scrap Handling | Evaluate lubrication control, oil recovery, scrap collection, chip evacuation, and access for cleaning. | Proper lubrication supports forming quality and tool life, while effective scrap handling prevents line stoppages and contamination. | High-speed coil stamping, coated aluminum production, and automated lines. | Check lubricant compatibility with the aluminum surface and downstream brazing, coating, or cleaning process. |
| Quality Inspection | Recommended checks include fin pitch, height, thickness, louver geometry, hole position, burr height, flatness, and cut length. | Consistent inspection links machine performance to finished heat-exchanger efficiency and assembly quality. | Automotive thermal systems, HVAC coils, refrigeration equipment, and industrial heat exchangers. | Define inspection frequency, measurement equipment, sample size, acceptance limits, and calibration requirements. |
| Energy and Operating Cost | Compare installed power, average energy consumption, compressed-air use, lubricant consumption, tooling cost, and maintenance intervals. | The purchase price is only one part of the total cost of ownership over the machine’s service life. | High-duty production, multi-shift operation, and facilities with energy-efficiency targets. | Request measured consumption under a defined production condition and include spare parts, tooling, training, and service costs. |
| Service and Spare Parts | Evaluate commissioning support, operator training, preventive-maintenance documentation, spare-parts availability, and response procedures. | Fast technical support reduces downtime and helps preserve feed accuracy and die performance. | Export installations, remote production sites, and plants without specialized press technicians. | Confirm service coverage, recommended critical spares, response time, warranty terms, and technical-document language. |
| Factory Acceptance Test | Use the buyer’s aluminum material, approved drawing, target speed, and agreed inspection plan during the acceptance test. | A documented test provides stronger evidence of real capability than catalogue specifications alone. | New production lines, customized fin profiles, and high-volume contracts. | Record output rate, dimensional results, stoppages, scrap percentage, safety functions, and changeover performance. |
| Best-Fit Selection | Choose the machine that meets the required product range, stable output, safety obligations, service capability, and total operating cost. | The best machine is application-specific; maximum speed or tonnage does not automatically provide the best value. | Small-batch custom work, standard HVAC production, automotive components, and fully automated heat-exchanger lines. | Use a weighted comparison covering technical performance, compliance, reliability, delivery, support, and lifecycle cost. |
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru