The best Profile Wrapping Machine in 2026 depends on the profiles you run, your finish requirements, and the pace your production line can sustain. A machine that handles straight MDF trim well may struggle with narrow edges, complex shapes, or delicate decorative films. The right choice starts with your actual product range, not a headline speed figure.
Management expert Peter Drucker offered a useful reminder: “There is nothing so useless as doing efficiently that which should not be done at all.” Drucker was not a wrapping-machine specialist, but the principle fits this purchase: automation only helps when it suits the work. Test representative profiles with your intended film. Watch how the machine feeds material, applies adhesive, controls temperature, and handles corners. Small wrinkles matter. So does changeover time.
This guide compares the practical details buyers should verify in 2026, including usable working width, feed consistency, operator controls, maintenance access, and supplier support. Ask for a production trial, not just a showroom demonstration. Check whether the wrapped surface stays even along the full profile, especially at edges and joints. Request clear specifications, service terms, and references from comparable operations. No single model is best for every workshop. A careful assessment can reveal the better fit—and sometimes show that a slower, simpler machine is the wiser investment.
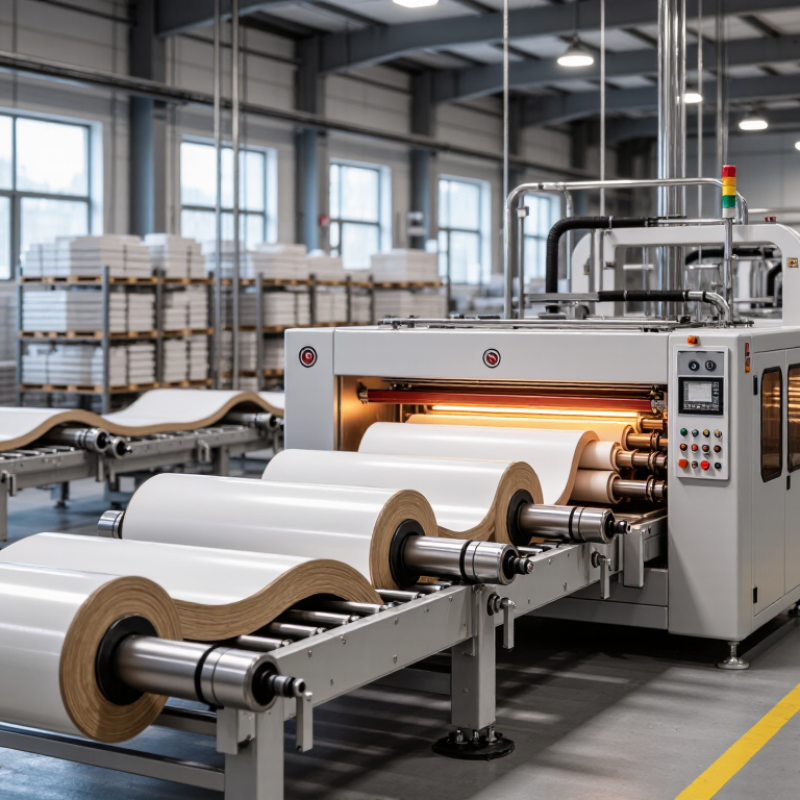
A profile wrapping machine covers long components with decorative film, veneer, or paper. Common workpieces include cabinet trim, door frames, and aluminum sections. The machine typically uses feed rollers to guide each profile through the wrapping line. An adhesive unit applies glue to the surface or covering material, depending on the setup. Then pressure rollers fold and press the covering around the profile. Trimming tools remove excess material at the edges or ends. The finished surface should look even, with no lifted corners or visible bubbles.
The process depends on matching the machine to the profile’s shape and material. A narrow groove, sharp corner, or slight bend can affect how the film sits. Operators adjust roller pressure, feed speed, adhesive amount, and sometimes temperature. Small changes matter. In practice, the first settings may not be right; test pieces help reveal wrinkles or weak bonding before a full production run. Results also depend on clean surfaces and consistent material quality.
Tips: Check the profile dimensions and covering specifications before setup. Run a short sample, then inspect corners and edges closely. Keep rollers clean, and record settings that work. A rushed adjustment can hide the real cause of a defect.
What Is the Best Profile Wrapping Machine in 2026?
Key Machine Types and Their Main Differences
The best machine depends on profile shape, surface material, adhesive, and daily output—not simply its advertised speed. Roller-based machines feed flat or gently curved profiles through pressure rollers, applying decorative film with consistent contact. They suit repeat production and straightforward shapes. For deep grooves, narrow edges, or complex contours, vacuum-assisted systems can draw film into harder-to-reach areas. They offer more shaping flexibility, but setup and cycle times may be longer. Small details matter.
Adhesive choice also separates machine types. Hot-melt systems heat adhesive for rapid bonding and are often chosen for continuous production. PUR systems can provide durable bonds across varied materials, but require careful control of application and cleaning. MarketsandMarkets’ Packaging Machinery Market report projected growth from USD 46.6 billion in 2022 to USD 58.2 billion by 2027. That figure covers packaging machinery broadly, not profile wrappers alone; it signals wider investment in automated production, rather than proving one machine type is superior.
Tips: Bring actual profiles and film samples to a trial. Check edge coverage, glue lines, changeover time, and scrap after startup. Ask operators to test the machine, too. A specification sheet cannot reveal every awkward adjustment. Some shops choose the fastest line, then regret its limited flexibility.
A practical comparison of machine configurations and adhesive systems. The best choice depends on the profile, covering material, production volume, and required bond performance.
| Category | Machine Type or System | What It Handles | Main Advantages | Key Limitations | Best Suited To |
|---|---|---|---|---|---|
| Machine configurations | |||||
| Configuration | Single-side / flat-surface wrapper | Applies a decorative covering to one principal face of a straight profile. The exact number of wrapped faces depends on the roller and guide setup. | Relatively straightforward setup; a practical option for simple profiles and repeat production. | Less suited to profiles with several deep grooves, tight radii, or multiple faces that must be covered in one pass. | Simple trim, mouldings, and other profiles with a consistent cross-section. |
| Configuration | Multi-side profile wrapper | Uses forming rollers and guides to wrap covering material around multiple faces of a profile, often in a continuous pass. | Can cover more complex cross-sections and reduce the need for separate finishing operations. | Setup and adjustment are more demanding; tooling and material must suit the profile geometry. | Profiles requiring coverage on several faces, such as frames, trims, and shaped mouldings. |
| Configuration | Universal or quick-change wrapper | Uses adjustable guides, pressure elements, or changeable tooling to accommodate a range of profile shapes and sizes. | Offers flexibility across product runs and can reduce changeover effort when appropriately configured. | “Universal” does not mean every profile can run without dedicated setup; complex shapes may still need custom tooling. | Manufacturers with varied product lines and frequent profile changeovers. |
| Configuration | Automated wrapping line | Combines a wrapper with equipment such as automatic feeding, conveying, cutting, or downstream handling. | Can reduce manual handling and support more consistent, continuous production. | Requires more floor space, integration planning, and investment than a stand-alone machine. | Higher-volume production with stable product specifications and repeatable workflows. |
| Common adhesive systems — these can be paired with suitable machine configurations | |||||
| Adhesive system | PUR hot melt | Applies reactive polyurethane hot-melt adhesive to bond the covering to compatible profile materials. | Can provide strong bonds and good resistance to heat and moisture when correctly specified and processed. | Requires careful control of application and curing conditions; equipment cleaning and adhesive handling need attention. | Applications where bond durability and environmental resistance are important. |
| Adhesive system | EVA hot melt | Uses thermoplastic ethylene-vinyl acetate hot-melt adhesive for profile covering. | Often offers a practical, straightforward process for compatible materials and standard applications. | Heat and moisture performance may be lower than that of a suitably specified reactive PUR system. | Cost-conscious production where the required service conditions are compatible with the adhesive. |
| Adhesive system | Cold glue | Applies a water-based adhesive, commonly used with compatible porous substrates and covering materials. | Useful for suitable paper-based coverings and substrates; avoids a hot-melt application process. | Drying and setting requirements can affect line speed and handling; suitability depends strongly on the materials. | Jobs using compatible porous materials where the process can accommodate the adhesive’s setting time. |
| Quick selection guide | |||||
| Priority | Recommended starting point | For simple profiles, compare a basic wrapper and adhesive compatibility. For multi-face or shaped profiles, evaluate a multi-side or adjustable machine using the actual profile and covering material. | For frequent product changes or high output, assess changeover tooling and line automation. Confirm adhesive, finish quality, and process settings with production trials before purchase. | ||
When comparing profile wrapping machines in 2026, judge output on your own profiles, not just the advertised speed. Measure finished pieces per hour, then check whether the film stays smooth around corners and narrow edges. Ask how quickly operators can change rolls, adjust tension, and reset the machine for another profile size. Those minutes add up during short production runs. A fast machine is not always the most productive.
Material compatibility matters just as much. Test the films and profiles you actually use, including painted, laminated, or uneven surfaces. Look for consistent adhesion without wrinkles, trapped air, or residue. A small trial run helps. Record setup time, rejected pieces, and film use; results can vary with temperature and operator experience. Operating costs include more than the purchase price: energy, replacement parts, maintenance, training, and downtime all affect the real cost per wrapped metre. Request a clear maintenance schedule and check how easily routine service can be done. One weak point in many comparisons is underestimated changeover time. It is easy to overlook. Keep that in mind when comparing daily output estimates.
Choosing a profile wrapping machine in 2026 means looking beyond its advertised speed. The right choice depends on profile shape, material, film type, and daily production needs. A narrow trim and a wide panel can behave very differently on the same line.
Start with adjustment range and changeover time. Can operators set guides and rollers accurately for different profiles? A clear control screen helps, but practical access matters too. If changing a roller requires awkward tools or repeated trial runs, setup can quietly eat into production time. Small details matter.
Check how steadily the machine controls film tension, feed, and heat. Uneven tension may cause wrinkles around corners; excessive heat can mark sensitive surfaces. Ask for performance data using profiles and wrapping materials similar to yours, not just a straight sample. Test real profiles. Record the results.
Also consider maintenance access, fault messages, and operator training. Sensors are useful when they point to a specific issue, such as a feed interruption, rather than displaying a vague alarm. Request details on routine cleaning, replacement parts, and expected service intervals. These figures vary with materials and workload, so treat them as estimates, not guarantees. A short production trial may reveal more than a polished demonstration, though it will not predict every shift or product variation.
What Is the Best Profile Wrapping Machine in 2026?
How Production Needs Shape the Best Machine Choice
The best profile wrapping machine is the one that fits your actual production mix. A shop running long shifts on one profile needs steady feed, quick roll changes, and reliable tension control. A smaller line switching between wood, metal, and composite profiles may benefit more from fast changeovers and simple adjustments. Check the profile dimensions, film types, adhesive requirements, and target output before comparing machine speeds. A fast machine is not automatically the right machine.
Production scale matters, but so does variation. The International Federation of Robotics reported 4,281,585 industrial robots in operation worldwide in 2023, a 10% rise over 2022, in its World Robotics 2024 report. That figure reflects broader factory automation, not profile wrapping alone. Still, it shows why buyers should consider how a wrapping line will connect with feeding, cutting, and inspection processes. Ask for a trial using your own profiles and film. A tidy specification sheet can miss real setup delays; that part deserves a hard look.
Tips: Track changeover time, film waste, and stoppages during a production trial. Ask operators to test adjustments themselves. Their feedback may reveal practical issues that a purchase checklist overlooks.
How production needs shape the best machine choice
The best choice depends on throughput, product variety, and changeover needs. These qualitative 1–5 fit ratings are an illustrative planning guide, not measured performance data or a universal ranking. Confirm actual line speed, profile dimensions, materials, and tooling requirements with machine specifications and production trials.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru