Cast Iron Castings are made by pouring molten iron into a shaped mold, then cooling it into a component. The process sounds simple. The engineering is not. Carbon content, cooling rate, mold design, and heat treatment all influence the finished part. Those choices affect strength, wear resistance, vibration damping, machinability, and cost.
The American Foundry Society’s industry facts report more than $50 billion in annual U.S. metalcasting shipments. That figure covers cast metals broadly, not cast iron alone, but it shows the scale of the manufacturing sector. The World Foundry Organization’s Census of World Casting Production tracks output by country and material, giving buyers and engineers a useful view of foundry production trends. Scale matters. Yet tonnage cannot tell you which grade belongs in a pump housing, brake drum, or machine base.
John Campbell, a leading foundry metallurgist and author of Castings, has emphasized, “The quality of a casting is determined by the quality of the liquid metal.” That principle helps explain why material selection and foundry process control must be considered together. Gray iron often suits parts that need damping and easy machining. Ductile iron can offer higher strength and toughness. White, malleable, and compacted graphite irons serve more specialized needs. There is no universal winner. A grade chosen from a datasheet alone can still disappoint in service. This guide compares the main types, their properties, and their trade-offs, so the best choice can be tied to the part’s actual loads, environment, and production requirements.
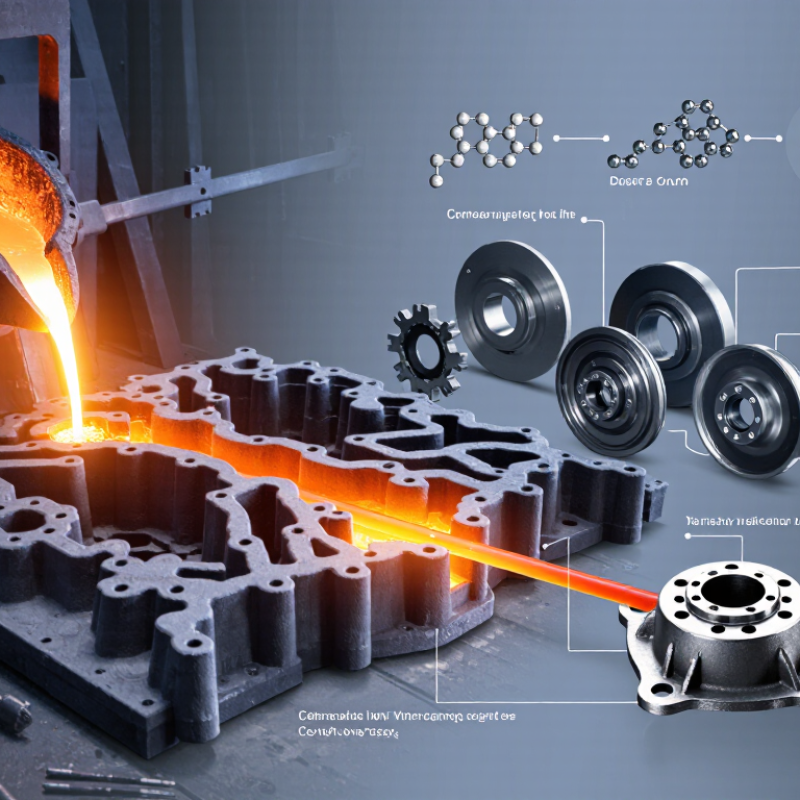
Cast iron castings are components formed by pouring molten iron into a shaped mold and allowing it to cool. The alloy typically contains more than 2% carbon, along with silicon and other elements that affect its behavior. As the metal solidifies, carbon can form graphite flakes or nodules, depending on the alloy and cooling conditions. These structures influence strength, wear resistance, vibration damping, and machinability. Details matter. A rough casting may be perfectly usable after machining, while a smooth surface alone does not prove the part is sound.
Production often starts with a pattern that creates the desired cavity in a mold. In sand casting, workers pack prepared sand around the pattern, then remove the pattern to leave the shape behind. The mold also needs channels that guide metal in and allow gases to escape. Iron is melted in a furnace, adjusted to the required composition, and poured into the prepared mold. Temperature and pouring speed matter; small variations can affect filling and solidification. After cooling, the mold is broken away, and excess metal is cut off. The casting may then be cleaned, machined, and inspected for dimensions or surface defects. Inspection methods depend on the part’s intended use, and some internal flaws are not visible by eye. The process is controllable, but never perfectly uniform.
Cast iron castings are components made by pouring molten iron-carbon alloy into a mold and allowing it to solidify. Cast irons generally contain more than 2% carbon; their properties depend on carbon form, alloying elements, cooling rate, and heat treatment.
| Cast Iron Type | Typical Structure | Typical Mechanical Characteristics | Main Advantages | Common Applications | Best Choice When... |
|---|---|---|---|---|---|
| Gray iron | Carbon is mainly present as graphite flakes in a pearlitic or ferritic metal matrix. | Common grades have tensile strengths of roughly 150–400 MPa; elongation is usually low, often below 1%. | Good vibration damping, machinability, castability, and thermal conductivity. | Machine bases, engine blocks, brake components, pipes, and pump housings. | Vibration damping, machinability, and economical production matter more than tensile strength or ductility. |
| Ductile iron (nodular or spheroidal graphite iron) | Graphite forms rounded nodules rather than flakes; the matrix may be ferritic, pearlitic, or mixed. | Common grades range from about 350 MPa to over 800 MPa in tensile strength, with elongation varying widely by grade. | Higher strength and ductility than gray iron; good fatigue and impact performance in suitable grades. | Pressure pipes, automotive parts, gears, crankshafts, and load-bearing components. | A casting must withstand substantial mechanical loads while retaining useful ductility. |
| White iron | Most carbon is combined as cementite or other carbides rather than forming free graphite. | Very hard and wear-resistant, but generally brittle; properties vary substantially with alloy and heat treatment. | Strong resistance to abrasion and sliding wear. | Wear plates, mill liners, rolls, and components exposed to abrasive materials. | Abrasion resistance is the primary requirement and impact loading is limited. |
| Malleable iron | Produced by heat-treating white iron so that carbon forms temper-carbon clusters. | Strength and elongation depend on grade; it is generally more ductile than white iron. | Useful combination of strength, toughness, and machinability for smaller castings. | Pipe fittings, brackets, clamps, and hardware components. | A relatively small casting needs better toughness than white iron can provide. |
| Compacted graphite iron (CGI) | Graphite forms short, interconnected vermicular shapes between flake and nodular forms. | Typically stronger and stiffer than gray iron, with lower ductility than many ductile iron grades. | Combines useful strength, thermal performance, and vibration damping. | Diesel engine blocks, cylinder heads, and other thermally and mechanically loaded components. | A component needs a balance of strength, stiffness, and thermal performance. |
Mechanical-property figures are indicative ranges, not design values. Actual results depend on the specified grade, section thickness, casting quality, and applicable standard.
| Stage | What Happens | Why It Matters |
|---|---|---|
| 1. Prepare the alloy | Pig iron, scrap, and other charge materials are melted. The melt’s chemistry is adjusted, and treatment additions may be used where required. | Carbon, silicon, and other elements influence graphite formation and the final properties. |
| 2. Make the mold and core | A mold is formed around a pattern; sand or other core materials create internal passages and cavities. | Mold design controls the casting’s shape, dimensions, feeding, and solidification. |
| 3. Pour the molten iron | Molten iron is poured into the mold through a gating system. | Controlled pouring helps fill the cavity and limits defects such as incomplete filling and trapped inclusions. |
| 4. Solidify and cool | The iron cools in the mold; its cooling rate and section thickness affect the resulting structure. | Solidification conditions influence graphite shape, matrix structure, hardness, and strength. |
| 5. Remove and finish | The casting is removed from the mold, cleaned, and may be heat-treated or machined. Inspection checks dimensions and quality. | Finishing and inspection help the component meet its intended specifications. |
Cast iron is not a single material with one fixed set of properties. Its carbon content, silicon level, and cooling history influence the structure that forms inside a casting. Carbon typically appears as graphite or as iron carbide, and that difference changes how the part behaves. Small differences matter. A foundry adjusts chemistry and cooling conditions to suit the casting’s shape and intended service.
In gray iron, graphite forms flakes that help damp vibration and conduct heat, but can make the material less resistant to impact. Ductile iron contains rounded graphite nodules, which generally improve strength and toughness. White iron forms hard iron carbides and resists abrasion, though it is difficult to machine and can be brittle. These trade-offs are easy to underestimate.
Cooling is not uniform across a thick casting. Thin edges lose heat quickly, while a heavy center cools more slowly; this can produce different structures in one part. Chills or controlled mold conditions can help manage the difference, but results depend on section size and chemistry. “Best” therefore depends on the job: a pump housing may favor vibration damping, while an abrasive liner may need wear resistance. Check the specified grade and test data for the actual casting, not just a general type name.
Gray iron contains graphite flakes that help damp vibration and conduct heat. It suits machine bases, brake discs, and engine blocks.
Ductile iron has rounded graphite nodules, which improve strength and toughness. It is common in pipes, gear housings, and suspension parts. ASTM A48 and ASTM A536 specify common gray- and ductile-iron grades.
White iron is hard and wear-resistant, but it can be brittle. It is used for liners and parts exposed to sliding abrasion.
Malleable iron offers better impact resistance than ordinary gray iron, making it useful for small brackets and fittings.
Compacted graphite iron sits between gray and ductile iron in several properties; engine components are a typical application.
The World Foundry Organization’s 2022 census estimated global casting production at 109.5 million tonnes. That figure shows the industry’s scale, not which grade suits a particular part. The boundary is not always neat.
Tip: Match the grade to the load, wear, vibration, and operating temperature. Ask the foundry for test data on the proposed grade and section thickness. A catalog value alone may not reflect a thick or thin casting.
Choosing a cast iron type starts with the component’s actual job. A machine base that must damp vibration has different needs from a pipe fitting exposed to bending loads. Gray iron machines well and absorbs vibration, but its graphite flakes make it less tolerant of tension and impact. Useful for housings and beds. Not every housing faces the same loads.
Ductile iron’s rounded graphite nodules improve strength and toughness, making it a candidate for gears, brackets, and pressure-bearing parts. Malleable iron can suit smaller fittings that need some flexibility, while white iron offers high wear resistance but is hard and brittle.
These descriptions are starting points, not guarantees. Check the expected load, temperature, wear, section thickness, and machining needs against test data for the actual grade and casting. A thick section may cool differently from a thin one, changing local properties.
I would also ask how the part fails if the design assumption is wrong. That question can expose a mismatch before production.
Cost matters, too, but choosing by price alone can be expensive later.
Choose cast iron by the load, impact, vibration, and shape your part must handle. Gray iron suits machine bases, housings, and brake components where vibration damping and easy machining matter. ASTM A48/A48M Class 30 specifies a minimum tensile strength of 30,000 psi for its test bars. That figure is useful, but it does not mean every casting performs identically; wall thickness and casting quality affect results.
For parts facing shock or bending, consider ductile iron. ASTM A536 Grade 60-40-18 lists 60,000 psi tensile strength, 40,000 psi yield strength, and 18% elongation. Those values offer a useful comparison with gray iron’s lower ductility. Still, a stronger grade may add cost or complicate machining. Ask the foundry for test data from a representative section, not just a grade label.
Malleable iron can suit smaller fittings and brackets that need some toughness. White iron offers high wear resistance, but its hardness can make machining difficult. Check operating temperature, corrosion exposure, section thickness, and the finish required. A thin rib beside a thick boss may cool differently and develop uneven properties. There is no perfect grade. I would verify the actual loading and casting process before choosing from a datasheet alone.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru