Choosing the right Hjt Wet Carrier can affect wafer handling, process stability, and production yield in heterojunction solar cell manufacturing. HJT wafers are thin and sensitive to scratches, particles, and surface contamination. A carrier must hold each wafer securely while allowing process liquids to reach the required surfaces. It should also support smooth drainage, rinsing, and drying. Small design details matter.
Start by checking wafer dimensions, thickness, and the layout of your wet-process equipment. Then review the carrier material for chemical compatibility, thermal limits, and particle control. Confirm that its slots provide enough support without pressing unevenly on the wafer edges. Too much contact can create damage. Too little can allow movement. Neither is ideal. Consider how quickly operators can load and unload wafers, and whether the carrier fits existing automation and cleaning routines.
Specifications alone are not enough. Ask suppliers for material data, cleaning guidance, and evidence from relevant production conditions. Where possible, run a controlled trial and inspect wafers for marks, residue, breakage, and handling consistency. Track results across repeated cycles, not just one successful run. There is no single carrier design that suits every HJT line; chemistry, equipment, wafer format, and throughput all influence the choice. Even a careful evaluation may miss a practical issue. A carrier that performs well in a test may behave differently during routine production, so feedback from operators should remain part of the decision.
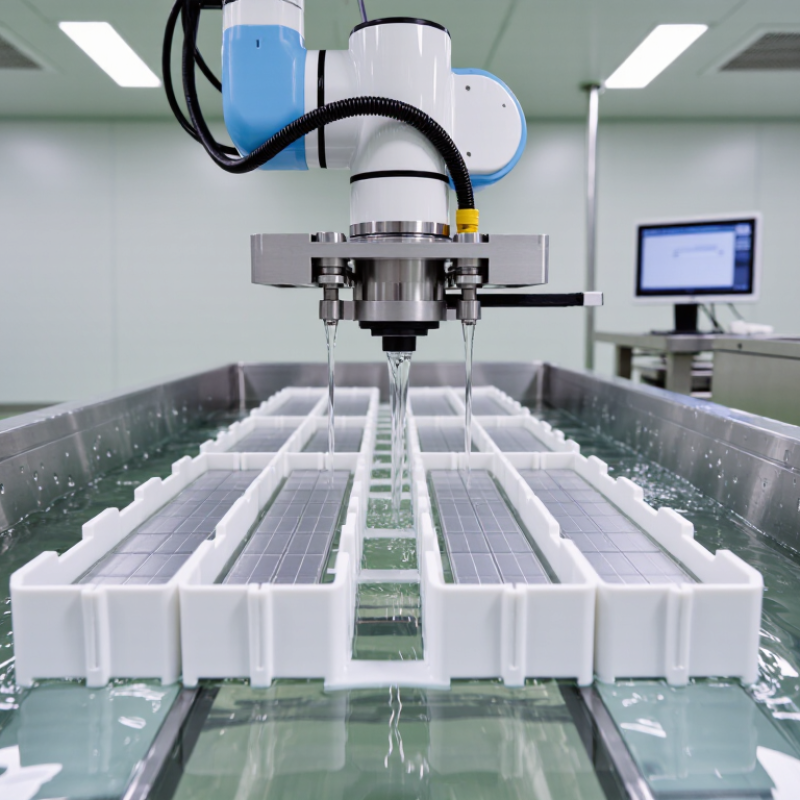
In HJT cell production, a wet carrier does more than hold wafers. It keeps fragile silicon substrates positioned as they pass through cleaning, texturing, and other wet-process stages. Stable support helps limit wafer movement, edge contact, and breakage. It also allows process liquids to reach the surfaces consistently, which matters when small differences in residue or treatment can affect later cell performance.
Choosing a carrier means matching its material and design to the actual process. Check chemical compatibility, temperature limits, drainage, and how securely wafers sit in their slots. Narrow or poorly finished contact points may leave marks or trap liquid. A carrier that is difficult to rinse can also carry residues between baths. Small details matter. In production, operators should inspect carriers for wear and verify that cleaning removes visible deposits. Testing a sample carrier under real process conditions is more reliable than relying on a specification sheet alone.
It is tempting to treat carriers as simple fixtures. That view can miss their influence on handling consistency and contamination control. Still, a better carrier cannot compensate for unstable bath conditions or careless loading. Selection deserves review alongside the wet-process recipe, wafer dimensions, and maintenance routine. Some trade-offs remain; denser support may improve stability but restrict liquid flow. Teams should document breakage, residue, and handling issues, then adjust the design based on observed results.
HJT wet carriers must match the actual process, not just the cell dimensions. Map each bath, rinse, and transfer step before specifying a carrier. Note chemical exposure, temperature, dwell time, and whether wafers enter face-up or edge-supported.
The 15th International Technology Roadmap for Photovoltaic (ITRPV, 2024) tracks silicon wafer thickness moving toward roughly 130 micrometres across mainstream cell technologies. That is a useful design reference, not a universal HJT specification.
Thin wafers flex easily. Small support gaps can become breakage points.
Check the carrier’s contact geometry against the wafer and the wet-process flow. Open drainage paths help reduce liquid carryover between baths, while smooth, cleanable surfaces limit residue around contact points.
Confirm chemical compatibility with the actual bath concentrations and operating temperatures; generic material labels are not enough.
Ask operators to test loading and unloading with wet gloves, since slippery edges can make a sound design awkward in practice. Measure wafer breakage, particle counts, and carryover during a representative production trial. Keep the results by process step.
I still treat carrier selection as a trial, not a catalog decision. Small handling issues can hide until the line runs at speed.
Choosing an HJT wet carrier is a materials decision and a geometry decision. Its surface must support thin wafers without trapping rinse water or creating pressure points. Quartz offers high chemical stability, while engineered polymers can reduce weight and impact damage. Compatibility depends on the actual bath chemistry, temperature, and cleaning cycle—not a supplier’s generic resistance chart. Check slot width, edge support, drainage paths, and robot-grip clearance against the production wafer. Small mismatches matter.
The Fraunhofer ISE Photovoltaics Report documents research heterojunction cell efficiencies above 26%, illustrating how sensitive advanced cell processes are to material quality. That figure is not a carrier-performance guarantee. It does, however, underline why particles, scratches, and uneven drying deserve close attention. Run carriers through repeated wet-dry cycles, then inspect contact areas under magnification. Measure wafer breakage and residue rates across real shifts, not just a short trial. A carrier that looks clean may still hold droplets in recessed corners. Easy to miss. The ITRPV roadmap also tracks ongoing reductions in wafer thickness, so designs should accommodate fragile substrates and future format changes. Honestly, no carrier choice is perfect; maintenance habits and handling variability can undermine a good design. Use trial data, and record the awkward failures too.
Comparing typical coefficients of thermal expansion (CTE) helps assess dimensional mismatch between carrier materials and silicon wafers.
Typical approximate CTE values near room temperature (µm/m·°C); actual values vary with grade and test conditions. A closer CTE match can reduce differential expansion, but chemical resistance, wafer support, particle control, and process-specific compatibility must also be evaluated.
For HJT production, carrier cleanliness is not cosmetic. Fine particles, dried chemistry, or residue around a slot can mark delicate wafer surfaces and disrupt repeatable handling. Fraunhofer ISE’s Photovoltaics Report (2024) records a 26.1% laboratory efficiency for silicon heterojunction cells. That benchmark is not a carrier test, but it shows why small process variations deserve attention. Inspect contact surfaces under bright, angled light; a faint film can be easy to miss.
Durability and chemical resistance matter together. A carrier may look sound yet swell, become brittle, or shed particles after repeated exposure to alkaline cleaners, acids, or hot rinses. Check the supplier’s compatibility data against the actual concentration, temperature, and exposure time in your line. Then run a controlled soak-and-cycle trial, recording mass, dimensions, surface condition, and particle counts before and after. The ITRPV 2024 roadmap documents continued industry pressure to reduce silicon wafer thickness; thinner wafers make stable support especially important. A carrier’s service life should be measured in real production cycles, not assumed from appearance.
Tips: Set a baseline with clean carriers, filtered rinse water, and particle checks. Track edge chips and residue by carrier position. If results vary, inspect the cleaning method too; the carrier may not be the only cause. A little inconvenient, but worth testing.
| Carrier Material | Cleanliness Potential | Mechanical Durability | Chemical Resistance | Typical Strengths | Points to Check Before Selection |
|---|---|---|---|---|---|
| Polypropylene (PP) | Good when made and cleaned for high-purity wet processing; cleanliness depends on resin, fabrication, and handling. | Good | Generally good with many aqueous acids and alkalis at moderate temperatures; compatibility can be limited by strong oxidizers and some solvents. | Lightweight, widely used, and economical for many wet-process applications. | Check temperature limits, chemical concentration, carrier loading, and particle or extractables performance over repeated cycles. |
| Polyvinylidene fluoride (PVDF) | Very good when high-purity grades and suitable fabrication practices are used. | Very good | Broad resistance to many acids and halogens; suitability varies with chemical, concentration, temperature, and exposure time. | A useful balance of chemical resistance, stiffness, and service life in demanding wet environments. | Verify compatibility with the exact bath recipe and confirm that molded or machined parts meet cleanliness requirements. |
| Perfluoroalkoxy polymer (PFA) | Excellent potential | Good | Excellent resistance to a wide range of aggressive process chemicals; verify conditions for the specific application. | High chemical inertness and low contamination potential make it suitable for stringent purity requirements. | Typically higher in material and fabrication cost; assess stiffness, design support, and handling requirements. |
| Polyether ether ketone (PEEK) | Good to very good, depending on grade, manufacturing, and cleaning validation. | Excellent | Resists many chemicals, but strong oxidizing agents and some process conditions require careful compatibility review. | High stiffness and wear resistance can support robust carrier features and repeated handling. | Confirm extractables and particle performance, as well as compatibility with every chemical and temperature in the process. |
| Fused silica / quartz | Excellent potential | High hardness, but brittle and susceptible to chipping or breakage under impact. | Resists many acids, but hydrofluoric acid and fluoride-containing chemistries attack silica-based materials. | High-purity inorganic material with good thermal stability. | Assess breakage risk, edge protection, handling method, and whether any process step uses HF or fluoride chemistry. |
| Selection priority for HJT wet processing | Specify particle, ionic contamination, and extractables requirements for the actual process. | Consider wafer support, transfer loads, clamping, and expected replacement interval. | Validate against the full chemical sequence, including concentration, temperature, dwell time, and rinsing. | Match the material to the carrier design, wafer format, and wet-bench operating conditions. | Run a process-specific compatibility and cleanliness qualification before production release. |
| Note: Ratings are general material-level comparisons, not guarantees for a particular carrier. Actual performance depends on material grade, fabrication quality, surface finish, chemical concentration, temperature, exposure time, and cleaning practice. Confirm compatibility and contamination performance with the carrier supplier and process qualification data. | |||||
A wet carrier can pass a cleanroom inspection and still fail beside a running line. Test it with actual HJT wafers, process chemistry, rinse water, and transfer speeds. Watch for wafer slip, edge chipping, residue, and uneven drainage. Small defects matter. IEA PVPS reported 456 GW of new photovoltaic capacity installed worldwide in 2023, underscoring the pressure to maintain throughput without sacrificing handling quality. Scale changes the test: a carrier that behaves well for one shift may drift after repeated chemical exposure.
Record results across multiple production runs, not just a supplier demonstration. Track breakage per thousand wafers, loading time, wetting consistency, and carrier deformation. Compare measurements before and after cleaning cycles. The International Technology Roadmap for Photovoltaic (ITRPV) tracks continuing changes in wafer formats and manufacturing processes; carrier trials should therefore use the dimensions and process window planned for the line. Keep the trial conditions reproducible. A simple log of bath temperature, dwell time, and wafer position can reveal patterns that visual checks miss. Some variation is stubborn. It may come from the carrier, or from upstream handling; separating the two takes honest retesting.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru