How to Choose Hot Dip Galvanized Steel Coil?
Choosing the right Hot Dip Galvanized Steel Coil begins with evidence, not appearance. Global crude steel production reached approximately 1.89 billion tonnes in 2023, according to World Steel Association data. This scale makes coil selection more complex, especially when suppliers offer similar surfaces, gauges, and zinc coatings. A bright finish is useful, but it does not prove long service life.
Dr. Gregory Zhang, a recognized researcher in hot-dip galvanizing technology, has explained: “The zinc coating is metallurgically bonded to the steel, so it protects even when the surface is scratched.” This principle matters on construction sites, where coils may face cutting, forming, transport marks, and humid storage. ASTM A653/A653M and EN 10346 provide essential reference points for coating mass, steel grade, tolerances, and forming performance. Buyers should compare these requirements directly with the final application.
Start with the environment. Coastal air, industrial moisture, and indoor dryness create different corrosion risks. Then check the substrate grade, yield strength, coating designation, coil width, thickness tolerance, and surface treatment. The U.S. Geological Survey’s Mineral Commodity Summaries also shows zinc remains a major industrial material, but availability does not guarantee consistent coating quality.
Ask for mill certificates, coating test results, and traceability records. Inspect the coil edge. Feel the surface carefully. Small details matter.
A low price can hide higher processing costs. I may be overcautious here, but choosing only by zinc weight is incomplete. A reliable decision connects technical standards, supplier experience, field conditions, and the actual forming process. That's where confidence starts.
What Is a Hot Dip Galvanized Steel Coil?
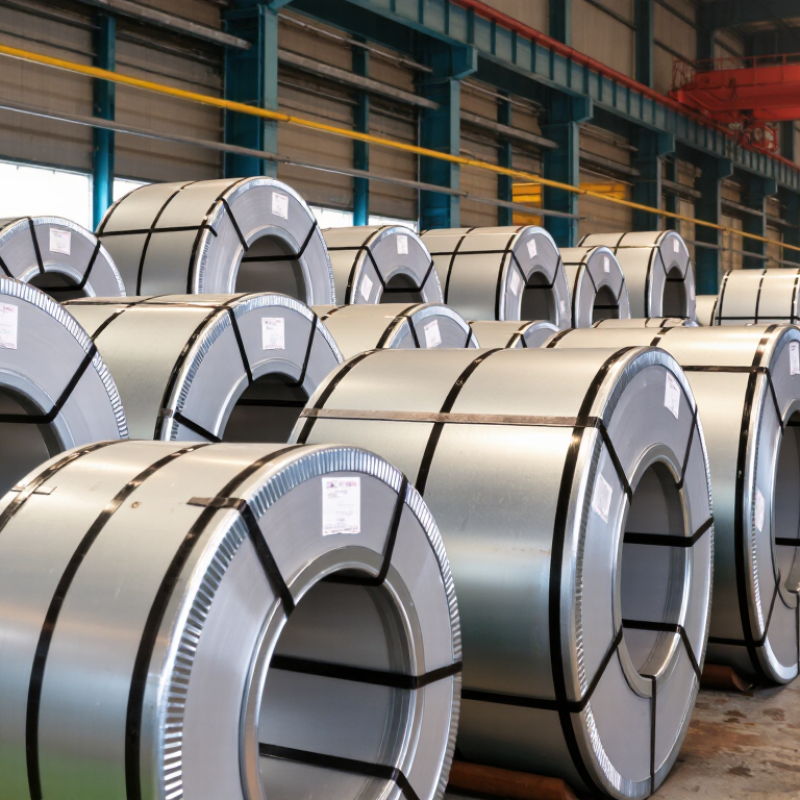
A hot dip galvanized steel coil is a rolled steel strip protected with a zinc coating. Manufacturers clean the steel, pass it through molten zinc, and cool the coated strip under controlled conditions. The zinc bonds to the surface and creates a barrier against moisture, oxygen, and salt. It also offers sacrificial protection. If the surface is scratched, zinc can corrode before the exposed steel does. The coil is then recoiled for transport, slitting, or forming. Its appearance may show a visible spangle, a fine crystal pattern created during solidification. Not every coil looks identical. Surface finish depends on zinc chemistry, cooling, and production control.
When choosing one, check the base steel grade, coating mass, width, thickness, and surface condition. A thicker zinc layer usually improves durability, but it may affect welding, bending, and cost. Ask for test certificates and inspect edges, oil marks, bare spots, dents, and uneven coating. Experienced buyers also consider the final environment. Indoor framing needs differ from coastal panels or agricultural buildings. A specification that sounds strong may still be unsuitable. That is worth checking.
Tips: Match coating mass to exposure, not habit. Confirm dimensions at several points, because coils can vary slightly. Store the material dry, raised from the floor, and protected from trapped water. Use clean gloves during handling. Fingerprints are small, but they can become visible stains. If forming is required, confirm ductility and coating adhesion before ordering. A small trial bend may reveal problems earlier than a large production run.
Which Galvanized Coating Grade Fits Your Application?
Choosing hot dip galvanized steel coil starts with the coating grade, not appearance alone. The grade indicates the zinc mass on both surfaces, commonly shown as Z100, Z275, or Z350 in g/m². Higher numbers usually provide stronger corrosion protection. However, they may affect forming behavior, welding settings, and material cost.
Match the grade to the working environment. Z100 can suit dry indoor panels with limited moisture. Z275 is a practical choice for general construction, ducts, frames, and sheltered outdoor components. Coastal air, road salt, or frequent condensation may require Z350 or a higher grade. Paint systems can add protection, but the coating surface must be prepared correctly.
Do not choose by number alone. Check cut edges, bends, storage conditions, and expected service life. A thicker coating does not repair poor drainage or trapped water. In production, I would inspect sample coils for coating uniformity and measure both sides before approval. Small scratches matter around formed edges. A common mistake is treating Z275 as universally suitable. It is not. Standards and test methods also vary, so confirm the designation with the supplier’s certificate and your project specification. Rechecking the environment may reveal that a moderate grade is enough, or that the original choice was too optimistic.
How to Compare Suppliers, Certifications, and Production Standards
Choosing hot dip galvanized steel coil requires more than comparing price per tonne. The World Steel Association’s World Steel in Figures 2024 reports 1.892 billion tonnes of crude steel production in 2023. That scale makes supplier screening essential, because capacity does not guarantee consistent coating quality. Request recent mill certificates, production locations, batch numbers, and independent test records. Verify ISO 9001 certification directly with the issuing body. Check its scope and expiry date.
Compare standards carefully. ASTM A653/A653M, EN 10346, and JIS G3302 define different requirements for steel grades, dimensions, coating mass, and testing. A supplier should state the exact standard, coating designation, and minimum coating mass in writing. Do not accept “heavy zinc coating” as a specification. Ask for coating thickness or mass results, tensile properties, elongation, surface condition, flatness, and dimensional tolerances. Salt spray results can help, but they should not replace coating-mass verification.
Inspect the coil edge and surface during sampling. Look for bare spots, sharp burrs, excessive spangle variation, wet storage stains, and telescoping. I once treated a lower quotation as efficient; the later slitting loss changed that calculation. Price is incomplete. Compare yield strength consistency, packaging strength, delivery records, claim handling, and traceability. A supplier with strong documentation may still have occasional failures. That is why a trial order, retained samples, and third-party inspection remain practical safeguards.
How to Inspect, Store, and Maintain Galvanized Steel Coils
Choosing a hot dip galvanized steel coil starts with the coating, not only the price. Check the zinc grade, coating mass, steel grade, width, thickness, and tolerances. Ask for mill test certificates and inspect the coil edge for cracks, telescoping, or uneven winding. Under bright, angled light, look for bare spots, heavy zinc buildup, stains, and white rust. Measure thickness at several points with a calibrated gauge. One reading is not enough. I once trusted a clean surface and missed damage hidden beneath the wrapping. That mistake delayed fabrication.
Store coils indoors, on level supports, with separators that prevent metal-to-metal contact. Keep them away from concrete dust, salt, acids, and wet timber. Condensation is a quiet threat. Allow air movement around each coil, but avoid drafts carrying moisture. If outdoor storage is unavoidable, use a sloped waterproof cover and leave ventilation gaps. Do not seal damp coils under plastic. Trapped water can cause white corrosion between coil laps. Check the wrapping after rain, temperature changes, and forklift movement. Storage records should note dates, locations, and visible damage. Small notes help, though they cannot replace inspection.
During handling, use padded slings and clean lifting equipment. Never drag coils across the floor. Remove loose dirt with a soft brush and dry cloth. Avoid abrasive tools that expose steel. For white rust, assess its depth before cleaning or repainting. Light deposits may be treated carefully, but severe coating loss needs technical review. Recheck stored coils regularly. Conditions change. My inspection routine still needs improvement when humidity rises overnight.
How to Choose Hot Dip Galvanized Steel Coil?
Inspection, storage, and maintenance guidance based on common galvanized coating designations.
How to read the chart: ASTM A653 coating designations indicate the approximate total zinc coating mass on both sides of the sheet. The values shown are converted from the designation values of 0.30, 0.60, and 0.90 oz/ft² using 1 oz/ft² ≈ 305.15 g/m².
- Inspect: Confirm the coating designation, surface uniformity, edge condition, dimensions, and visible defects. Use a calibrated magnetic or electromagnetic coating-thickness gauge when verification is required.
- Store: Keep coils indoors or under a dry, ventilated shelter. Prevent contact with standing water, condensation, soil, and corrosive chemicals.
- Maintain: Keep protective packaging intact until use, separate coils from the floor, and remove moisture promptly to reduce the risk of wet storage stain.
Coating requirements should always be checked against the applicable purchase specification and product standard.