Choosing the right Htpb Sealant starts with the conditions it must face, not just a product name. Will the joint move as temperatures change? Is the surface concrete, metal, or a coated material? These details affect adhesion, flexibility, and service life. A sealant that performs well on one substrate may fail on another.
Review the manufacturer’s technical data sheet for application temperature, cure time, movement capability, and chemical resistance. Check whether the product needs a primer, and confirm that the primer suits the actual surface. Details matter. For a critical joint, a small adhesion test can reveal problems before a full application. Clean, dry surfaces and careful mixing, where required, also make a real difference. Even so, site conditions can be less tidy than a test panel.
Consider exposure to sunlight, moisture, fuels, or process chemicals, and compare those conditions with documented product limits. Do not assume all HTPB formulations behave alike. Ask the supplier for current compatibility and performance information when the project involves unusual substrates or severe exposure. Not always. A datasheet may not answer every practical question, so record the conditions and clarify uncertainties before installation. This guide explains the key selection factors, common trade-offs, and checks that help match a sealant to the project. The aim is not to find a universal product, but to make a defensible choice based on the joint, the environment, and verified product data.
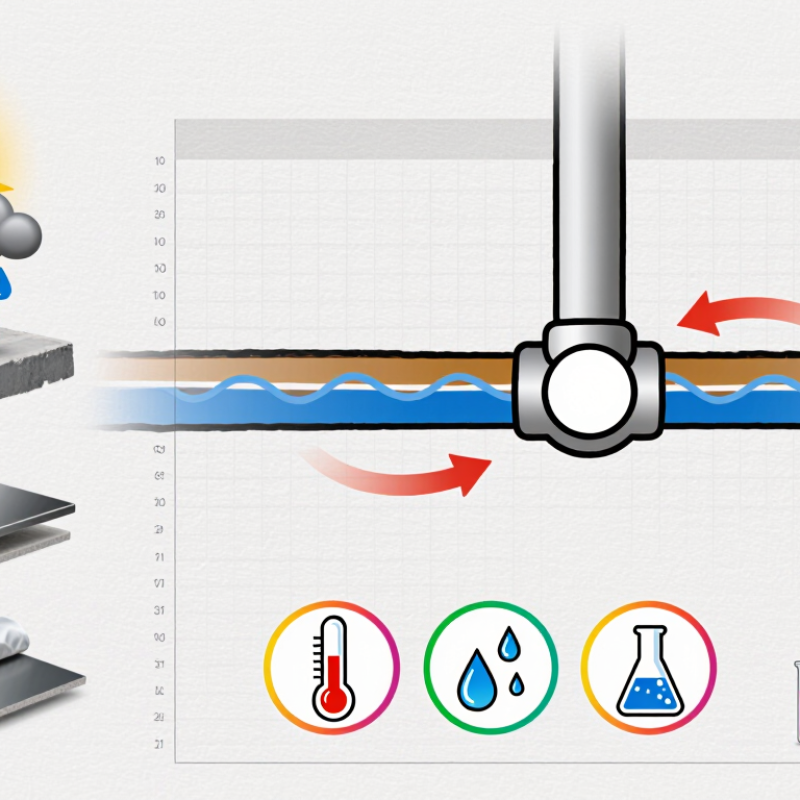
HTPB (hydroxyl-terminated polybutadiene) sealants typically cure into flexible polyurethane networks. Their low-temperature flexibility, elastic recovery, and water resistance depend on formulation and cure conditions. The polymer name alone tells you little. Request cured-product data and test reports, not just resin specifications.
Professional test reports help compare key properties. ASTM D412 measures tensile strength and elongation; ASTM D2240 measures hardness; ASTM C719 evaluates adhesion and cohesion during cyclic joint movement. These are test methods, not performance guarantees. Compare results only when sample preparation, cure time, and test temperature match your project. A Shore A reading cannot predict outdoor durability by itself. The joint matters.
Tips: Match movement capability to the actual joint width and temperature swing. Test adhesion on the real substrate, such as dusty concrete or primed metal. Review immersion, UV, and service-temperature data when relevant. One awkward truth: site moisture and mixing errors can outweigh polished laboratory results. Trial a small bead and record cure time, tack, and any failures before scaling up.
Before choosing an HTPB sealant, define what the joint must withstand. Record the expected temperature range, moisture exposure, movement, and contact with oils, fuels, or cleaning agents. Be specific. A seam on a sun-heated roof faces different demands from a sheltered equipment enclosure. Note whether the joint stays still or flexes repeatedly during operation.
Identify every surface the sealant must bond to, such as concrete, metal, or a coated panel. Check the product’s technical data for substrate compatibility, movement capability, application temperature, and cure time. Verify adhesion on representative samples when practical; surfaces that look clean may still carry oxidation, dust, or release agents. Joint width and depth matter, too. A narrow bead may not accommodate the movement you expect.
Set priorities before comparing products. Is long-term flexibility more important than a fast return to service? How much downtime can the project tolerate? It is easy to focus on a single impressive property and overlook installation conditions. That happens. Record the actual site temperature and whether the joint can remain dry during curing. Include those details when requesting technical guidance, and keep the acceptance criteria clear enough for an installer to check on site.
How to Choose the Right HTPB Sealant for Your Project
HTPB sealants differ in hydroxyl content, viscosity, filler loading, and crosslinker choice. These differences affect flexibility, adhesion, and working time. HTPB’s hydroxyl groups react with isocyanates to form a polyurethane network, but cure speed depends on formulation and site conditions. Check the technical data for mix ratio, usable life, and full-cure time. Small test batches help reveal problems before a long joint is filled.
Curing method matters. Two-part systems offer controlled chemistry but need accurate measuring and thorough mixing. One-part products may simplify application, yet their cure can depend more heavily on temperature and moisture. For field work, consider whether a cartridge gun, static mixer, or bulk dispensing setup can place an even bead. A cold concrete edge can slow cure. It happens. ASTM C920 movement classes, including 25% and 50%, can help frame joint-movement needs; however, do not assume an HTPB product meets that standard without documented testing.
Market figures provide context, not a design rule. Grand View Research estimated the global sealants market at USD 12.9 billion in 2023, with projected annual growth of 4.8% from 2024 to 2030. For project selection, prioritize application-specific test data: adhesion on the actual substrate, cure through the bead, and performance after temperature cycling. One detail is easy to miss: a neat finish does not prove a sound bond. Sealant depth, surface preparation, and mixing consistency deserve equal attention.
| Formulation approach | Typical curing system | Useful characteristics | Key considerations | Suitable application method | Best fit |
|---|---|---|---|---|---|
| Unfilled or lightly filled, two-component HTPB polyurethane | Hydroxyl-functional HTPB reacts with a polyisocyanate curing agent. The two parts are mixed before application; cure is based primarily on the formulation’s NCO-to-OH balance. | Can provide a flexible elastomer with low-temperature flexibility. With little filler, it can be easier to spread or cast than a heavily filled compound. | Mixing ratio, mixing quality, temperature, and batch size affect working time and cure. Confirm adhesion and compatibility with the actual substrate. Avoid assuming that all HTPB grades or curing agents are interchangeable. | Metered two-part dispensing, hand mixing for small batches, or pouring into a prepared joint or cavity. Tool promptly within the verified working time. | Projects needing a flexible, custom-formulated sealant and where two-part mixing and controlled application are practical. |
| Mineral-filled, two-component HTPB polyurethane | The same hydroxyl–isocyanate reaction as other two-component HTPB systems; mineral fillers are incorporated to modify handling and cured properties. | Fillers can increase viscosity and alter hardness, sag resistance, density, and cost. A suitable grade may hold its shape better in a gap or vertical joint than a less-structured compound. | Filler type and loading affect flow, flexibility, and mixing. Check for settling, air entrapment, and adequate wetting of the substrate. Performance must be verified for the specific formulation. | Cartridge or plural-component dispensing if the rheology permits; otherwise use a spatula, trowel, or controlled pour. Use equipment capable of handling the compound’s viscosity. | Applications where a more structured, less-flowing compound is needed, subject to project-specific adhesion and movement requirements. |
| Moisture-curing, one-component HTPB-based polyurethane prepolymer | An isocyanate-terminated prepolymer reacts with moisture. Water participates in reactions that form urea linkages and release carbon dioxide; cure generally progresses inward from exposed surfaces. | Ready to use without mixing a separate curing component. Moisture-cure chemistry can be convenient for field application. | Availability and cure behavior depend on the specific HTPB-based design. Deep or thick sections may cure slowly; carbon dioxide can contribute to bubbles if formulation and application are not controlled. Humidity, temperature, and joint geometry matter. | Apply from a sealed cartridge or pack and tool the exposed bead. Follow the supplier’s guidance on bead dimensions, humidity, and time before exposure. | Field work where avoiding on-site two-part mixing is important and the proposed product is specifically validated for HTPB-based sealant use. |
| Adhesion-promoted HTPB polyurethane | May use either a two-component hydroxyl–isocyanate cure or a one-component moisture cure, with adhesion promoters or primers selected for the substrate. | A primer or adhesion-promoting package can improve bonding to specific surfaces when validated as part of the system. | There is no universal primer for all metals, plastics, masonry, or coatings. Surface cleanliness, abrasion, primer flash-off, and compatibility are critical; test the complete system on representative substrates. | Prepare the substrate, apply the specified primer if required, then dispense and tool the sealant using the method suited to its cure system and viscosity. | Projects where durable adhesion to a particular substrate is a primary requirement and qualification testing is available. |
Selection note: HTPB sealant properties are formulation-dependent. Confirm joint movement, service temperature, chemical exposure, substrate adhesion, cure time, and applicable test requirements with product-specific data and representative trials. Isocyanate-containing components require appropriate handling, ventilation, and protective measures.
An HTPB sealant’s bond depends on both its formulation and the surface beneath it. Concrete may carry dust, laitance, or moisture; metal can have oil or oxidation; painted surfaces may fail within the coating. Clean a test area using the planned preparation method, then check adhesion after full cure. A neat bead is not proof of a durable bond. ASTM C920 classifies sealants by movement capability: Class 25 and Class 50 indicate ±25% and ±50% joint movement, respectively. Treat these figures as a selection benchmark, not a guarantee that a particular HTPB product meets either class.
Temperature and moisture matter during application and service. A cold substrate can slow curing, while direct sun may heat a joint and change how it moves. Record the surface temperature, weather, and joint dimensions during a field trial. Compare the conditions with the sealant’s technical data sheet and ASTM C1193 guidance for joint-sealant use.
Tips: Test each actual substrate, including its coating, before committing. Keep a small cured sample for inspection, and check for edge lifting or soft spots. The test patch takes time, but skipping it can cost more later.
A sealant can look sound in a sample tube and still fail on a real joint. Verify that its technical data identifies applicable test methods and clearly states the intended service conditions. Ask for batch-specific quality records, not only a general product sheet. Check whether reported properties include adhesion, hardness, elongation, and curing time. Results matter only when test methods and conditions are clear.
Test it on the actual materials, with realistic surface preparation and joint dimensions. Record temperature, humidity, mixing ratio, and cure time; small changes can affect performance. Small details matter. Compare cured samples against the project’s acceptance criteria, including expected movement, moisture, and chemical exposure. A tidy lab result is not the whole story. Field conditions can be uneven, and a short trial may miss slow changes. That limitation deserves attention.
Review the safety data before handling or testing. Confirm ventilation needs, protective equipment, storage limits, and disposal guidance. Make sure staff can follow the precautions in the work area, not just on paper. If a test result is unclear, repeat it or ask a qualified laboratory to evaluate the sample. Do not treat a pass on one substrate as proof of suitability everywhere. The right choice rests on documented evidence that matches the joint, the environment, and the people applying the sealant.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru