Choosing Weld Fixture Tooling in 2026 means balancing part accuracy, production speed, and the realities of your shop floor. A fixture must hold components securely, maintain repeatable joint alignment, and leave enough access for the welding process. It also needs to suit the part’s size, material, expected production volume, and changeover frequency. Fit matters.
Start with the weldment, not the catalog. Review drawings, tolerances, clamp locations, heat exposure, and the sequence operators will follow. Check whether the tooling can accommodate the welding torch, cables, and inspection equipment without awkward repositioning. For a small batch, adjustable tooling may justify its extra setup time. For steady production, dedicated locating points can support faster, more consistent loading. The best choice depends on actual cycle data, not assumptions.
Material and construction deserve close attention. A heavy fixture can resist movement, but excessive mass may slow handling and complicate maintenance. Replaceable wear surfaces, accessible clamps, and clear datum points can make daily use less frustrating. Yet no checklist predicts every distortion pattern. Trial welds, dimensional checks, and operator feedback reveal what drawings alone may miss. Record those results and revise the setup where needed. Sometimes the first fixture works, but not quite well enough.
This guide explains how to compare fixture types, assess accuracy and flexibility, and plan for safety, maintenance, and future product changes. Its aim is practical: help you choose tooling that supports reliable weld quality without adding needless complexity.
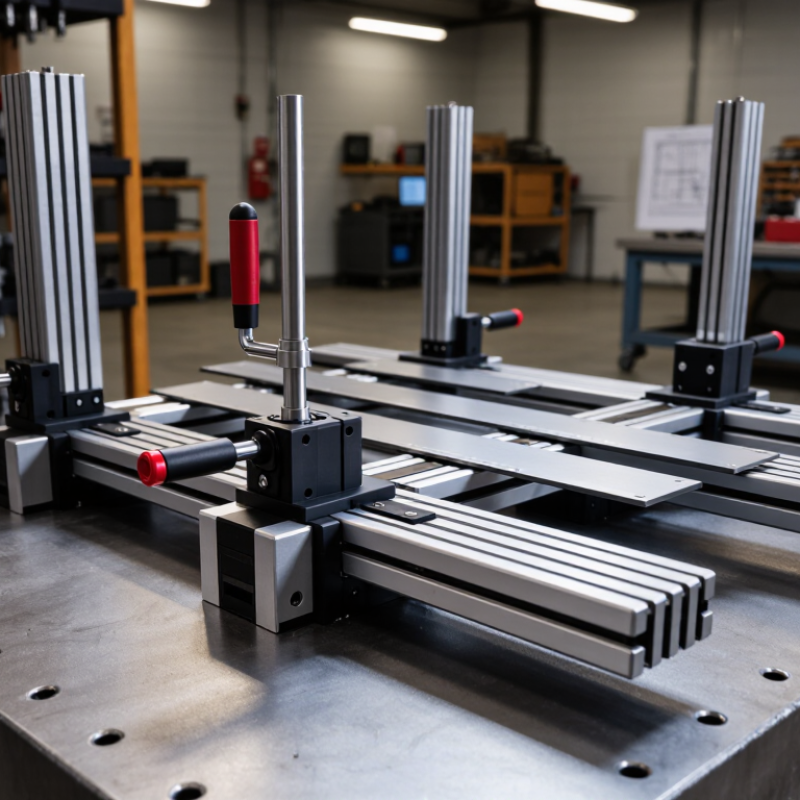
ISO 13920 provides general tolerances for welded constructions when individual dimensions lack specific limits. Its tolerance classes cover linear and angular dimensions, plus selected geometric characteristics. The drawing should identify the applicable class and any tighter, function-critical limits. Do not treat the standard as a substitute for defining how mating parts must fit.
Start fixture design with the part’s functional datums: perhaps a machined mounting face, two locating holes, and a welded edge. Relate clamp and support points to those datums, then check the tolerance stack between them. A class suited to a broad frame may be too loose for a close-fitting bracket. Conversely, unnecessarily tight limits can increase machining and inspection effort without improving assembly. Use the current applicable edition and verify class selection against the drawing and production needs.
Weld heat changes geometry. A fixture can hold parts in position, but it cannot erase poor fit-up or predict every distortion. Check sample parts after welding and cooling, measuring the critical interfaces rather than relying only on fixture dimensions. A small gap at a locating pin may reveal more than a perfect-looking setup. Sometimes the first fixture needs adjustment; that is useful evidence, not a design failure.
Define part geometry and tolerance needs using ISO 13920, then select fixture targets that support the critical features.
How to read this chart: Smaller values indicate tighter control. These are illustrative engineering targets, not tolerance values specified by ISO 13920. Confirm the applicable tolerance class and edition on the part drawing, and set fixture requirements around the critical datums and interfaces.
How to Choose Weld Fixture Tooling in 2026?
Match Fixture Design to Weld Sequence and AWS D1.1 Requirements
Choose tooling around the weld sequence, not just the finished part. Tack locations, clamp access, and release order affect movement as heat builds. AWS D1.1 sets requirements for structural steel welding, but it does not prescribe one universal fixture layout. Check the project’s specified code edition, approved welding procedure, joint details, and inspection access. Leave room for the welder to maintain the required position and for inspectors to examine critical welds. A clamp that blocks a visual check is a real design flaw.
Automation raises the stakes. The International Federation of Robotics reported 4,281,585 industrial robots operating worldwide in 2023 in its World Robotics 2024 report. For robotic cells, repeatable datums and secure part location help keep the programmed torch path aligned. Still, a fixture that looks perfect in CAD can trap spatter or make part removal awkward. Test a physical setup with the actual weld sequence; this step is easy to underestimate.
Tips: Mark clamp points on the weld sequence drawing. Confirm torch, electrode, and inspection access before release. Then check fit-up after tacking and again after cooling. Record what shifts. Some distortion will remain, and that is worth reviewing before production.
| Assembly / Weld Sequence | Suitable Fixture Tooling | Location and Restraint Strategy | Sequence and Distortion Control | AWS D1.1 Considerations | Checks Before and After Welding |
|---|---|---|---|---|---|
| Plate-to-plate T-joint Welded along one or both sides; long joints may be completed in segments. | Flat weld table with adjustable stops, removable clamps, and access for the specified weld process. | Locate the plate from stable datum faces. Use enough restraint to maintain alignment while allowing for thermal movement and weld access. | For long joints, consider a balanced or segmented sequence when permitted by the approved welding procedure. Avoid locking the assembly so tightly that it cannot accommodate shrinkage. | Confirm the applicable approved WPS, joint details, welder qualifications, preheat requirements, and inspection provisions. AWS D1.1 does not prescribe a universal fixture layout. | Verify joint fit-up, alignment, and access before welding. After release, check dimensions, angular distortion, and weld acceptance criteria specified for the project. |
| Beam or girder with repeated stiffeners Stiffeners are positioned and welded at multiple stations. | Beam bed with adjustable station stops, squaring blocks, and removable hold-downs set clear of the weld path. | Establish a primary beam datum and use station stops to control stiffener spacing. Check web alignment at several points rather than relying on one end stop. | Use a documented station order and a consistent weld-side pattern. Where appropriate, alternate locations or sides to limit cumulative bow and twist; validate the sequence on a representative assembly. | Ensure the joint preparation, WPS variables, preheat, and required inspection are followed. Confirm any specified dimensional tolerances against the contract documents and applicable code requirements. | Check stiffener location, squareness, and web position during fit-up. Measure camber, sweep, and twist after welding and after the fixture is released. |
| Box section or closed assembly Multiple sides are joined in an order that may restrict later access. | Modular nest with removable side supports, accessible clamp points, and clearance for the torch, electrode, or inspection equipment. | Use repeatable corner and end datums. Design clamps and supports to be removable in sequence so they do not block required welds or inspection access. | Plan the weld order before closing the section. Complete inaccessible welds at the appropriate stage, and use a balanced sequence to reduce the risk of pulling the section out of square. | Verify that welds can be made and inspected as required by the project. Follow the applicable WPS and code requirements for workmanship and inspection; do not treat the fixture as a substitute for these controls. | Confirm access, root opening or fit-up where specified, and planned inspection access before closing. Check section dimensions and squareness after cooling and release. |
| Thin-gauge attachment to a heavier member Short welds can produce localized distortion or burn-through risk. | Low-mass, adjustable clamping with smooth contact pads; add a qualified heat sink only when suitable for the process and procedure. | Support the thin component close to the joint without creating a gap or obstructing the weld. Avoid excessive clamping force that can deform the part before welding. | Use the approved procedure and a controlled weld order. Distribute welds where the design allows, and confirm that any intermittent-weld pattern matches the drawings. | Use a WPS applicable to the joint, material, thickness range, and process. Check specified preheat and other procedure requirements rather than assuming thin material needs none. | Inspect fit-up and component flatness before tacking. After welding, check for distortion and inspect the weld to the project’s applicable acceptance requirements. |
| Repetitive bracket or lug production Identical parts are located and welded in a repeatable cycle. | Dedicated nest or modular fixture with hardened locating faces, replaceable wear components, and clearly defined clamp positions. | Use a consistent datum scheme that prevents incorrect orientation. Design stops to locate the part without hiding the joint or limiting required weld access. | Standardize tack locations and the production weld order. Review the first completed parts for dimensional drift and revise the fixture or sequence if results are inconsistent. | Keep production controls aligned with the approved WPS and project inspection plan. Confirm that welders and welding operators meet applicable qualification requirements. | Perform first-piece dimensional and visual checks, then use a defined in-process sampling plan. Recheck locator wear and clamp condition at planned intervals. |
| Large or flexible structural frame Several members meet at multiple joints and may move as welds are added. | Adjustable strongback or modular bed with measured reference points, removable braces, and accessible locations for dimensional checks. | Support the frame at planned points and locate from a controlled datum. Use temporary bracing only when its removal and effect on final geometry have been planned. | Develop a staged sequence that considers joint accessibility, heat input, and accumulated shrinkage. Measure at defined stages instead of relying solely on final inspection. | Apply the contractually specified AWS D1.1 edition and project requirements. Confirm WPS coverage, preheat, workmanship, inspection, and any required records with the responsible welding authority. | Record baseline dimensions, intermediate measurements, and final geometry after cooling and release. Investigate repeatable movement before adding permanent preset or restraint. |
Note: Fixture choices and weld sequences are fabrication planning guidance, not a substitute for the contract documents, the applicable AWS D1.1 edition, an approved WPS, or required inspection. Confirm project-specific requirements with the responsible welding coordinator or engineer.
Manual, modular, and robotic tooling solve different changeover problems. Manual fixtures often suit low-volume work with stable part designs. An operator can reposition clamps, stops, and locators with basic tools. The setup is straightforward, but every adjustment takes time. That matters. If changeovers happen daily, small delays can accumulate, and inconsistent clamp positions may affect fit-up. Record setup dimensions and verify the first part after each change.
Modular tooling offers adjustable plates, locators, and clamps that can be rearranged for different parts. It can reduce changeover time without the full complexity of automation. However, modules still need accurate positioning and careful storage; missing components can slow a shift. Robotic tooling may suit repeatable, high-volume production with frequent model switches. Quick-change interfaces and programmed tool paths can make transitions more consistent, but only when part data and process validation are reliable. Not always. A robot does not fix poor locating strategy. Compare actual changeover frequency, labor, part variation, and maintenance capacity before investing. A simple timed trial can reveal whether flexibility is worth the added setup discipline.
Choosing weld fixture tooling in 2026 means setting accuracy from real robot data, not a catalog number. ISO 9283 provides methods for measuring robot performance, including pose repeatability. Repeatability is not absolute accuracy. A robot may return consistently to a point that is slightly off.
Check the repeatability data for the payload, speed, pose, and conditions closest to your welding cell. A wrist-mounted torch and cable bundle can affect behavior. So can reach and approach direction. Record variation at the actual weld locations, especially corners and deep joints. Small shifts matter when a torch must hold a tight angle.
Use those measurements to build an accuracy budget alongside part variation, fixture manufacturing tolerance, and clamping movement. Keep the fixture’s contribution small enough for the weld process to meet its requirements. That sounds tidy, but production rarely is. Independent errors may combine differently, so avoid relying on a single theoretical calculation. Validate with repeated robot approaches and a measured test part. Look for movement after clamping, then check the torch path against the joint. If the results drift, revisit the datum scheme or locator contact—not just the robot setting.
Choosing weld fixture tooling in 2026 means checking more than cycle time. The fixture should hold parts consistently without blocking the weld path, inspection points, or safe operator movement. Confirm that clamps resist expected heat and spatter, and that locating surfaces remain stable across repeated cycles. Small shifts matter.
ISO 3834 focuses on welding quality controls, so tooling should support documented, repeatable production. Check whether the fixture helps maintain joint fit-up, access for inspection, and traceability of setup changes. A practical trial weld can reveal gaps that drawings miss. Record the settings and results, then review them with qualified welding personnel. Not every production line needs the same controls; the applicable quality level depends on the work and its requirements.
OSHA 1910.252 addresses welding and cutting hazards, including fire prevention and ventilation. Keep fixtures from obstructing screens, fume extraction, or clear access to fire-control equipment. Look for sharp edges, pinch points, and awkward clamp handles that may expose operators to burns or hand injuries. Check nearby combustibles and hot-work arrangements before production begins. The fixture alone cannot ensure compliance. Procedures and training still matter. In practice, a convenient clamp can create a poor reach or hide a hazard, so reassess the setup after operators use it on the shop floor.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru