Cnc Lathe Parts are used in equipment where fit, finish, and repeatability matter. A turned shaft may look simple, yet a small variation in diameter can affect assembly or service life. For global buyers, choosing a manufacturer involves more than comparing unit prices. Material availability, production capacity, inspection practices, and communication all influence the result.
This guide introduces manufacturers serving international customers and outlines practical points for evaluating them. Look for clear information about materials, machining capabilities, tolerance control, and quality documentation. Ask how suppliers inspect critical dimensions, manage batch consistency, and handle changes to drawings. A polished website is not proof of reliable production. Samples and technical discussions offer better evidence.
Details matter. So does follow-through.
No supplier fits every project. A high-volume producer may suit repeat orders, while a smaller specialist may offer closer engineering support for complex parts. Lead times can also change with material sourcing, finishing requirements, and shipping arrangements. Buyers should verify capabilities directly and compare quotations using the same specifications. The manufacturers featured here provide a starting point, not a universal ranking. Some details may need closer review; supplier claims deserve thoughtful questions. With careful checks, buyers can make a more informed shortlist and build relationships based on measurable performance.
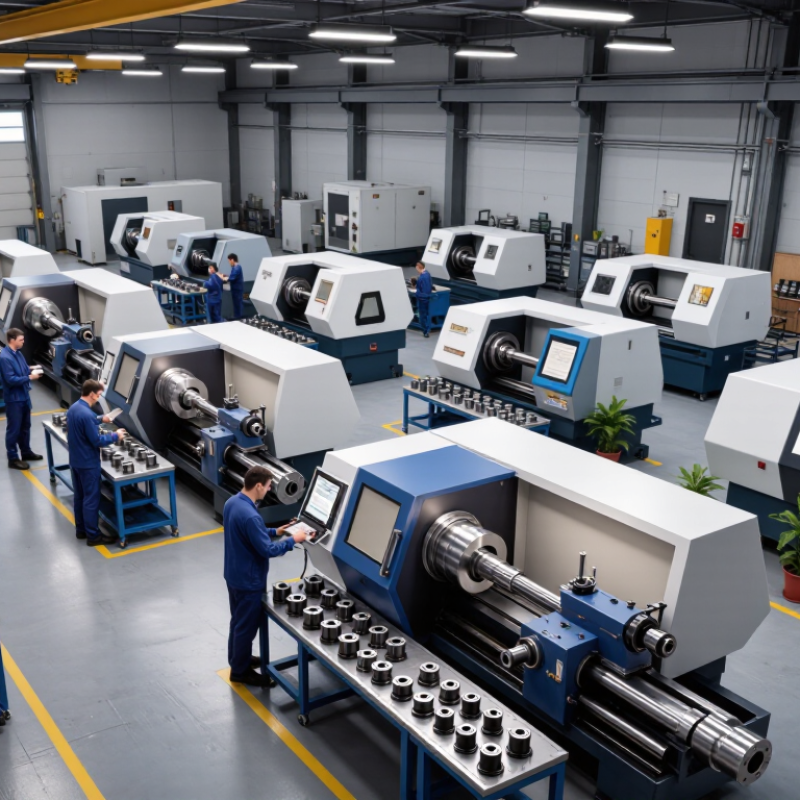
CNC lathe parts are made by rotating a workpiece against a cutting tool. The tool removes material along the part’s axis or across its face. This process creates precise diameters, shoulders, grooves, bores, and threads. A typical turned shaft might have a narrow bearing seat, a larger central section, and a chamfered end.
Common geometries include straight shafts, stepped pins, bushings, sleeves, flanges, and tapered components. Many are symmetrical around a central axis, but their details vary. A sleeve may need a smooth outer diameter and a carefully sized internal bore. A stepped shaft may require accurate transitions between diameters. Cross-holes or flats can sometimes be added with live tooling, depending on the machine setup.
Fit matters. During inspection, manufacturers may check diameters with micrometers and verify bore sizes with suitable gauges. Surface finish, thread dimensions, and burrs also affect assembly. A clean-looking part can still be wrong. That is easy to miss. Drawings sometimes leave edge breaks or finish requirements unclear, so buyers and machinists should resolve those details before production.
For global buyers comparing CNC lathe parts manufacturers, ISO 2768-1 Medium class gives a useful baseline for unspecified linear dimensions. For dimensions greater than 30 mm and up to 120 mm, the permitted deviation is ±0.3 mm. A 60 mm feature could therefore measure from 59.7 mm to 60.3 mm, provided the drawing does not specify a tighter tolerance. Check the drawing notes carefully.
This allowance may suit non-critical lengths or shoulders, but it can be too broad for a shaft intended to fit a bearing. A micrometer reading near either limit might pass the general tolerance while still causing trouble during assembly. Check critical diameters, fits, and locations against their individual drawing tolerances. ISO 2768-1 does not replace geometric tolerances or define surface finish.
When reviewing a supplier, ask how dimensions are measured and whether inspection records identify the actual readings. Temperature, burrs, and the measuring tool can affect results. Small details matter. A practical reminder: a quoted tolerance is only useful when both parties apply it to the same feature and measurement method. I would double-check any unclear drawing note before production; it is an easy step to miss.
For global buyers, a turned part’s finish should be more than “smooth” or “as machined.” ISO 21920:2021 provides a common profile-based framework for stating and evaluating surface texture. Its three parts cover drawing indications, parameters, and specification operators. That shared language helps buyers compare quotations and inspection results across suppliers.
A callout such as Ra 0.8 µm gives useful information, but it does not describe every surface feature. Two turned parts can share the same Ra and still differ in peak shape, spacing, or directionality. ISO 21920-2:2021 defines profile parameters, while ISO 21920-3:2021 addresses how specifications are evaluated. The drawing should also make relevant settings clear, including the evaluation length and filtering approach. Small details matter.
During inspection, the stylus should cross the turning marks rather than follow them. Otherwise, the measured profile may understate the texture. A stated tolerance and agreed measurement method make supplier data easier to compare. Still, one reading is not the whole story; instrument setup and part location can affect results. Buyers should ask for traceable measurement records, especially when finish affects sealing, friction, or coating adhesion. A neat Ra figure can look reassuring, but without its measurement context, it may leave room for costly interpretation.
For global buyers, a CNC lathe supplier’s certificate is a starting point, not proof that every shaft or bushing will meet specification. ISO’s Survey of Management System Standard Certifications, 2022, recorded 1,265,216 valid ISO 9001 certificates across 189 countries and economies. That scale makes certification useful for screening, but buyers still need to check the certified site, scope, and current status.
ISO 9001 asks suppliers to manage processes, document controls, address risks, and improve quality. IATF 16949 adds automotive-specific requirements, including stronger controls for traceability, supplier performance, and production changes. On a shop-floor visit, ask how a revised tool offset is recorded, who approves it, and whether the measurement system is calibrated. Paper is not proof. A polished certificate cannot show whether the batch on your order was inspected correctly.
For CNC parts, request recent inspection records tied to the drawing revision, material certificates, and evidence of corrective action for nonconforming parts. Check whether the supplier monitors key dimensions, such as bore diameter or runout, through production—not only during final inspection. A capable supplier should explain its control plan in plain language and show how it handles a failed measurement. Even then, audits have limits; sampling can miss a recurring issue, and buyers should verify performance through incoming inspection and delivery data.
Top CNC Lathe Parts Manufacturers for Global Buyers
Choosing a CNC lathe parts manufacturer takes more than comparing hourly rates. Start with materials: ask whether the shop regularly machines your specified alloy, and request material certificates tied to each production lot. For capacity, compare spindle size, machine hours, batch flexibility, and realistic lead times—not just the number of machines on the floor. Deloitte and the Manufacturing Institute’s 2024 smart manufacturing survey found that 92% of surveyed manufacturing executives expect smart manufacturing to drive competitiveness within three years. Digital records can help buyers track inspection results, but only when measurement methods are clearly documented.
Tips: Request a sample inspection report showing critical dimensions, tolerances, and measurement equipment. Ask how the supplier handles tool wear during long runs. A polished sample is useful, but it does not prove stable production. Look for evidence from repeat orders, such as consistent measurement trends and documented corrective actions. If the supplier cannot explain how it checks a small bore or thread, pause. That gap matters. Good comparisons also consider communication speed and whether quality records arrive with each shipment. These details may seem minor; they can still affect assembly and delivery schedules.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru