Choosing the right Multi Lane Packing Machine manufacturer requires more than comparing speed claims. Packaging lines must match product behavior, material structure, factory space, and operator skills.
This guide examines leading manufacturers worldwide through practical and technical criteria. It considers machine design, dosing accuracy, sealing stability, lane synchronization, and changeover time. A reliable machine should handle real production conditions, not only showroom samples. For example, powder may create dust around the forming tube, while sticky products can affect filling consistency. Film tracking also becomes critical when several lanes run continuously.
Manufacturers with strong engineering experience usually provide detailed testing, documented specifications, and responsive service. Their teams should explain suitable materials, expected output, maintenance intervals, and spare-part availability. Demonstrations using your actual product can reveal problems early. Small details matter, including accessible sensors, clear control screens, and tool-free adjustments.
No ranking is perfect. Different factories need different strengths. A compact line may suit a growing producer, while a large facility may prioritize automation and high uptime. Buyers should review safety systems, installation support, training, and long-term operating costs. Initial price alone can mislead.
The manufacturers discussed here represent important options across international markets. Their capabilities may vary by product type, package size, and regional service coverage. Careful comparison remains essential. Ask precise questions. Request evidence. Then select equipment that supports consistent quality, efficient production, and dependable daily operation.
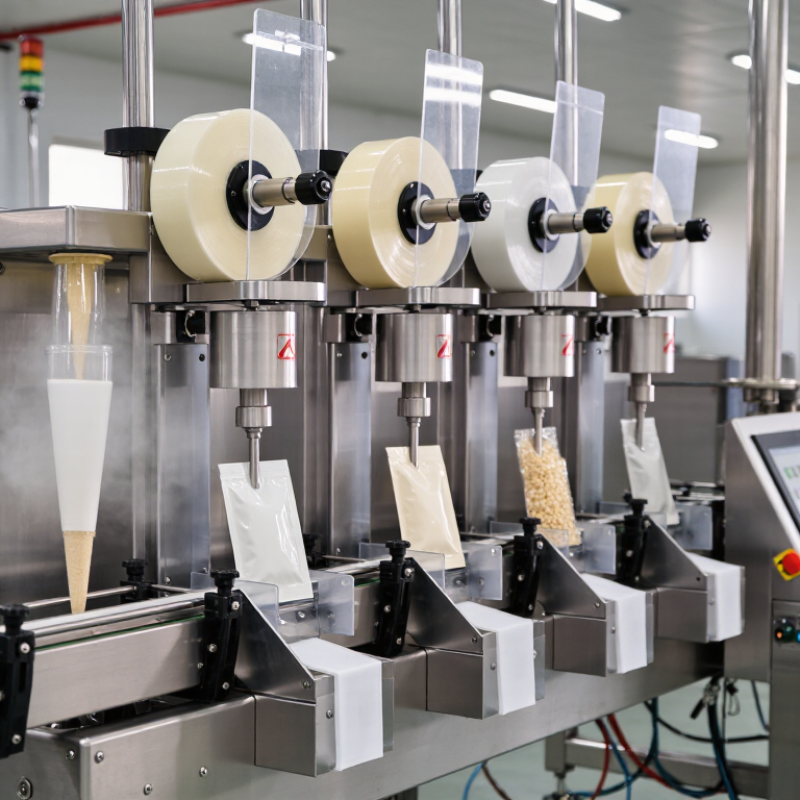
A multi-lane packing machine divides one product stream into several parallel lanes. Each lane measures, fills, and seals an individual pack. This design increases output without requiring one extremely fast line. Typical systems handle powders, granules, liquids, or small solid pieces. Product shape and flow behavior determine the correct dosing method. That detail matters.
During operation, an infeed system distributes product across multiple lanes. Volumetric cups, augers, pumps, or weighers control the fill. Forming collars shape film around each portion. Heated sealing jaws close the package, while cutters separate finished units. Sensors check film position, temperature, registration marks, and missing product. Servo drives synchronize feeding, sealing, and cutting. In practical production, stable synchronization protects accuracy and seal quality. A small timing error can create leaking packs or uneven weights.
Choosing a machine requires more than comparing lane numbers. Operators should test the actual product, packaging material, target weight, and cleaning routine. Washdown needs, changeover time, spare parts, and operator access also affect reliability. More lanes can raise capacity, but they may increase adjustment work and start-up waste. It is not a magic solution. A poorly balanced system may run quickly yet produce inconsistent packs. Good commissioning includes trial runs, recorded measurements, and operator training. Performance can still change with humidity, product temperature, or film variation. Honest monitoring remains essential.
Multi-lane packing machines divide one product flow into several synchronized lanes. Each lane forms, fills, seals, and cuts individual sachets. The process starts with a controlled film roll. Guide rollers pull the film through forming collars, creating narrow pockets. A servo-driven dosing system then delivers a measured portion into each pocket. Timing matters. Even a small delay can cause uneven fills or weak seals.
After dosing, heated sealing jaws close the longitudinal and cross seals. A cutting unit separates the finished packs at fixed intervals. Sensors check film position, product presence, temperature, and registration marks.
If one lane drifts, the control system can adjust speed or stop the machine. This protects consistency, but it cannot correct every material problem. Film tension, humidity, and product shape still influence performance.
From practical installation work, operators need more than fast output. They must inspect sealing surfaces, clean dosing parts, and verify lane alignment during changeovers. Poor cleaning can create buildup around narrow filling channels. That issue is easy to miss.
Modern machines use touch-screen controls and recipe storage, yet skilled judgment remains important. A setting that works for powder may fail with granules or irregular pieces. Manufacturers with strong engineering support usually provide trial testing, operator training, and clear maintenance access. Even then, production teams should record seal pressure, temperature, and rejected packs instead of trusting the display alone.
Comparing Multi Lane Packing Machine manufacturers requires more than checking advertised speed. A machine may run 300 packs per minute in ideal conditions, yet perform differently with powder, granules, or sticky products. Ask for product trials using your actual materials. Request videos, sample packs, and measured production data.
Lane flexibility matters during product changes. Look for independent lane control, servo-driven dosing, and accurate film tracking. Quick-release forming parts can reduce cleaning and changeover time. Inspect seal consistency closely. Weak seals often appear after long runs, not during a short demonstration. The control system should record alarms, temperature changes, and rejected packs. Clear data supports maintenance decisions.
Hygiene and access deserve careful attention. Stainless steel contact areas, sloped surfaces, and tool-free access simplify daily cleaning. Check whether operators can reach sensors safely. Spare-part availability also affects real reliability. Ask about local technicians, remote diagnostics, training, and response times. Compare electrical standards and documentation for each market. Some manufacturers provide impressive brochures but incomplete service details. That gap deserves scrutiny. Total cost includes film waste, compressed air, energy, labor, and planned downtime. A lower purchase price may hide expensive adjustments. Even experienced buyers can overlook this point. A factory acceptance test with agreed performance limits creates stronger evidence than promises alone.
This benchmark compares typical output ranges by lane count without displaying company or brand data. The range is calculated from a conservative operating speed of 30–60 packing cycles per minute, with one pack produced per lane during each cycle.
When comparing global manufacturers, buyers should also evaluate dosing accuracy, film compatibility, stainless-steel hygiene design, changeover time, PLC and HMI functions, service coverage, and compliance with applicable food-packaging standards.
Leading multi-lane packing machine manufacturers worldwide combine mechanical precision with practical production experience. Their systems divide products into several lanes before filling, sealing, or counting them. This design can increase output while using limited floor space. Experienced manufacturers first study product shape, moisture, speed, and packaging material. A factory trial often reveals problems that drawings miss. Small details matter.
Reliable suppliers provide stainless steel contact parts, clear guarding, and accessible cleaning areas. Their engineers should explain lane balancing, film tension, sealing temperature, and sensor calibration in measurable terms. Proper documentation supports installation, operator training, maintenance, and audits. Testing should include real products and production-speed conditions. Otherwise, performance claims remain uncertain.
Leading manufacturers also invest in remote diagnostics and replaceable components. Response time matters when one sensor stops a complete line. Yet no machine is perfect. Product variation, dust, vibration, and operator habits can reduce efficiency. A careful supplier admits these limits and recommends practical controls. Buyers should compare acceptance tests, spare-part availability, safety records, and local technical support. The strongest partnership develops through transparent data, repeated trials, and honest discussion of costly weaknesses.
Top Multi Lane Packing Machine Manufacturers Worldwide
Multi-lane packing machines serve high-volume production where small products require consistent dosing and sealing. Common applications include snack portions, powdered drinks, pet treats, wet wipes, and personal-care sachets. A twelve-lane system can fill many packs per cycle. However, speed alone is not enough.
Selection should begin with the product. Granules may need multihead weighing, while powders require auger dosing and dust control. Liquid products demand stable pumps and accurate flow management. Check film width, pack dimensions, seal style, and target output before comparing manufacturers. Ask for a live trial using your actual product. Small differences in moisture can change filling accuracy.
A reliable supplier should explain changeover time, cleaning access, safety controls, and spare-part availability. Servo-driven systems often improve registration and reduce adjustment waste, but they also require skilled maintenance. Inspect the sealing jaws closely. Uneven temperature can create weak edges or wrinkled seals. Review electrical standards, documentation, training, and remote support for each market. Total cost includes film waste, compressed air, labor, and planned downtime. The cheapest quotation may become expensive after installation. I have seen specifications look impressive, yet operators struggled with daily cleaning. That weakness deserves attention. Make room for manual checks, because sensors can miss unusual product behavior.
The following table summarizes common multi-lane packing machine configurations, applications, and practical selection criteria. Performance values are typical industry ranges and may vary according to product characteristics, package size, film type, dosing system, and local compliance requirements.
| Application / Product Type | Recommended Lane Configuration | Typical Output Range | Suitable Dosing Method | Common Package Format | Important Selection Factors |
|---|---|---|---|---|---|
| Powdered beverages, instant coffee, spices, and seasonings | 4–12 lanes | Approximately 120–1,000 sachets per minute, depending on lane count and fill volume | Auger filler or volumetric cup filler | Three-side-seal or four-side-seal sachet | Dust control, auger accuracy, anti-static design, seal cleanliness, and powder compatibility |
| Liquid products such as sauces, oils, detergents, and cosmetic samples | 2–12 lanes | Approximately 60–600 sachets per minute | Piston, pump, or flow-meter filling system | Pillow sachet, stick pack, or four-side-seal pouch | Viscosity range, drip prevention, hygienic construction, cleaning access, and seal integrity |
| Granules, sugar, salt, rice, seeds, and small hardware components | 4–12 lanes | Approximately 100–800 sachets per minute | Volumetric cup, multi-head combination weigher, or linear weigher | Pillow bag, stick pack, or sachet | Particle size distribution, bridging risk, product flowability, target weight, and vibration control |
| Snacks, confectionery pieces, nuts, and small baked products | 2–8 lanes | Approximately 50–400 packs per minute | Multi-head weigher, linear weigher, or counting system | Pillow bag, gusseted bag, or stick pack | Gentle product handling, target-weight accuracy, anti-bridging design, and discharge timing |
| Medical, pharmaceutical, and laboratory powders | 2–10 lanes | Approximately 60–500 sachets per minute | Servo auger or other validated precision dosing system | Unit-dose sachet or stick pack | Batch traceability, cleanability, recipe control, dose verification, and applicable GMP requirements |
| Seeds, fertilizers, pet treats, and agricultural products | 2–8 lanes | Approximately 40–350 packs per minute | Linear weigher, volumetric cup, or auger filler | Pillow bag, sachet, or small pouch | Abrasion resistance, moisture protection, dust management, product variability, and sealing temperature |
| Selection Dimension | What to Evaluate | Practical Recommendation |
|---|---|---|
| Required production capacity | Required packs per minute, operating hours, product changeover frequency, and expected production growth | Select the lane count based on the required sustained output rather than the highest advertised speed. Include reasonable capacity for downtime and changeovers. |
| Product characteristics | Bulk density, particle size, moisture, viscosity, flowability, fragility, abrasiveness, and temperature | Conduct product trials using representative materials before finalizing the dosing system and lane configuration. |
| Fill-weight accuracy | Target fill weight, permitted tolerance, statistical control requirements, and reject handling | Compare test results at the intended speed and product temperature; do not assess accuracy only at low-speed operation. |
| Film and package format | Film width, laminate structure, thickness, sealant layer, package dimensions, and tear-notch requirements | Confirm film compatibility, maximum web width, sealing temperature range, registration control, and package-size changeover limits. |
| Machine construction and hygiene | Stainless-steel contact parts, drainage, tool-free access, washdown suitability, guarding, and cleanability | For food, pharmaceutical, or cosmetic use, prioritize hygienic design and documented material compatibility. |
| Automation and controls | Servo drives, touchscreen recipes, automatic film tracking, fault diagnostics, remote access, and data collection | Choose controls that support repeatable changeovers, operator access control, production reporting, and integration with upstream and downstream equipment. |
| Changeover performance | Changeover time, tool requirements, recipe storage, adjustment points, and accessibility | Evaluate the complete changeover procedure with the actual products, films, and package sizes planned for production. |
| Reliability and service support | Spare-parts availability, technical response time, preventive-maintenance requirements, training, and documentation | Request a recommended spare-parts list, service-level terms, operator manuals, electrical drawings, and maintenance schedules before purchase. |
| Safety and compliance | Guarding, emergency stops, electrical safety, risk assessment, local regulations, and applicable market requirements | Verify conformity documentation and site-specific requirements before shipment and installation. |
| Total cost of ownership | Purchase price, utilities, film waste, labor, maintenance, spare parts, downtime, and expected service life | Compare cost per acceptable pack over the planned operating period instead of comparing equipment price alone. |
Note: Actual output, accuracy, machine dimensions, power consumption, and compatible materials should be confirmed through a formal technical specification and product test.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru