What Is PE Coloring Masterbatch Used For?
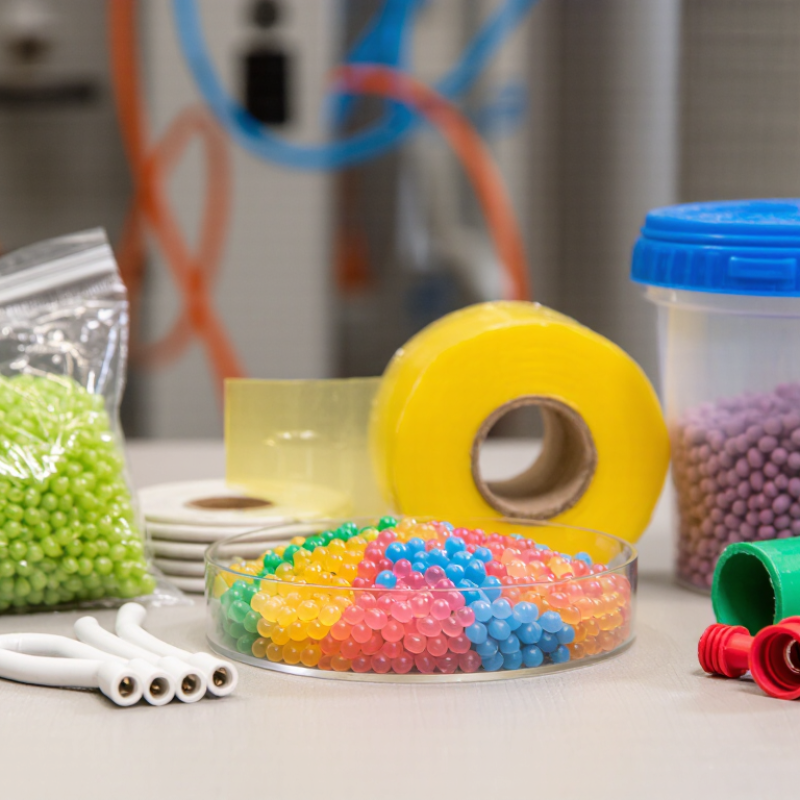
Pe Coloring Masterbatch is a concentrated blend of pigments, polymers, and performance additives. Manufacturers use it to create consistent colors in plastic products. These products include packaging films, pipes, household containers, automotive parts, and electrical components. A small masterbatch dosage can tint a large volume of resin. This improves handling compared with measuring loose pigments on the production floor.
The commercial importance is substantial. PlasticsEurope reported global plastics production of about 400.3 million tonnes in 2022. That scale creates constant demand for reliable, repeatable coloration. Grand View Research has also identified masterbatch as a growing plastics-processing market, supported by packaging, construction, and automotive applications. These reports provide useful direction, although market estimates differ by region, product definition, and research method.
Color is only one function. A suitable Pe Coloring Masterbatch must disperse evenly, match the target shade, and remain stable under heat and processing pressure. For example, a film producer may need a uniform blue across a 1,000-meter roll. Poor dispersion can create streaks, specks, or weak visual coverage. That is expensive.
Professional selection also considers resin compatibility, loading level, food-contact requirements, weather resistance, and recycling goals. The OECD reported that only about 9% of global plastic waste was recycled in 2019. Therefore, colorants should not be chosen without considering the final product’s recovery pathway. This point is often underestimated. In practice, the cheapest masterbatch may increase waste, cleaning time, or rejected production. A careful technical trial remains essential, because laboratory color results do not always predict factory performance.
What Is PE Coloring Masterbatch?
PE coloring masterbatch is a concentrated color additive designed for polyethylene products. It combines pigments with a compatible polyethylene carrier resin. The mixture is heated, blended, and formed into small pellets.
These pellets disperse color during film blowing, extrusion, injection molding, or blow molding. They make pigment dosing cleaner and more consistent than adding loose powder. It is not a magic powder.
In practical production, PE coloring masterbatch is used for plastic bags, packaging films, containers, pipes, sheets, and household parts. The masterbatch is mixed with natural or recycled polyethylene at a controlled dosage. A suitable carrier helps the color spread evenly through the melt. Poor compatibility may create streaks, weak spots, or uneven shades.
Technicians often begin with a small trial batch, then adjust the loading rate after checking the finished product. Small changes matter.
Reliable selection requires more than matching a color sample. Pigment heat resistance, light stability, migration performance, and melt-flow behavior should suit the application.
Operators should also check moisture, processing temperature, screw speed, and residence time. Excessive masterbatch can raise cost or affect mechanical properties. Too little can produce dull or inconsistent color.
A technical data sheet and batch traceability improve quality control, although testing remains necessary. Laboratory results may not fully predict a fast production line.
How PE Coloring Masterbatch Works in Plastic Manufacturing
What Is PE Coloring Masterbatch Used For?
How PE Coloring Masterbatch Works in Plastic Manufacturing
PE coloring masterbatch is used to give polyethylene products consistent, controlled color. It contains concentrated pigments or dyes inside a polyethylene-based carrier. During manufacturing, workers blend a measured amount with natural PE pellets. The mixture then enters an extruder, where heat and shear soften the polymer and distribute the color throughout the melt.
The carrier matters. It helps the color concentrate mix smoothly with the base resin. A suitable carrier can improve dispersion and reduce visible streaks, specks, or uneven shading. Operators usually adjust the let-down ratio according to the required color strength. Film, pipe, packaging, and molded parts may need different pigment levels. Small errors show. Poor feeding can create color bands across a film roll.
Temperature control also affects performance. Excessive heat may weaken certain pigments or change the final shade. Moisture, contamination, and inconsistent pellet feeding can cause additional defects. For this reason, production teams often inspect a trial sample before full-scale manufacturing. They compare it under standard lighting and check color, surface appearance, and mechanical properties.
In practice, the first trial is rarely perfect. A slight adjustment to pigment loading or extrusion conditions may be necessary. Color matching should not rely only on visual judgment. Instrumental testing provides more reliable data, although operators still need practical experience to interpret the results. The best process balances accurate dosing, stable processing, and the end product’s performance requirements.
Common Applications of PE Coloring Masterbatch
PE coloring masterbatch is a concentrated blend of pigments, additives, and a polyethylene carrier resin. It adds stable color during extrusion, injection molding, or blow molding. The operator mixes a measured amount with natural PE pellets. This process reduces pigment dust and supports more consistent dosing. Small errors still matter. An incorrect let-down ratio can create streaks, shade variation, or weak surface gloss.
Packaging remains its largest application area. PlasticsEurope reported that packaging represented 39.6% of European plastics demand in 2021. PE coloring masterbatch is used in shopping bags, shrink films, stretch films, caps, bottles, and flexible pouches. Transparent blue film may improve visual clarity, while white masterbatch can increase opacity in dairy containers. Colored caps also help users distinguish product types quickly. However, heavy pigmentation may complicate recycling or optical sorting, especially with very dark shades.
Agriculture uses colored PE films, irrigation components, and mulch films. Black mulch film helps limit light reaching weeds and can support soil moisture control. In construction, masterbatch colors ducts, protective sheets, pipes, and cable insulation. Household products, including storage boxes, bins, and toys, also depend on repeatable color matching. The OECD’s Global Plastics Outlook recorded 460 million tonnes of global plastic production in 2019, showing the scale of these applications. Yet color selection should consider end use, weather exposure, food-contact requirements, and recycling systems. A vivid shade is not always the most responsible choice.
Benefits of Using PE Coloring Masterbatch
PE coloring masterbatch is used to give polyethylene films, bags, pipes, containers, and molded parts a stable, uniform color. It contains concentrated pigments or dyes dispersed in a compatible carrier resin. Processors add it during extrusion or injection molding. This method is cleaner and more consistent than handling loose powder pigments. PlasticsEurope reported global plastics production of 400.3 million tonnes in 2022. Such scale makes efficient color control important for reducing processing errors and material loss.
The main benefit is reliable shade distribution. A well-formulated masterbatch can improve opacity, visual identification, and product appearance with a relatively small addition rate. It also supports automated dosing, which helps reduce operator contact and batch-to-batch variation. For outdoor polyethylene products, selected color systems may improve resistance to sunlight and weathering. However, color is not a perfect fix. Incorrect dosing, poor mixing, or incompatible carriers can create streaks and uneven surfaces. Smithers’ industry analysis identifies performance, sustainability, and processing efficiency as continuing priorities in the masterbatch market. These benefits depend heavily on testing.
Tips: Match the carrier resin with the PE grade. Check melt flow, dispersion, and heat stability before production. Use a calibrated dosing unit. Keep a retained color sample for comparison. ASTM or ISO testing can support more reliable quality decisions, although real production conditions may still expose weaknesses.
How to Select and Apply PE Coloring Masterbatch
What Is PE Coloring Masterbatch Used For?
How to Select and Apply PE Coloring Masterbatch
Polyethylene coloring masterbatch gives films, pipes, containers, and molded parts consistent color. PlasticsEurope reported 400.3 million tonnes of global plastics production in 2022. This scale makes stable, efficient coloring important for processors. Select a masterbatch with a polyethylene carrier that matches the base resin. Check melt flow rate, pigment loading, heat stability, and required opacity. A mismatch can create streaks, specks, or weak weld lines. Color measurement should use a spectrophotometer, not eyesight alone. Small differences often become visible under retail lighting.
Application depends on the machine and product thickness. Start with the supplier’s recommended let-down ratio, then adjust through controlled trials. Many processors begin between 1% and 4%, but strong pigments may need less. Dry blending must be uniform before feeding. Keep pellets clean and moisture-free, even though PE absorbs little water. Record barrel temperatures, screw speed, output, and color values. ISO 1133 melt-flow testing can help compare resin and masterbatch behavior. I have seen operators overlook residence time. That can cause pigment degradation and unexpected shade changes.
Tips: Use the same resin grade during color trials. Purge before changing shades. Inspect a thin film against white and black backgrounds. Do not judge color immediately after molding; cooling can change appearance. A lower dosage may reduce cost, but it can also reduce coverage. Recheck the formula after recycled content, additives, or processing conditions change. No recipe works forever.
What Is PE Coloring Masterbatch Used For?
PE coloring masterbatch is used to add consistent color to polyethylene products such as films, bags, bottles, containers, pipes, profiles, and molded parts. The chart shows typical starting let-down ratios by application.
A lower dosage is commonly used for thin films and light shades, while thicker molded products or applications requiring stronger opacity may need more masterbatch. Final selection should consider pigment concentration, color strength, polyethylene grade, processing temperature, product thickness, and required light or weather resistance. These figures are typical starting points; production trials are required for final adjustment.