Choosing the right surface stress meter can shape the accuracy of an entire measurement process. The instrument may look compact, yet its readings depend on sensor design, calibration, sample geometry, and operator technique. A polished screen does not guarantee dependable results.
This guide examines seven practical considerations before purchase. These include measurement range, resolution, repeatability, probe compatibility, calibration support, data handling, and service quality. Each factor matters when testing coatings, glass, films, or other engineered surfaces. For example, a meter used beside a production line may need a rugged body and quick stabilization. A laboratory model may require finer resolution and traceable calibration records.
Experience also shows that specifications can be misunderstood. A wider range is not always better. Higher resolution can expose noise instead of useful detail. The ideal surface stress meter should match the material, test method, and working environment. It should also support consistent results between operators and across different days.
Small details matter. Check how the probe contacts the surface. Confirm whether temperature changes affect readings. Ask how often calibration is recommended. Then review the manufacturer’s technical documents, warranty terms, and support response. These checks may feel slow. They prevent expensive mistakes later.
No selection method is perfect. Real samples can behave differently from test standards, and even careful users can overlook drift. That is why independent verification remains valuable. A thoughtful comparison, supported by documented testing, helps turn a promising instrument into a reliable measurement tool.
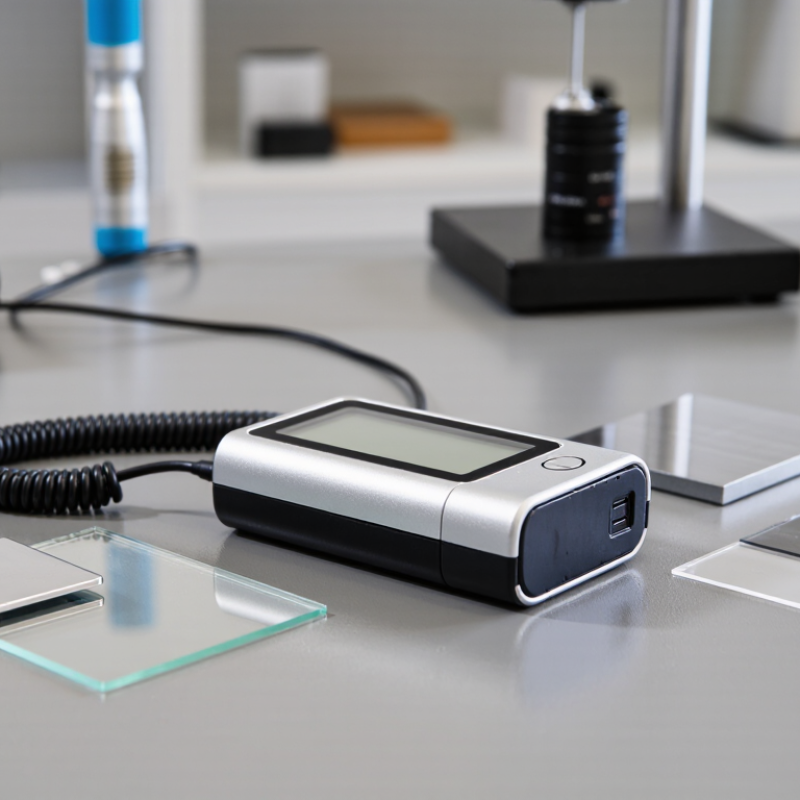
When choosing a surface stress meter, define the measurement goal before comparing specifications. A production line may need a rapid pass/fail reading. A laboratory may require stress mapping across the entire pane. These are different jobs. ASTM C1048 sets a minimum surface compressive stress of 69 MPa for fully tempered architectural glass, while heat-strengthened glass commonly requires 24–52 MPa. Therefore, the meter must cover the expected range and show repeatable results near the acceptance limit.
Surface type matters just as much. Standard optical methods work best on clear, flat glass with known thickness and refractive properties. Low-iron glass, coated glass, curved panels, chemically strengthened glass, and laminated assemblies can change light transmission or measurement geometry. ISO 1288 measurement procedures also show why thickness and test configuration must be controlled when evaluating glass strength. A practical check includes the sample’s thickness, curvature, coating, edge condition, and target stress depth. Do not assume one fixture fits every panel.
Measurement uncertainty deserves attention. A reading of 68 MPa and one of 72 MPa may lead to opposite decisions, although the difference is small. Ask for repeatability data, calibration procedures, and validation against reference samples. The prettiest specification sheet can still hide poor results on coated surfaces. That assumption needs testing. A short trial with real production glass is often more informative than a long comparison table. Cite: ASTM C1048; ISO 1288.
Choosing the right surface stress meter starts with its working range. ASTM E837-20 covers residual stress measurement using the hole-drilling method, but your application may involve thinner coatings, smaller loads, or shallow stress gradients. Select a range that places normal readings near the middle, not at the limit. A device rated from 0 to 1,000 MPa may look versatile, yet it can hide small changes below 20 MPa.
Resolution and accuracy are different. Resolution shows the smallest displayed increment. Accuracy describes closeness to the accepted value. A meter displaying 0.1 MPa is not automatically accurate to 0.1 MPa. NIST Technical Note 1297 recommends evaluating uncertainty through repeatability, calibration, resolution, and environmental effects. Its guidance commonly uses a coverage factor of k=2 for approximately 95% confidence. That matters when comparing two instruments with similar specifications.
Check the complete uncertainty budget. ASTM E837-20 also emphasizes corrections linked to material properties, hole geometry, and strain response. Temperature can quietly shift readings. So can a rough surface. In practical testing, I would repeat each measurement on a reference coupon and record the spread, not only the average. A clean specification can still mislead. I once trusted a narrow resolution figure and overlooked poor repeatability. That was a costly lesson. Choose the meter whose verified uncertainty fits your decision limit, then confirm its calibration through an ISO/IEC 17025-accredited laboratory where possible.
Tip 1: Match the sensor principle to your material. Optical systems suit transparent samples, while electrical designs may work better with conductive films.
Tip 2: Check the contact area carefully. A rough coating can create unstable readings or damage a delicate surface.
Tip 3: Review the sensor’s mechanical range. Brittle layers need gentle loading and controlled movement.
Tip 4: Confirm chemical compatibility before testing. Solvents, acids, oils, and cleaning agents can swell, soften, or corrode sensor components.
Tip 5: Consider temperature control. Even small temperature changes may alter viscosity, surface tension, and measured stress. Keep the sample and sensor near the same temperature.
Small details matter.
Tip 6: Examine how the meter handles different sample sizes and shapes. A sensor designed for flat films may not suit curved parts or porous materials.
Tip 7: Ask for calibration procedures, reference materials, and repeatability data.
In practical lab work, these details often reveal more than headline accuracy. I once focused too heavily on resolution and overlooked fixture stability. The readings looked precise but shifted after each sample change. That experience changed my evaluation process.
Test the complete setup with your actual material, not only with a supplier’s standard sample. Record surface preparation, humidity, temperature, and contact time. A compatible sensor should produce dependable results without forcing the material into an unnatural condition.
Check the calibration certificate and its traceable reference standard. Confirm the calibration date, uncertainty, and recommended interval. Test zero stability before measuring a sample. A drifting zero can make a clean surface look defective. Ask whether the instrument supports repeatability checks under your actual temperature conditions. Review the sensing range and resolution carefully. More sensitivity is not always better.
Examine the software before purchasing. It should display live readings clearly and flag unstable measurements. Look for adjustable sampling rates, automatic averaging, and user access controls. The software should retain calibration history and record changes. A complicated interface can create avoidable operator errors. I once trusted a polished screen too quickly. The exported values lacked essential test settings.
Data-recording features deserve equal attention. Each result should include a timestamp, operator identity, sample number, and measurement location. Confirm that raw readings remain available after averaging. Check whether files can be exported in common formats without losing units. Secure backup options are useful in busy laboratories. Review how the system handles failed tests and repeated measurements. Do not rely only on a screenshot. A saved record should let another technician reproduce the decision. Test the complete workflow with a real sample before installation. That trial may expose missing fields, slow software, or confusing calibration reminders.
A surface stress meter must survive the environment where it will work. Check its housing, sensor protection, and resistance to dust, moisture, vibration, and temperature changes. A clean laboratory and a busy production floor demand different levels of durability. Ask for realistic test data, not vague claims. Small details matter.
I once evaluated a meter that produced excellent readings but had a fragile connector. One accidental pull stopped the inspection. That experience changed my checklist. Examine cable strain relief, screen visibility, battery access, and storage protection. The strongest device is not always the most expensive one. However, weak construction can create repeat purchases and delayed testing.
Support also affects ownership cost. Confirm calibration intervals, repair times, replacement sensor prices, and technical training options. Clear manuals help, but responsive technical guidance can prevent costly measurement errors. Request a service process in writing. It may reveal limitations.
Calculate more than the purchase price. Include calibration, accessories, software, batteries, downtime, and staff training. A lower-priced meter can become expensive after several years. A higher-priced model may reduce interruptions, but only if its support remains dependable. Ask how long spare parts stay available. Review the warranty conditions carefully. Some promises sound reassuring until a fault occurs.
Your measurement records should also remain traceable. Keep calibration certificates and inspection notes. This supports reliable decisions during audits or process reviews. I would still test the meter on your own materials before buying. General specifications cannot predict every surface, and that is where many selection decisions become uncertain.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru