Precision Work Rolls are small in profile but decisive in the mill. They contact the strip directly, influencing thickness, surface finish, and dimensional consistency. The World Steel Association’s World Steel in Figures 2024 reports that global crude steel production reached 1,892.2 million tonnes in 2023. That scale helps explain why roll performance matters across hot- and cold-rolling operations. It does not, by itself, identify the best roll for a particular mill.
The main types are commonly distinguished by material and service: forged-steel rolls, cast-steel rolls, high-speed-steel rolls, and carbide rolls. Each brings different trade-offs in wear resistance, toughness, surface quality, and operating cost. OECD steel-market analyses also examine capacity, trade, and decarbonization pressures—conditions that shape mill investment and maintenance priorities. Still, a report cannot replace operating data from the line. Strip grade, rolling load, coolant practice, and finishing requirements all matter. A detail worth checking.
This guide compares the leading roll types and explains where each may fit. It also considers limitations, not just advertised advantages. Material names can sound definitive. They are not. Roll life and product quality depend on design, heat treatment, grinding, and operating discipline. The right choice is usually specific to the stand and production target. There is no universal winner.
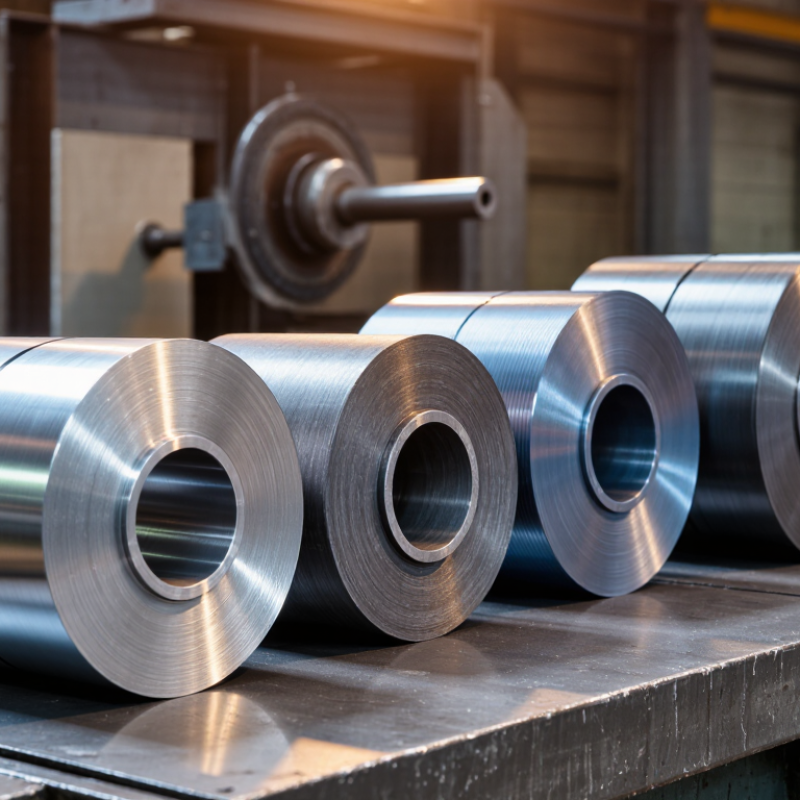
Precision work rolls are classified by mill, material, and duty—not by “precision” alone. In a four-high cold-rolling mill, smaller-diameter work rolls contact the strip directly, while backup rolls resist bending. Sendzimir mills use clustered roll arrangements and very small work rolls for thin, hard materials. The mill layout matters: a roll suitable for one stand may wear unevenly or deflect in another. World Steel Association data put 2023 global crude steel production at about 1.89 billion tonnes, underscoring the scale of rolling operations, though production volume alone does not determine roll choice.
Material selection follows contact pressure, surface finish, and wear demands. Forged steel rolls are common where toughness and resistance to fatigue are critical; high-chromium iron rolls can offer strong wear resistance in suitable applications. Carbide-based rolls may serve demanding finishing duties, but their brittleness and operating conditions need careful review. Hardness figures are meaningful only when the scale, test method, and roll layer are specified. Small detail. It changes comparisons.
Duty classification is just as practical: roughing, intermediate, and finishing work rolls face different loads, temperatures, and surface requirements. A finishing roll may need a highly controlled texture to transfer the required strip finish, while a roughing roll prioritizes durability under heavier reduction. Mill operators typically track wear, roll force, strip defects, and grinding history together. These are useful clues, not a perfect prediction; operating conditions can change faster than a specification sheet.
Cold-rolling work rolls face high contact pressure, repeated thermal changes, and abrasive strip surfaces. Their material affects wear, surface finish, and maintenance intervals. Three common choices are forged steel, high-chromium steel, and high-speed steel (HSS), each suited to different mill conditions.
Forged steel rolls offer toughness and resistance to impact. They can suit demanding stands where load changes are significant, though their wear resistance may be lower than that of harder alloys.
High-chromium rolls contain hard carbides that help resist abrasion and support a consistent strip finish. They are often considered for work that needs a balance of wear life and surface quality. A close look matters.
HSS rolls are designed to retain hardness under heat and resist wear, making them useful in demanding finishing applications. Their performance still depends on roll design, cooling, grinding, and the steel being rolled.
For example, a mill handling hard strip may value HSS wear resistance, while a stand exposed to impact may favor forged steel’s toughness.
No material wins everywhere.
Selection should follow operating data, including rolling force, temperature, surface requirements, and actual campaign life. Shop records can reveal patterns, but they are not perfect: changes in lubrication or grinding practice can blur comparisons.
Hot-strip work rolls face heat, pressure, scale, and repeated contact with moving steel. The main choices are ICDP, high-chromium iron, and high-speed steel (HSS). World Steel Association’s World Steel in Figures 2024 reports roughly 1.89 billion tonnes of crude steel production in 2023. That scale highlights why dependable roll life matters, though production volume alone cannot identify the best roll material.
ICDP rolls combine a hard working layer with a tougher core, making them a common option for finishing stands. High-chromium iron offers strong wear and oxidation resistance, useful where surface condition must remain stable over a campaign. HSS rolls contain hard carbides that help retain wear resistance under demanding hot-rolling conditions. They may extend campaigns, but grinding, cooling, and operating practice still matter. There is no universal winner. A tidy ranking can mislead: stand position, steel grade, and mill settings change the result.
Tips: Match roll material to the stand’s actual wear pattern, not just its nameplate role. Track roughness, wear, and grinding stock between campaigns. Small details matter. And mill data may be imperfect, so check trends across several campaigns before changing specifications.
Special-purpose work rolls refine strip after heavier reduction stages. Their job is not simply to make metal thinner. They influence surface texture, flatness, and the consistency of each pass. Small changes matter. A roll’s diameter, crown, finish, and material must suit the mill and product.
Temper rolls support a light reduction that improves shape and mechanical properties. Operators may use a controlled surface texture to transfer a chosen finish onto the strip. Skin-pass rolls perform a similar light treatment, often helping reduce yield-point markings and improve handling. The distinction can blur in practice, depending on the process and mill terminology. That deserves checking before specifying a roll.
Foil rolls need very smooth, carefully maintained surfaces because tiny marks can show on thin material. Clean handling matters; a trapped particle may leave a visible line. Leveling rolls address flatness rather than appearance alone. Their geometry and alignment help correct edge waves or center buckles as strip passes through the machine. Results depend on incoming material, tension, and setup, so roll selection cannot solve every shape problem. Measurements should guide adjustments, though mills do not always have perfect data.
Roll quality needs more than a polished surface and a hardness number. For steel, copper, and aluminum rolling, Rockwell C hardness provides a quick check of resistance to indentation. ISO 6508-1 defines the HRC method; the commonly used working range is 20–70 HRC. A reading near either end deserves careful interpretation. Surface condition, test location, and curved geometry can affect results. Measure several prepared spots, not just one convenient patch.
Small detail. It matters.
Brinell hardness, reported as HBW, uses a ball indenter and can help assess larger, potentially less uniform areas. ISO 6506-1 specifies the test method. HRC and HBW are different scales, so avoid treating a conversion chart as exact evidence of roll performance.
Surface finish is another key measure: Ra, in micrometres, describes average profile deviation from a mean line. ISO 21920-2 sets profile-texture parameters, while the measurement procedure and filter settings still matter. For example, a roll marked Ra 0.2 µm is not automatically suitable for every product or pass schedule. The target depends on material, lubrication, and the required strip finish.
Slightly imperfect, but important: a single Ra value cannot capture every scratch, waviness pattern, or isolated defect. Record the cutoff, instrument direction, and test locations alongside the result.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru