Why Choose a Vehicle Spray Booth for Your Business?
Why Choose a Vehicle Spray Booth for Your Business?
A Vehicle Spray Booth can turn an ordinary repair bay into a controlled finishing environment. It manages airflow, captures overspray, and reduces dust settling on wet paint. The difference appears clearly on a finished door panel. Fewer particles mean less polishing, rework, and customer complaints.
Industry demand supports this investment. Grand View Research reports continued growth in the global automotive paints and coatings market, driven by vehicle production, refinishing, and stricter finish expectations. MarketsandMarkets also identifies automotive coatings as a major technical market, with performance, durability, and application efficiency shaping purchasing decisions. These reports do not guarantee profit. They show a direction.
A professional booth also supports safer, more repeatable work. OSHA guidance on spray finishing emphasizes ventilation, ignition control, housekeeping, and suitable equipment. NFPA 33 provides widely recognized requirements for spray application operations. Together, these references highlight an important point: booth selection involves more than size and price.
A booth is not a magic box.
Your business still needs trained technicians, filter maintenance, airflow checks, and documented cleaning routines. Energy consumption deserves attention too. A poorly selected booth may create high operating costs, especially during long curing cycles. That weakness is easy to overlook.
The strongest choice matches your workload, vehicle dimensions, paint system, available space, and local compliance responsibilities. It should also support future growth, not only today’s repair orders. For many workshops, that balance makes a Vehicle Spray Booth a practical investment in finish quality, workflow control, and professional credibility.
Define Vehicle Spray Booths by Function, Design, and Automotive Use
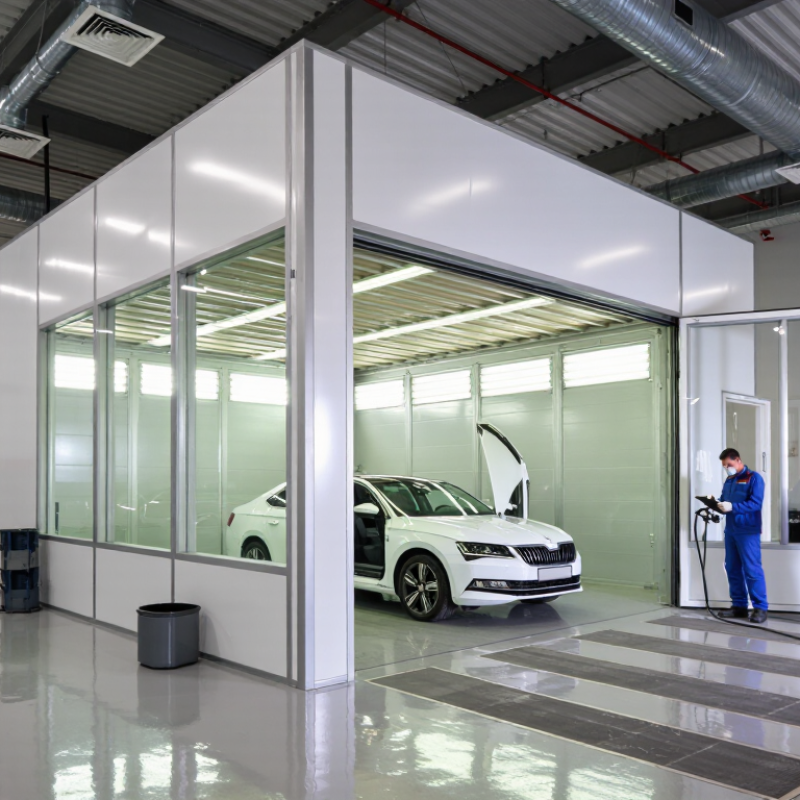
Choosing a vehicle spray booth means examining its function, design, and automotive purpose. It is not simply an enclosed room for applying paint. A well-designed booth controls airflow, filters particles, manages lighting, and supports consistent curing conditions.
By function, booths may use downdraft, crossdraft, or side-draft airflow. Downdraft systems pull overspray toward floor-level filters, helping protect freshly coated panels. Crossdraft designs move air horizontally and may suit specific workshop layouts.
The correct choice depends on vehicle size, coating volume, floor space, and maintenance capacity. Airflow must remain stable. Uneven pressure can create dust marks, dry spray, or inconsistent gloss.
Design affects daily work. Clear visibility, sealed doors, durable filters, and accessible service panels reduce interruptions. Strong lighting reveals sanding scratches and subtle surface defects before spraying.
In automotive use, a booth should accommodate more than full-size cars. Vans, bumpers, doors, and small repair parts may require different working arrangements.
From practical workshop experience, clean preparation often matters as much as booth performance. That lesson is easy to overlook.
The process is not flawless. Filters load faster than expected, and careless cleaning can undermine a good airflow system.
Regular inspections, documented maintenance, and operator training support reliable results. Manufacturer guidance and recognized safety practices should direct installation, ventilation, and electrical planning.
Compare Booth Types for Finish Quality, Safety, and Production Capacity
Why Choose a Vehicle Spray Booth for Your Business?
Compare Booth Types for Finish Quality, Safety, and Production Capacity
A vehicle spray booth controls airflow, dust, lighting, and overspray around each job. These factors directly affect finish quality. Downdraft booths pull contaminated air downward through the floor. They usually produce the cleanest surface, especially on large panels and dark colors. Crossdraft booths move air from the front toward the rear. They cost less, but particles can travel across freshly coated surfaces. Side-draft designs offer a practical middle ground. They can suit smaller facilities with limited installation space.
Safety depends on more than the booth style. A properly sized exhaust system removes vapors and maintains stable airflow. Suitable filters capture overspray before it reaches fans or exhaust paths. Clear gauges help technicians notice pressure changes early. Regular filter replacement matters. Small maintenance delays can become serious quality and safety problems.
Production capacity changes the decision. A downdraft booth may support premium refinishing, but installation and operating costs can be higher. A crossdraft booth may increase flexibility for moderate workloads. Curing capability also matters when several vehicles move through the shop daily. Faster curing can reduce waiting time, but excessive heat may damage sensitive materials. No booth is perfect. In practical evaluations, businesses sometimes focus on purchase price and overlook cleaning time, energy use, or technician movement. Measure real workflow before choosing. A booth that looks efficient on paper may slow production on the floor.
Control Overspray and VOCs with 98%-Efficient Particulate Filtration
Why Choose a Vehicle Spray Booth for Your Business?
A vehicle spray booth gives overspray a controlled path instead of letting paint mist settle on floors, lamps, and nearby vehicles. A 98%-efficient particulate filtration stage can capture most airborne paint particles under its tested conditions. However, efficiency depends on particle size, airflow, filter loading, and seal quality.
The U.S. EPA’s AP-42 guidance identifies paint application and solvent evaporation as separate emission sources. This distinction matters. Particulate filters capture droplets, but they do not automatically remove VOCs.
VOCs require proper ventilation and, where designed, an additional adsorption or exhaust-treatment stage. OSHA and NIOSH publications repeatedly emphasize exposure control through engineering controls, not personal protection alone.
In daily operation, a pressure gauge can reveal rising resistance before airflow becomes visibly weak. A booth also protects finish quality. Dust on a fresh clear coat is expensive to repair.
Still, the 98% figure is not magic. A damaged gasket, overloaded filter, or poorly balanced fan can reduce real-world performance.
Tips:
Record filter changes, airflow readings, and coating usage. Check the manufacturer’s test conditions before comparing efficiency claims. Keep doors closed during spraying. Train operators to avoid excessive trigger time and unstable spray distance. EPA solvent-emission guidance can help estimate material losses, but shop conditions vary, so your own records may expose problems that a brochure misses.
Estimate ROI Through Throughput, Rework Reduction, and Energy Demand
Why Choose a Vehicle Spray Booth for Your Business?
A vehicle spray booth can improve ROI through faster curing, cleaner finishes, and fewer repeat jobs. Throughput matters when each idle hour delays delivery. For example, adding one completed vehicle daily can create measurable monthly capacity. The calculation should include labor, coating materials, booth utilization, and average gross profit. Do not assume every added slot becomes a sale. Local demand may be the weaker link.
Rework reduction is often less visible, but equally important. Dust, uneven color, and poor solvent control can create extra sanding and respraying. A controlled booth environment helps technicians repeat the same process more reliably. Industry quality studies commonly place automotive refinish rework near 5–15%, depending on process discipline and shop conditions. Track your own rate for eight weeks before investing. Experience beats a perfect spreadsheet. Record labor hours, material waste, and delivery delays.
Tips: Measure booth cycles, fan runtime, and electricity separately. The U.S. Department of Energy explains that fan power follows the affinity-law relationship, so reducing speed by 20% can cut theoretical power demand by about 49%. Real savings will be lower if airflow becomes inadequate. The DOE also reports that compressed-air leaks can waste 20–30% of system output. Inspect hoses, regulators, and doors weekly. Review results monthly, then adjust production targets when the evidence disagrees with your original forecast.