Why Choose an Assembly Line Trolley for Your Factory?
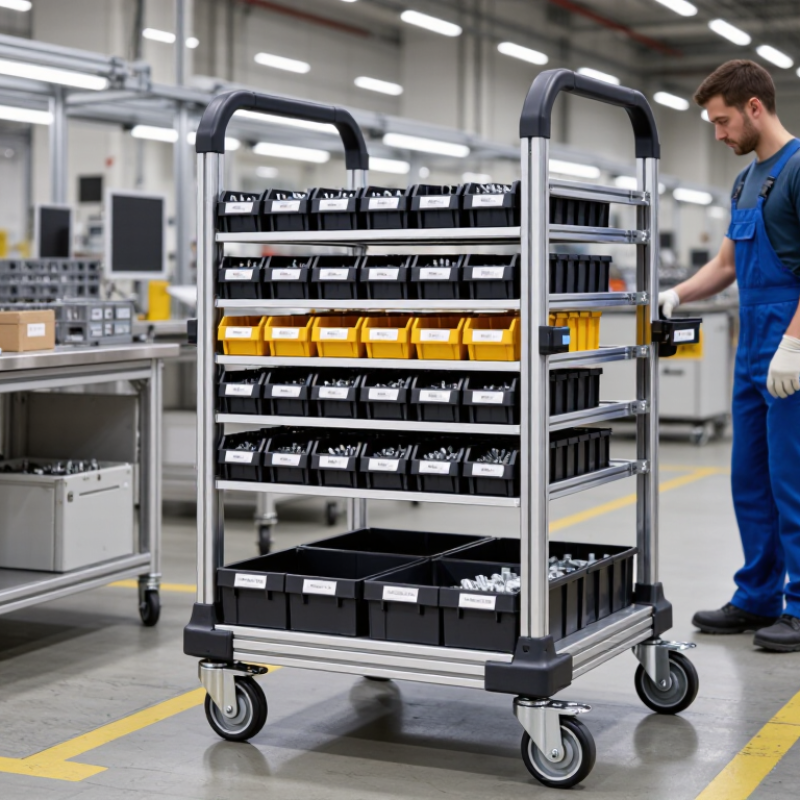
In a busy factory, small delays can spread quickly along a production line. An operator may walk several extra steps to collect fasteners, fittings, or boxed components. Repeated across a shift, those trips take time away from assembly and create unnecessary movement. An Assembly Line Trolley can keep frequently used materials close to the workstation, where they are easier to see and reach. Small details matter. Shelf height, handle position, and wheel quality all affect how comfortably staff can move and load the trolley. A well-matched design can support a steadier supply of parts and reduce clutter around benches and walkways.
The right trolley depends on the work, not just the available floor space. Consider the load’s weight, size, and shape, along with how often materials need replenishing. A narrow trolley may fit between stations but offer too little capacity; a larger one may obstruct turning areas. Check that its wheels roll smoothly on the factory floor and that shelves keep items stable during movement. Still, a trolley is not a cure-all. Poorly planned routes or overloaded shelves can create new handling problems. Before choosing a model, observe a typical shift, note where parts are stored, and ask operators what slows them down. Their practical feedback can reveal needs a product specification alone may miss. The best choice is the one that fits the daily workflow safely and reliably, even if that means reconsidering an initial preference.
Assembly Line Trolleys in Context: Material Handling’s 20–50% Cost Share
Why Choose an Assembly Line Trolley for Your Factory?
Material handling can account for roughly 20–50% of manufacturing costs, depending on the process and how the figure is measured. That share includes more than moving parts. It may involve operator time, repeated trips, waiting, excess staging, and damage from awkward transfers. Small delays add up. An assembly line trolley can keep tools and components close to the work area, helping operators spend less time walking or searching. But a trolley alone will not solve a poorly planned workflow. Its shelves, load capacity, and turning radius should match the parts, aisle width, and production sequence. I have seen tidy-looking setups still create bottlenecks when carts arrive at the wrong time.
Tips: Track walking time and replenishment delays before changing the layout. Test a trolley on one line first. Check wheel movement, shelf height, and access to frequently used parts. Review the results with operators; they often notice practical issues managers miss.
The best measure is not simply how many trolleys a factory buys. Compare handling time, waiting, and product damage before and after a controlled trial. Keep the comparison consistent across shifts. A trolley may reduce unnecessary movement, though crowded aisles or oversized loads can erase the gain. Revisit the setup as products and work patterns change.
How Trolleys Support Line-Side Supply and Lean One-Piece Flow
An assembly line trolley brings parts close to the point of use, where operators need them. Trays can follow the build sequence, keeping fasteners, fittings, and small components within easy reach. A clearly marked shelf also makes missing items easier to spot before work stalls. Small details matter.
For one-piece flow, the trolley should carry only what the next task requires. A compact load reduces searching and limits clutter around the workstation. When a container empties, a simple card or empty-bin signal can prompt replenishment from the supermarket area. A steady delivery route helps prevent both shortages and excess stock. Keep the path clear.
Trolley design needs to match the actual line, not an idealized drawing. Check aisle width, turning space, handle height, and the weight of a full load during a real shift. Wheels that roll smoothly over floor joints can reduce effort, but they still need suitable brakes and regular inspection. That is not automatic. Overloading or poorly arranged parts can create new delays, so teams should adjust shelf positions and delivery frequency after observing the work. One useful test is whether an operator can take the next part without stepping away from the station.
Ergonomic Push-and-Pull Design Under ISO 11228-2
An assembly-line trolley can make parts easier to move between workstations, but its ergonomic value depends on how people push and pull it. ISO 11228-2 provides a framework for assessing these tasks. It considers factors such as the force required, travel distance, frequency, and working posture. A trolley alone does not guarantee a low-risk task.
Small details matter. Handle height should suit the workers using it, while suitable casters can help the trolley roll smoothly over ordinary floor joints. Check how it starts, turns, and stops when carrying a realistic load. A short trial along the actual route can reveal awkward reaches or sudden effort that a showroom test may miss. Not every shift is identical.
Keep loads stable and within clear sightlines, and avoid overloading the trolley to save trips. Floor condition, tight corners, and uneven loading can all increase push-and-pull effort. Record operator feedback and review the setup when the route or workload changes. The assessment may not catch every difficult moment, so practical observation still matters. A well-chosen trolley supports safer material handling when its design and use are matched to the task.
Measuring Results Through Travel Distance, Replenishment Time, and WIP
An assembly line trolley is useful when it improves the movement of parts, not merely because it looks organized. Measure the distance an operator walks during a normal shift. A simple floor map and a few timed observations can reveal repeated trips between storage, workstations, and the line. Shorter routes may reduce wasted motion, though crowded aisles can erase that gain.
Replenishment time matters just as much. Record the interval from a workstation’s request to the arrival of the correct parts. A trolley with clearly separated bins can make shortages easier to spot and deliveries more predictable. Keep frequently used items within easy reach. Small details count. Still, a trolley will not fix unclear signals or poor restocking schedules; those problems need attention too.
Work-in-process inventory offers another practical measure. Count the parts waiting between operations before and after introducing a trolley system, using comparable production periods. Less WIP can mean fewer blocked stations and less material sitting untouched. But lower numbers are not automatically better if workers face frequent stockouts. Review the figures with operators, and note unusual shifts or product changes. The first results may be messy, and that is worth acknowledging. Real improvement comes from checking the measures repeatedly and adjusting routes, bin quantities, and delivery timing.