When procurement teams source components across borders, material choice affects cost, durability, and delivery confidence. Welded Metal offers a practical solution for frames, brackets, enclosures, platforms, and industrial assemblies. Its strength comes from joining prepared sections into a stable structure. This approach can reduce part counts and simplify installation at the customer’s site. It also supports flexible designs when product volumes or dimensions change.
Reliable sourcing depends on more than a competitive quotation. Experienced buyers review steel or aluminum grades, weld sizes, joint locations, surface treatments, and dimensional tolerances. They ask suppliers for welding procedure records, inspection reports, material certificates, and clear sample approvals. A qualified factory should explain how it controls distortion, porosity, spatter, and corrosion protection. Details matter. On-site audits, video inspections, and independent testing can strengthen confidence before full production begins. Packaging also deserves attention, especially when welded frames travel by sea and face moisture, vibration, and repeated handling.
Welded Metal is not automatically the best choice for every application. Complex joints may require extra fixtures, skilled labor, or secondary machining. Poor drawings can create expensive misunderstandings across languages and time zones. That risk is real. Even strong suppliers can miss a tolerance when feedback arrives late. A thoughtful global sourcing strategy therefore balances price with engineering support, traceability, lead time, and after-sales responsibility. The result is not simply a lower purchase cost. It is a component that arrives ready to perform, with fewer surprises between the factory floor and the final installation.
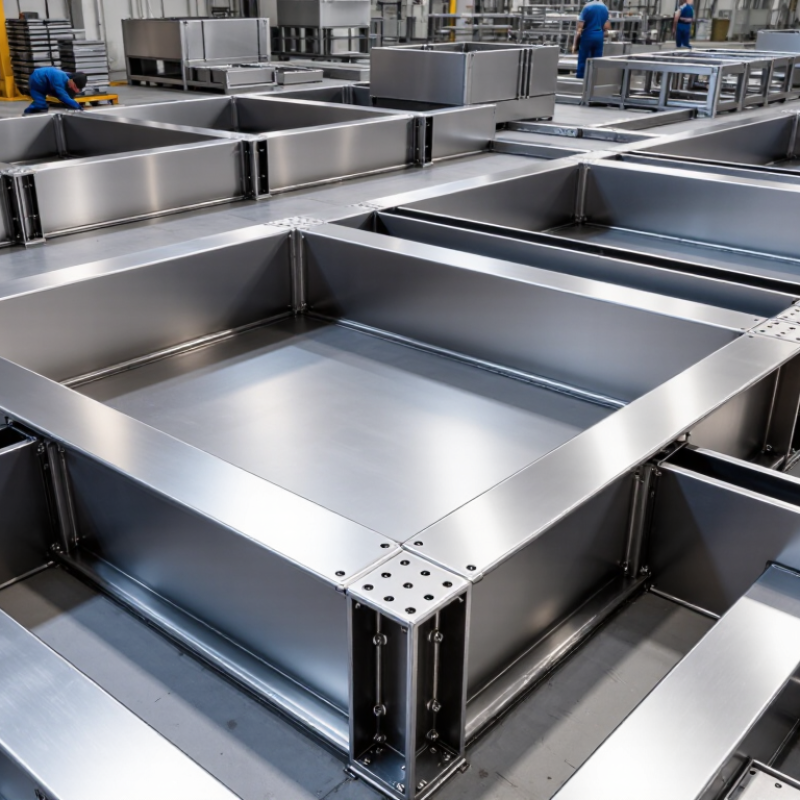
Welded metal is made by joining separate metal pieces with heat, pressure, or both. The process can use electric arcs, resistance, laser energy, or controlled gas flames. The joint may also need filler metal to close gaps and improve strength.
Manufacturers use welded metal for frames, brackets, tanks, pipes, platforms, and machine housings. A steel frame, for example, may combine cut tubes with small reinforced plates. Aluminum welds can reduce weight in transport equipment. Stainless steel helps resist corrosion in clean production areas. The correct method depends on metal type, thickness, joint design, and expected load.
Global sourcing requires more than comparing unit prices. Buyers should review welding procedures, operator qualifications, material certificates, and inspection records. Visual checks can find cracks, uneven beads, burn-through, or poor alignment. Some suppliers also use ultrasonic, radiographic, or magnetic testing when risk levels justify it. Requirements should be written clearly, including tolerances, surface treatment, packaging, and traceability.
A polished weld is not automatically a strong weld. That assumption causes expensive rework. In practical inspections, hidden porosity or distortion can matter more than appearance. Drawings may also overlook transport vibration or assembly access. Sample testing, production-stage communication, and independent checks make sourcing decisions more reliable. Mistakes still happen, especially when specifications cross languages or measurement systems. Clear photographs and shared inspection points can reduce that gap.
Welded metal gives global sourcing teams a practical balance of strength, flexibility, and production scale. According to the World Steel Association’s 2024 World Steel in Figures, global crude steel output reached about 1.89 billion tonnes in 2023. That industrial capacity supports reliable access to common grades, fabrication equipment, and skilled welding labor across many regions. Welded assemblies can also reduce machining time and material waste compared with parts carved from solid blocks. A supplier can produce frames, brackets, tanks, and structural components from standard sheets or tubes. Design changes are usually manageable. A revised joint may require a new fixture, not an entirely new production system.
The financial benefit is real, but it is not automatic. Welding quality depends on joint design, operator training, inspection, and controlled heat input. ISO 3834 provides quality requirements for fusion welding, while independent inspection can verify dimensions, penetration, and surface defects. The International Energy Agency reports that iron and steel production creates roughly 7–9% of global energy-related carbon dioxide emissions. Therefore, responsible sourcing should examine electricity sources, scrap content, transport distance, and coating processes. A low-cost quotation can become expensive after rework or delayed shipping. I would not select a supplier from price alone. Trial batches, weld procedure records, material certificates, and clear acceptance criteria offer stronger protection. Some assumptions still fail in practice. A simple-looking weld can distort a panel, weaken a corner, or complicate final assembly.
When manufacturers compare global sourcing options, welded metal often looks attractive because it reduces assembly steps. A skilled supplier can join cut tubes, plates, and brackets into one ready-to-use frame. This saves fasteners, handling time, and warehouse space. In real production, the savings become clearer on repeat orders. Fixtures can be adjusted, welding sequences documented, and inspection points standardized. A frame that leaves the factory assembled also reaches the customer with fewer loose parts. That matters.
Cost control depends on design decisions made before production begins. Consistent joint geometry supports robotic or semi-automatic welding, while accessible seams reduce rework. Specifying suitable steel thickness can lower material use without weakening the structure. However, thinner is not always better. Engineers should review load paths, heat distortion, corrosion exposure, and expected service life. Samples, weld maps, dimensional checks, and visual inspections create traceable evidence. For critical assemblies, non-destructive testing may be appropriate. These practices cost something, but uncontrolled defects cost more.
Global sourcing adds freight, communication, and compliance risks. Clear drawings should define tolerances, weld sizes, surface treatment, packaging, and acceptance criteria. A pilot batch can reveal warping or awkward packing before volume production. In one production review, a team assumed a simple bracket would pack efficiently. Its protruding welds required extra protection. The lesson was practical: unit price alone is incomplete. Reliable sourcing balances labor, materials, inspection, transport, and correction costs. Supplier audits and documented process controls provide useful confidence, though they never replace thoughtful engineering review.
Practical production and sourcing factors that influence the cost, scalability, and performance of welded metal assemblies.
| Cost and Sourcing Dimension | Typical Welded-Metal Condition | How It Supports Cost-Effective Production | Sourcing Consideration |
|---|---|---|---|
| Material utilization | Often based on sheet, plate, tube, or structural sections cut to near-net shapes. | Near-net cutting can reduce excess machining and decrease material waste compared with manufacturing a complete part from a solid block. | Request nesting layouts, cut-part yield data, and the proposed material grade before approving production. |
| Part consolidation | Multiple prepared components can be joined into one structural assembly. | Combining parts may reduce the number of purchased components, fasteners, and assembly operations. | Check weld accessibility, distortion control, inspection requirements, and repair procedures during design review. |
| Machining requirements | Welding creates the primary structure; machining is commonly limited to critical interfaces, bores, or mounting surfaces. | Reducing full-part machining can lower machine time, tooling consumption, and material removal costs. | Define dimensional tolerances carefully; unnecessarily tight tolerances can offset the savings from fabrication. |
| Production scalability | Manual, semi-automated, robotic, and fixture-assisted welding can be selected according to volume and geometry. | The process can scale from prototypes and low-volume orders to repetitive production without changing the basic joining method. | Compare fixture investment, operator qualifications, takt time, and expected annual volume. |
| Tooling investment | Many welded assemblies require production fixtures rather than permanent hard tooling. | Lower tooling complexity can improve the economics of product launches, engineering changes, and moderate-volume orders. | Ask whether fixtures are included in the quotation and how future revisions will affect tooling charges. |
| Lead-time drivers | Lead time depends on material availability, cutting, forming, fit-up, welding, finishing, inspection, and logistics. | A coordinated fabrication route can eliminate separate supplier handoffs for cutting, forming, and joining. | Use a stage-based schedule and confirm capacity for welding, surface treatment, and final inspection. |
| Joint strength and durability | A properly designed and executed weld can provide a permanent load-bearing connection. | Permanent joints can reduce reliance on separate brackets and mechanical fasteners in suitable applications. | Specify joint design, weld size, material compatibility, acceptance criteria, and required non-destructive testing. |
| Quality consistency | Repeatability improves with qualified welding procedures, controlled fixtures, trained personnel, and documented inspection. | Process control reduces rework, scrap, field failures, and unexpected quality-related costs. | Request welding procedure specifications, welder qualification records, inspection plans, and traceability documents. |
| Surface finishing | Assemblies may receive cleaning, grinding, blasting, painting, powder coating, plating, or other specified protection. | Finishing can be integrated into the fabrication route, reducing coordination between separate vendors. | Confirm weld spatter limits, edge preparation, coating thickness, corrosion category, and masking requirements. |
| Global logistics | Welded assemblies can be shipped as completed units, subassemblies, or flat-packed kits when the design permits. | Shipping a consolidated assembly may reduce local labor and the number of inbound component shipments. | Evaluate package dimensions, gross weight, container utilization, corrosion protection, and import classification. |
| Total landed cost | The final cost includes material, fabrication, finishing, inspection, packaging, freight, duties, and quality-related risk. | A lower piece price is valuable only when it remains favorable after logistics, compliance, rework, and warranty exposure are included. | Compare suppliers using the same Incoterm, specifications, inspection scope, packaging standard, and delivery assumptions. |
Why Choose Welded Metal for Global Sourcing?
Quality, Standards, and Supplier Evaluation
Welded metal suits global sourcing when suppliers can prove process control. The World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023. That scale creates choice, but it also creates uneven quality. A reliable supplier should provide material certificates, heat-number traceability, approved welding procedures, and dimensional inspection records. Small gaps can become expensive problems.
Standards create a common technical language. ISO 3834 defines quality requirements for fusion welding. ISO 15614 supports welding procedure qualification, while ISO 9606 addresses welder qualification. The ISO Survey 2023 recorded more than 1.26 million ISO 9001 certificates worldwide. Certification helps, but it does not replace evidence from the actual workshop. Ask for sample inspection reports, calibration records, non-destructive testing methods, and corrective-action history.
Walk the production route, even through a documented remote audit. Watch how steel enters storage, how joints are prepared, and how finished frames are protected. Check weld appearance, penetration requirements, distortion control, and packing conditions. Request records linked to each batch. This detail matters during customs checks and field installation. Supplier evaluation is rarely perfect. A polished audit can still miss rushed shifts or weak subcontractor control. Independent testing may be worthwhile for critical parts. Cheap quotes often hide inspection, rework, or freight risks. Keep questioning the process.
Why Choose Welded Metal for Global Sourcing?
Global Sourcing Risks and Best Practices
Welded metal can reduce part counts, tooling costs, and assembly time. In global sourcing, however, a low quotation may hide serious production risks. Different suppliers may interpret the same drawing differently. A two-millimeter gap can affect fit, strength, and finishing quality.
I have seen sourcing projects fail because material grades were confirmed only by email. Require mill certificates, heat numbers, and clear weld specifications before production starts. The drawing should define tolerances, surface treatment, inspection points, and the required welding standard. A weld map helps production teams locate critical joints. Sample approval is useful, but it cannot replace process control.
Small details matter. Ask for welding procedure records and operator qualifications. Use staged inspections during cutting, fit-up, welding, and final measurement. Independent inspection can identify undercut, porosity, distortion, or missing welds before shipment. Keep photos, test reports, packing records, and revision histories in one shared file. Traceability protects both sides when questions arise.
Do not assume visual inspection finds hidden defects. It often does not. Non-destructive testing may be necessary for load-bearing components. Over-specifying every requirement can also raise costs without improving performance. I still consider this a difficult balance. The safest sourcing plan leaves room for technical review, realistic lead times, and one controlled production change at a time.
Global Sourcing Risks and Best Practices
The 2023 World Bank Logistics Performance Index scores logistics capability from 1 to 5. Higher scores generally indicate stronger customs, infrastructure, shipment reliability, tracking, and delivery performance. For welded-metal sourcing, buyers should combine logistics data with qualified supplier audits, welding procedure qualification, material traceability, dimensional inspection, and pre-shipment quality checks.
Source: World Bank, Logistics Performance Index 2023. Scores shown are national logistics performance scores and are not company or brand ratings.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru