For global buyers, Cnc Machining Metal is more than a production method. It is a practical route to accurate, repeatable, and scalable metal components. A milled aluminum housing can leave the shop with clean bores, sharp edges, and tolerances measured in microns. That consistency matters when parts travel from a supplier in Asia to an assembly line in Europe or North America.
Peter Zelinski, a long-time manufacturing journalist and editor, has stated, “The machine tool is the foundation of manufacturing.” His observation explains why CNC capability remains central to modern sourcing. Computer-controlled equipment reduces manual variation and supports complex designs. It can also process aluminum, stainless steel, brass, titanium, and engineering alloys. Buyers can request inspection reports, material certificates, surface-finish data, and first-article samples before approving production. These documents make supplier evaluation more reliable.
Cost is another reason global companies choose Cnc Machining Metal. Digital drawings can move quickly between engineering teams and factories. Tool changes, batch sizes, and cycle times can be reviewed before production begins. Still, lower pricing does not always mean better value. I have seen attractive quotations become expensive after rework, unclear tolerances, or weak packaging caused delays. That is an uncomfortable point, but it deserves attention. Buyers should compare process control, communication, inspection equipment, and delivery records alongside price. Certification claims also require verification. A careful sourcing decision combines technical evidence with real manufacturing experience.
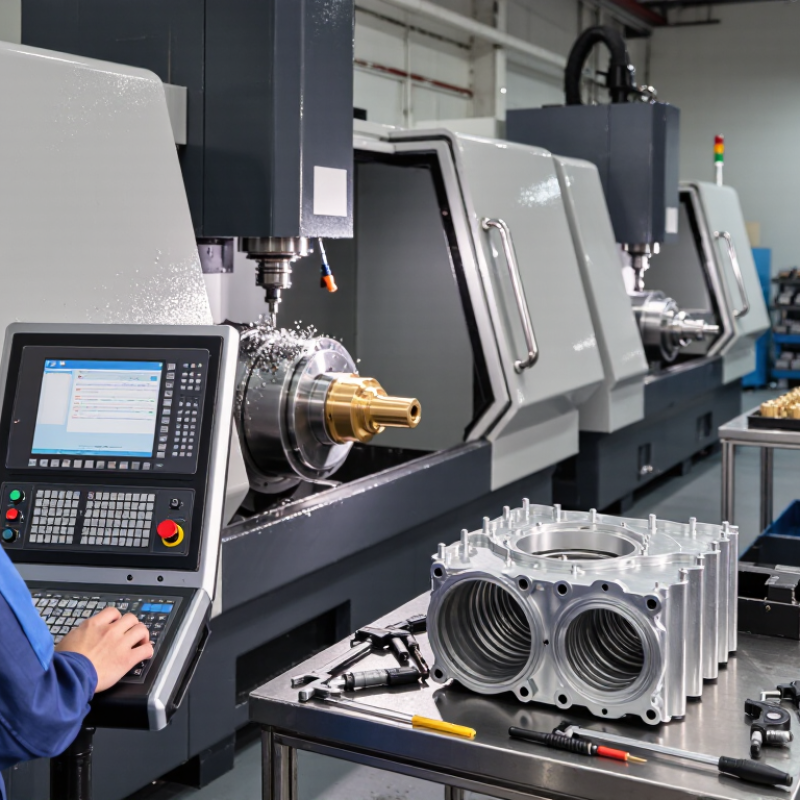
CNC metal machining gives global buyers a practical route to tight, repeatable dimensions. Under suitable conditions, experienced machinists can hold tolerances down to ±0.01 mm on selected features. That level matters when a bearing bore, sealing face, or threaded connection must fit without excessive play. A small aluminum housing, for example, may require a controlled bore and flat mounting surface. The machine follows digital coordinates, while calibrated tools remove material in measured passes.
Precision does not come from the machine alone. Material stability, tool wear, temperature, fixturing, and cutting strategy all influence the final result. A ten-degree temperature change can affect metal dimensions, especially on larger parts. Reliable suppliers verify critical features with micrometers, height gauges, or coordinate measuring equipment. They should also provide inspection records linked to drawing requirements. Ask for that evidence.
±0.01 mm is not magic. It is a manufacturing target with conditions. Very small internal corners, deep cavities, and thin walls can challenge consistency. Some designs need wider tolerances to control cost and reduce distortion. This is where engineering review becomes valuable. A first design may look precise but still be difficult to inspect or machine. Revising datum points, wall thickness, or tolerance zones can improve reliability. Small details decide whether parts assemble smoothly across repeated orders.
CNC machining metal gives global buyers a practical balance of accuracy, strength, and repeatability. Yet quality depends on more than a precise machine. ISO 2768 helps define general tolerances when drawings do not specify every dimension. This creates a shared language for suppliers, inspectors, and purchasing teams. A machined housing may look correct, but a two-millimeter tolerance difference can affect assembly.
THAT GAP MATTERS
ASTM standards add material and testing requirements that support consistent performance across borders. They can define alloy composition, hardness, tensile strength, or inspection methods. Buyers should confirm the exact ASTM specification, not simply request “ASTM material.” The wrong grade may still machine smoothly while failing under heat, pressure, or repeated loading.
ISO 9001 shapes the production system behind the part. It encourages controlled drawings, traceable records, calibrated measuring tools, and corrective action when defects appear. In practice, an operator may check a shaft with a micrometer, record the result, and isolate parts from the same batch if the diameter drifts. Small details matter. However, certification alone cannot guarantee perfect components. Engineers must still review datums, surface finishes, tolerances, and real operating conditions. I have seen drawings follow common standards yet leave an important fit unclear. That uncertainty deserves a question before cutting metal, not an assumption after delivery.
For global buyers, CNC machining becomes more valuable when complex parts demand controlled accuracy. A 3-axis machine moves along X, Y, and Z, making it suitable for plates, blocks, and open surfaces. However, deep cavities often require several setups. Each repositioning can introduce alignment errors, clamping marks, and dimensional variation.
A 4-axis machine adds rotary movement. It can machine multiple sides with fewer interruptions. A 5-axis machine moves the cutter and workpiece simultaneously, helping maintain a consistent tool angle across curved surfaces. This reduces repositioning and improves access to undercuts, impellers, medical housings, and aerospace brackets. The result is often tighter feature alignment and smoother finishes. Small details matter.
The 2024 Deloitte Smart Manufacturing and Operations Survey reported that 86% of manufacturers consider smart manufacturing important to competitiveness. Multi-axis machining supports that direction by combining physical precision with digital toolpath control. Yet axis count alone does not guarantee accuracy. Thermal growth, spindle condition, fixture rigidity, cutting-force changes, and calibration still influence the final part. ISO 230-2 testing helps evaluate positioning accuracy and repeatability, while in-process probing can detect deviations before inspection.
In practical production, a 5-axis setup may reduce handling, but it can also demand stronger programming skills and more disciplined verification. That trade-off is easy to underestimate. Buyers should review tolerance reports, material data, inspection methods, and machine calibration records before comparing quotations. A cheaper setup can become expensive after repeated rework.
For global buyers, CNC machining metal offers repeatable accuracy, strong parts, and flexible production volumes. In practical projects, design for manufacturing (DFM) often determines delivery speed more than machine capacity. A manufacturability review checks wall thickness, hole depth, tool access, tolerances, and material selection before cutting begins. Clear designs reduce programming changes, quotation questions, and avoidable rework. With a production-ready model, many standard CNC metal orders can move from approval to shipment within 3–10 business days. The exact timing still depends on quantity, inspection needs, surface finishing, and material availability.
Tips: Keep internal corners compatible with standard tools. Avoid unnecessarily tight tolerances. Add clear datum references and specify critical surfaces. A simple drawing can prevent several emails. Provide the 3D model, 2D drawing, material grade, finish, and required quantity together. This helps engineers review the part without guessing.
I have seen small design details create large delays. A deep pocket may require special tooling. A thin aluminum wall may deform during clamping. These issues are not always obvious on a screen. Even experienced teams can miss one. That is why an early DFM discussion is valuable.
Engineers may suggest wider radii, fewer setups, or a different machining sequence. Those changes can reduce risk without changing the part’s function. Still, DFM is not magic. Complex geometries, first-article inspections, and international shipping can extend the schedule. Reliable suppliers should explain those limits clearly, not promise every project in the same timeframe.
For global buyers, CNC-machined metal is only useful when compliance survives the supply chain. RoHS restricts ten hazardous substances in electrical and electronic products, including lead, mercury, and cadmium. The European Commission treats these as substance-level controls, not general quality claims. That distinction matters. A machined aluminum housing may look clean, yet its plating, paint, or residue can change the assessment. Buyers should request material declarations, coating details, and traceable test records before production approval.
REACH creates broader chemical-management duties in Europe, including communication requirements for substances of very high concern. The European Chemicals Agency updates its Candidate List as scientific evidence and priorities change. An old declaration is not automatically current. It may be incomplete. Global E-waste Monitor 2024 reports 62 million tonnes generated in 2022; only 22.3% was formally collected and recycled. This gives compliance a physical meaning. Buyers should check alloys, surface treatments, lubricants, packaging, and supplier change controls.
ASTM compliance supports consistency, but ASTM is not universal legal approval. A drawing should name the required material and test standard, such as ASTM E8/E8M for tension testing. Inspection reports should connect heat numbers, dimensions, hardness, and results to each shipment. A certificate without batch traceability is weak evidence. Suppliers sometimes copy declarations between similar parts. Independent verification can expose a wrong alloy, unreported coating, or missing revision. That missing revision often appears after shipment.
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
1 Hayotsrim Street
Nahariya 22311
Israel
Phone: +972 (0)4 9855 121/ 111/ 176
Fax: +972 (0)4 9855 175
Email: sale@dialoguetoolkit.com
Url: www.egmo.co.il
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Distributor in Belgium
Avenue Lavoisier 18B
1300 Wavre
Belgium
Phone: +32(0)471 93 43 12
Email: sale@dialoguetoolkit.com
Url: www.cameco-tubings.be
Distributor in Belgium Flanders
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Sklarska 70
435 42Litvinov
Czech Republic
Phone: +420 602 110 208
Email: sale@dialoguetoolkit.com
Url: www.hacomost.cz
Rusthollarinkatu 8
Espoo FIN-02270
Finland
Phone: +358 (0) 106137100
Fax: +358 (0) 106137701
Email: sale@dialoguetoolkit.com
Url: www.avs-yhtiot.fi
ZI du Val d’Argent
11 rue Guy Moquet
95100 Argenteuil
France
Phone: +33 1 30 25 94 20
Fax: +33 1 30 25 94 59
Email: sale@dialoguetoolkit.com
Url: defa-inox.fr
An der Autobahn 15
Oyten D-28876
Germany
Phone: +49 – 4207 – 69 94 – 0
Fax: +49 – 4207 – 69 94 – 40
Email: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Skouze 14
Piraeus 18536
Greece
Phone: +30 (0)210-4530240
Email: sale@dialoguetoolkit.com
Url: www.agv.gr
Via Novara 10 / B-C
20013 Magenta
Milano
Italy
Phone: +39 02 97298663
Fax: +39 02 97291855
Email: sale@dialoguetoolkit.com
Url: www.indra.it
Distributor for Lithuania, Estonia & Latvia
Serveces g. 2-27
02121 Vilnius
Lithuania
Phone: +370 (5) 210 22 74
Fax: 370 (5) 210 22 75
Email: sale@dialoguetoolkit.com
Url: tekknow.lt
Distributor for Israel, Moldova, Kosovo, Iceland, Hungary, Slovenia, Romania, Bulgaria & Malta
Buitenvaart 1411
Hoogeveen 7905 SJ
The Netherlands
Phone: +31(0)528 234 084
Fax: +31(0)528 234 084
Email: sale@dialoguetoolkit.com
Url: www.www.dialoguetoolkit.com
Bijsterhuizen 2152
6604 LG Wijchen
the Netherlands
Phone: +31 (0)24 648 93 80
E-mail: sale@dialoguetoolkit.com
Url: www.pdgastechnology.nl
Steenspil 8
4661 TZ Halsteren
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Energieweg 14
4691SG Tholen
The Netherlands
Phone: +31(0)85 0074200
E-mail: sale@dialoguetoolkit.com
Url: www.bergen-ip.eu
Strandgata 15A
4307 Sandnes
Phone: +47 91135785
Email: sale@dialoguetoolkit.com
Url: hydraserv.no
ul. Zalogowa 17
Gdansk 80-557
Poland
Phone: +48 58 522 03 80, -81
Fax: +48 58 342 20 10
Email: sale@dialoguetoolkit.com
Url: www.verdigroup.pl
Estrada Nacional 10
Centro Empresarial SADO
Internacional Armazem C 19
2910-809 Setúbal
Portugal
Phone: +351 919 582643
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Serbia, Croatia, Bosnia & Herzegovina, Montenegro, North Macedonia & Albania
Cara Dusana 205A
11080 Belgrade
Serbia
Phone: +381 60 46 56 086
Email: sale@dialoguetoolkit.com
Url: www.timfluid.com
Partizánska Ľupča 552
032 15 Partizánska Ľupča
Slovak Republic
Phone: +421 903 735 360
Email: sale@dialoguetoolkit.com
Url: www.ecmsystems.sk
C/ Sebastián Elcano 32, 2ª Planta, Puerta 33
28012 Madrid
Spain
Phone: +34 916 794 286
Fax: +34 916 794 287
Email: sale@dialoguetoolkit.com
Url: www.arcamo.com
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
Distributor for Sweden, Denmark & Faroe Islands
Metalgangen 13
2690 Karlslunde
Denmark
Phone: +45 7384 1230
Fax: +45 7384 1280
Email: sale@dialoguetoolkit.com
Url: pgflowteknik.dk
An der Autobahn 15
D-28876 Oyten
Germany
Phone: +49 4207 699 40
Fax: +49 4207 6994 40
E-mail: sale@dialoguetoolkit.com
Url: www.hy-lok.de
Neumo Mühendislik ve Paslanmaz Çelik San. Tic. Ltd. Şti.
Birlik sanayi Sitesi 6. Cadde No:19
34520 Beylikdüzü/Istanbul
Turkey
Phone: +90 (212) 875 01 41
Fax: +90 (212) 875 23 13
Email: sale@dialoguetoolkit.com
Url: www.neumo.com.tr/
Kirkhill Place
Kirkhill Industrial Estate
Dyce AB21 0GU
United Kingdom
Phone: +44 (0) 1224 775277
Fax: +44 (0) 1224 775040
Email: sale@dialoguetoolkit.com
Url: www.hylokuk.com
ST. Semenovskaya B., D49, APT/FLOOR/OFFICE I/5/16
107023 MOSCOW
RUSSIA
Phone: +7 495 517 7261
Fax: +7 495 360 8062
Email: sale@dialoguetoolkit.com
Url: www.fluid-line.ru