Why Use an Automatic Checkweigher?
An Automatic Checkweigher does more than display a number. On a fast packaging line, it weighs each passing pack, rejects units outside set limits, and records results for review. That helps teams spot fill drift before it becomes a costly pattern. The detail matters: a few grams across thousands of packs can affect giveaway, complaints, and production records.
MarketsandMarkets’ checkweigher market analysis estimated a global market of about $279 million in 2023, with growth projected through 2028. Market forecasts are estimates, not guarantees. For technical context, OIML R 51-1 sets requirements for automatic catchweighing instruments, including testing and metrological performance. As measurement expert Lord Kelvin put it, “When you can measure what you are speaking about, and express it in numbers, you know something about it.” That principle fits the production floor. Still, measurement alone cannot fix poor setup.
The strongest case for an Automatic Checkweigher is practical: it checks every pack, creates usable evidence, and can support timely adjustments. Operators can compare live results with target weights, inspect reject trends, and investigate a sudden shift. Yet the system is not magic. Product spacing, vibration, calibration, and maintenance all affect results. A well-chosen checkweigher makes control more visible; people still need to interpret what it finds.
What an Automatic Checkweigher Is
Why Use an Automatic Checkweigher?
What an Automatic Checkweigher Is
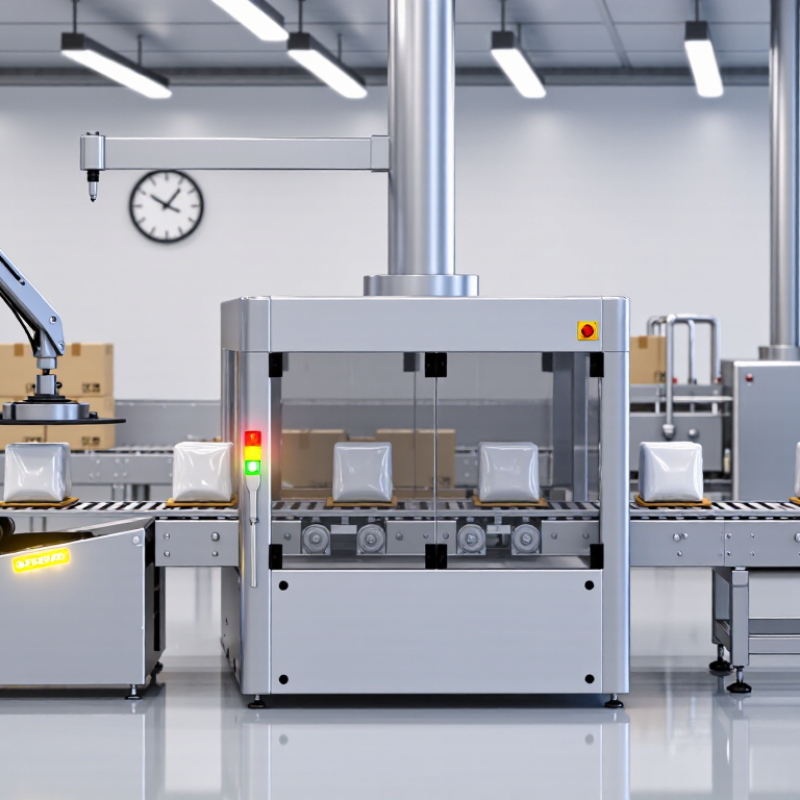
An automatic checkweigher is an in-line weighing system that checks products as they move along a production conveyor. A sensor detects each item, and a weighing platform records its weight while the item is in motion. The system compares that reading with a preset acceptable range. Products outside the range can trigger an alarm or be diverted by a reject mechanism. It works without requiring an operator to weigh every package by hand. That matters.
A typical unit includes a conveyor, load cell, controller, and display. For example, a sealed carton passes over the weighing section, where the load cell measures the force it applies. The controller then assigns a result, often within a fraction of a second. Reliable readings depend on steady product spacing, correct setup, and routine checks with known test weights. Vibration, poor belt alignment, or items touching one another can affect results. It is easy to overestimate what one reading proves: a checkweigher measures weight, not package appearance or contents. Teams should also review rejected items and investigate recurring patterns. Even a well-adjusted machine needs attention when product size, line speed, or packaging changes.
Why Use an Automatic Checkweigher?
What an Automatic Checkweigher Is
An automatic checkweigher weighs products as they move along a production line and compares each weight with preset limits. Products outside those limits can be identified for removal or further inspection.
Illustrative example: The chart shows sample readings for 12 packages with a 500 g target and example acceptance limits of 495–505 g. Actual limits are set according to the product and applicable requirements.
How an Automatic Checkweigher Measures Products
An automatic checkweigher weighs each package as it travels along a production line. An infeed belt spaces products, helping each one cross the weighing section without touching its neighbors. A load cell senses the force beneath the moving belt. The control system combines that signal with timing and conveyor-speed data to calculate a weight. It then compares the result with the configured target and limits. Simple in principle. Sensitive in practice. Vibration, uneven product spacing, and residue on the belt can affect readings, so routine checks and stable line conditions matter.
Products outside the set limits can trigger a reject mechanism, while recorded results help operators spot gradual filling changes. OIML R 51-1 describes metrological and technical requirements for automatic catchweighing instruments; the appropriate instrument class and operating setup affect how results should be assessed. The measurement is not a substitute for checking the complete process. The FAO’s 2019 State of Food and Agriculture estimated that 14% of food was lost between post-harvest and retail. That estimate covers many causes, not just underweight packages. Checkweigher records can reveal weight variation, but they cannot explain every cause on their own.
Why Use an Automatic Checkweigher? - How an Automatic Checkweigher Measures Products
An automatic checkweigher weighs products while they move along a production line. It compares each measured weight with configured limits, helping identify out-of-range items and monitor filling consistency.
How the Measurement Works
| Stage | What Is Measured | How It Works | Typical System Output |
| Product spacing | Position and timing of each item | A conveyor or timing mechanism separates products so they can be weighed individually. | One identified weighing event per product |
| Dynamic weighing | Product load as it crosses the weigh conveyor | A load cell senses force; the indicator processes the signal while accounting for the moving conveyor and vibration. | Measured weight, commonly displayed in g or kg |
| Weight comparison | Measured weight versus target and configured limits | The controller compares the result with product-specific acceptance limits. | Underweight, acceptable, or overweight classification |
| Sorting and recording | Classification and production data | If configured, a reject device removes out-of-range products; the system can record results for process monitoring. | Reject signal, count, and weight-trend data |
Illustrative Product Checks
| Product Example | Target Weight | Configured Acceptable Range | Measured Weight | Deviation from Target | Checkweigher Result |
| Small packaged item | 250 g | 247.5–252.5 g | 249.8 g | −0.2 g | Accept |
| Standard pouch | 500 g | 495–505 g | 493.6 g | −6.4 g | Reject — below lower limit |
| Large pack | 1,000 g | 990–1,010 g | 1,004.2 g | +4.2 g | Accept |
| Multi-unit carton | 2,000 g | 1,980–2,020 g | 2,023.1 g | +23.1 g | Reject — above upper limit |
| Sample container | 750 g | 742.5–757.5 g | 750.6 g | +0.6 g | Accept |
Note: Product weights and acceptance ranges above are illustrative examples, not universal settings or legal tolerances. Actual limits depend on the product specification, packaging, operating conditions, and applicable regulations.
Where Checkweighers Fit in a Production Line
An automatic checkweigher usually sits on the production line after filling or sealing and before case packing. At this point, each package is closed, so its weight can be checked without interrupting earlier filling work. A belt carries packs across a weighing section, where sensors record readings as the line moves. Small timing differences matter.
The system compares readings with configured weight limits and can divert out-of-range packs to a separate lane. This lets operators inspect a specific package instead of stopping the whole line for routine checks. Placement depends on the product and equipment. A checkweigher needs consistent spacing, a stable conveyor, and enough room for rejected packs to exit safely. If containers wobble or packages touch, readings may be less reliable. This is easy to underestimate.
Teams may connect weight results to filling equipment or production records. Repeated low readings can point to a filler setting; scattered readings may indicate inconsistent product flow or handling. The instrument cannot identify the cause by itself. Operators still need to verify setup, inspect samples, and follow documented checks. Automation can support faster production, but only when the checkweigher suits the line’s speed, package size, and layout. That fit is not always perfect.
How Checkweighers Support Quality and Compliance
An automatic checkweigher weighs each pack while it moves along the line and flags units outside set limits. That creates a time-stamped record for quality checks and helps staff spot drift before it affects more packages. Small deviations matter. OIML Recommendation R 51-1:2016 sets accuracy classes and verification requirements for automatic catchweighing instruments, giving operators a technical basis for checking performance. But a correct reading depends on regular calibration, stable product flow, and suitable settings.
The scale of food loss makes reliable measurement relevant. FAO’s 2019 State of Food and Agriculture estimated that 14% of food is lost between harvest and retail. UNEP’s Food Waste Index Report 2024 estimated 1.05 billion tonnes of food waste at retail, food-service, and household levels in 2022. These figures do not prove that checkweighers prevent food loss; they show why process control deserves attention.
A checkweigher does not certify a product by itself. Operators still need documented procedures, verified instruments, and clear responses to out-of-limit readings. It is easy to trust the dashboard too much. A manual spot check can reveal issues the system’s trend line misses.
What to Consider When Choosing a Checkweigher
When choosing an automatic checkweigher, start with the product and line conditions, not the machine’s headline speed. Record each pack’s weight range, dimensions, and packaging material. A light pouch can behave differently from a rigid tub on a fast conveyor. Ask suppliers to test representative products at your actual line speed, including awkward formats and routine changeovers. Small details matter.
Accuracy also depends on belt vibration, product spacing, and how consistently packs arrive. Specify the required weighing range, throughput, reject method, and data records before comparing equipment. FAO’s 2019 State of Food and Agriculture estimated that about 14% of global food is lost between harvest and retail. That figure does not measure checkweigher performance, but it underlines why reliable process control deserves attention. Check that the system can connect with your line controls and flag repeated weight drift. Consider washdown needs, available floor space, and how quickly operators can clean and recalibrate it. Then test again. A technically capable unit can still disappoint if the real bottleneck is upstream, or if changeovers take longer than expected. That part is easy to overlook.